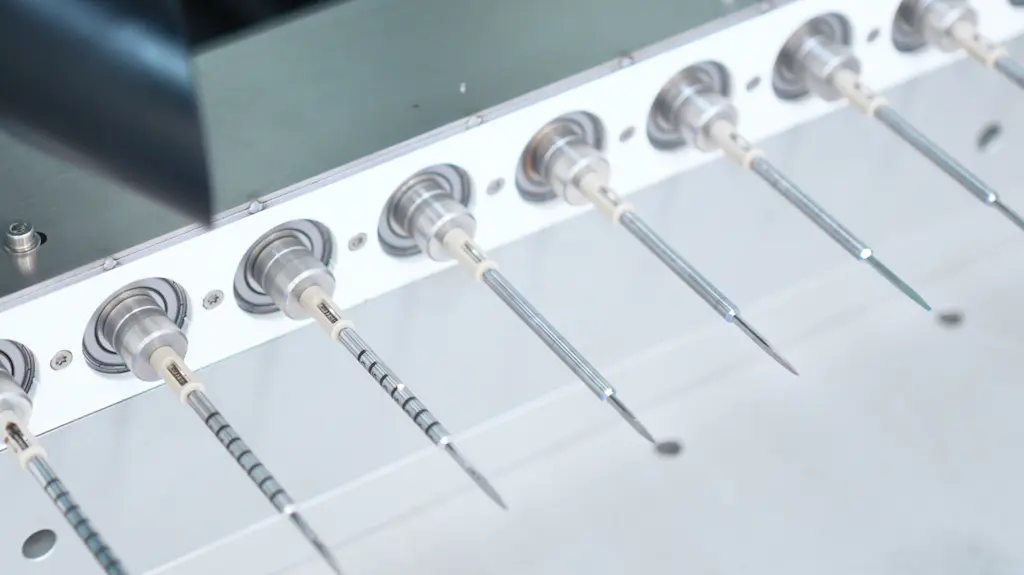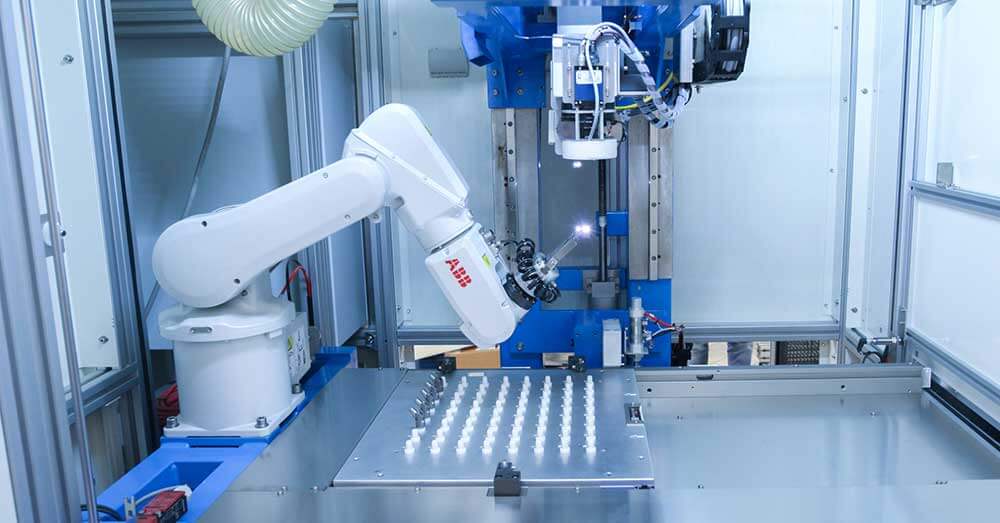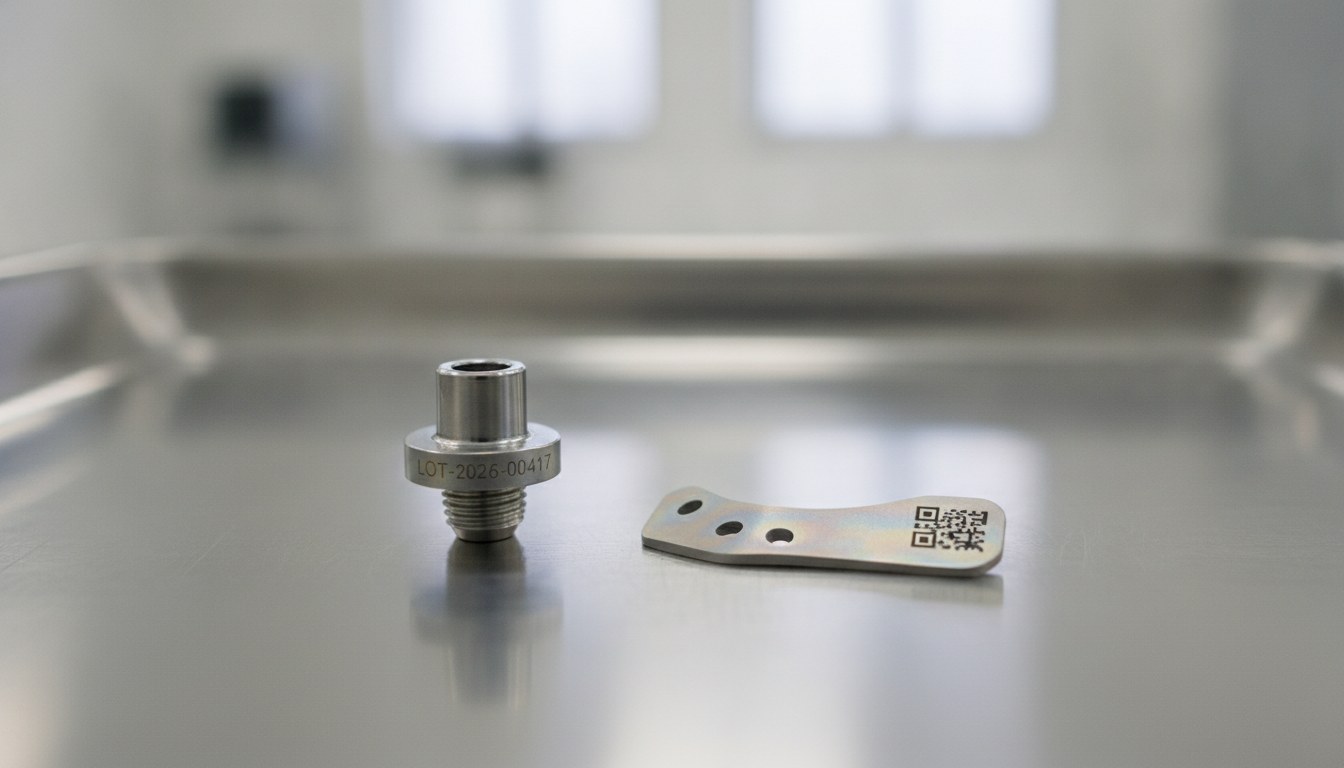
Anyone who manufactures implantable titanium screws, abutments or plates knows exactly why that surface must be treated with care: the issue is that marking is the last operation to touch it, and it’s the point where all that care risks being undone. Any technique that removes material, deposits residues or uncontrollably alters the oxide film (TiO₂) calls into question the very characteristic for which the part exists. On an implantable device, in short, marking is not a cosmetic step.
At the same time, the regulatory framework leaves no room for compromise. An implantable device must carry a UDI identifier that is legible and permanent throughout its entire life cycle, and the code must survive washing, passivation and repeated sterilization cycles without becoming illegible and without creating micro-cavities that could become initiation points for contamination or corrosion.
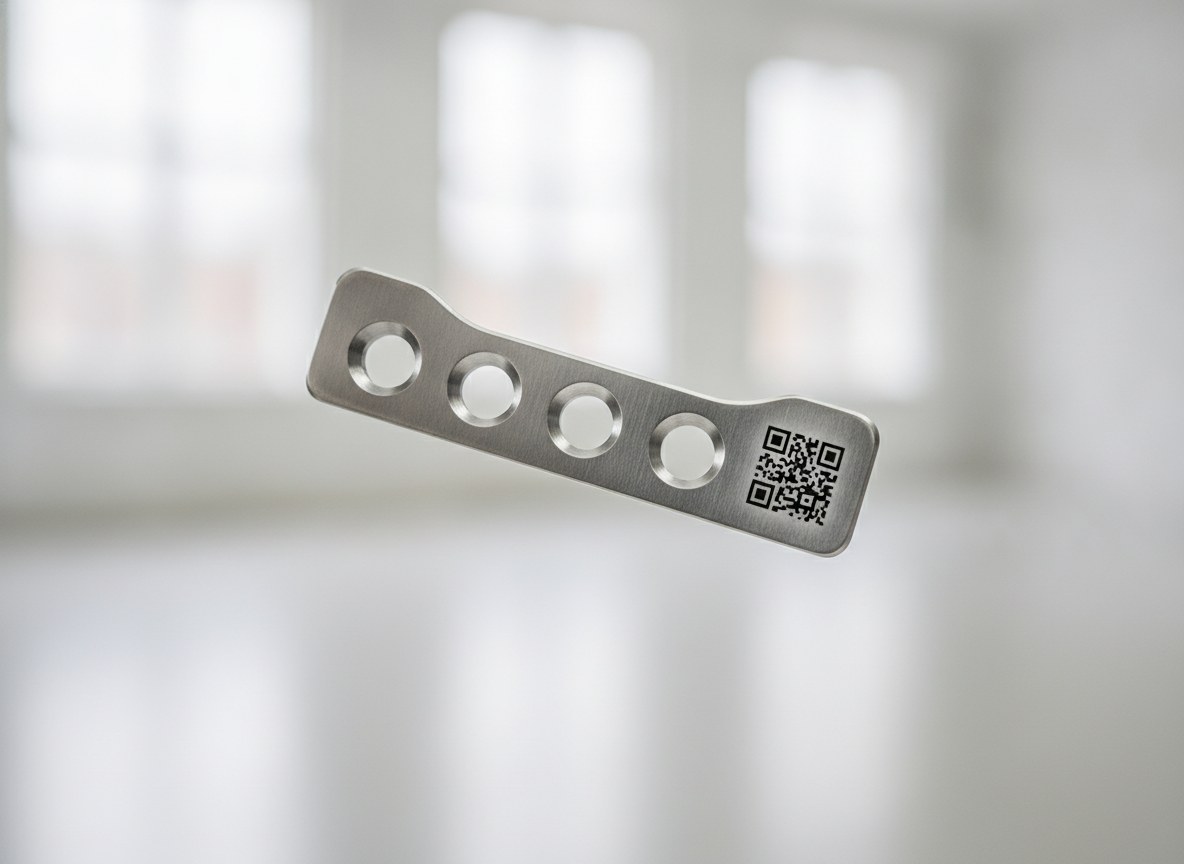
Laser marking by controlled oxidation addresses both constraints at once: it generates contrast — and color — by modifying the oxide layer instead of removing it, without adding foreign material and without compromising downstream treatments.
The right criterion for choosing marking on implantable parts
On an implant, the surface is inspected and documented with the same care reserved for dimensional tolerances. From this follows a simple criterion for judging a marking technique: what it does to the oxide layer. Ink marking deposits foreign material, which then has to be removed or remains as a potential contaminant. Mechanical engraving or micro-punching removes metal and creates grooves with edges and burrs — that is, geometries that are difficult to clean and passivate. These are the same reasons why, when it comes to the traceability and MDR compliance of dental implants, the choice of marking technology is to all effects a process choice, not a finishing one.
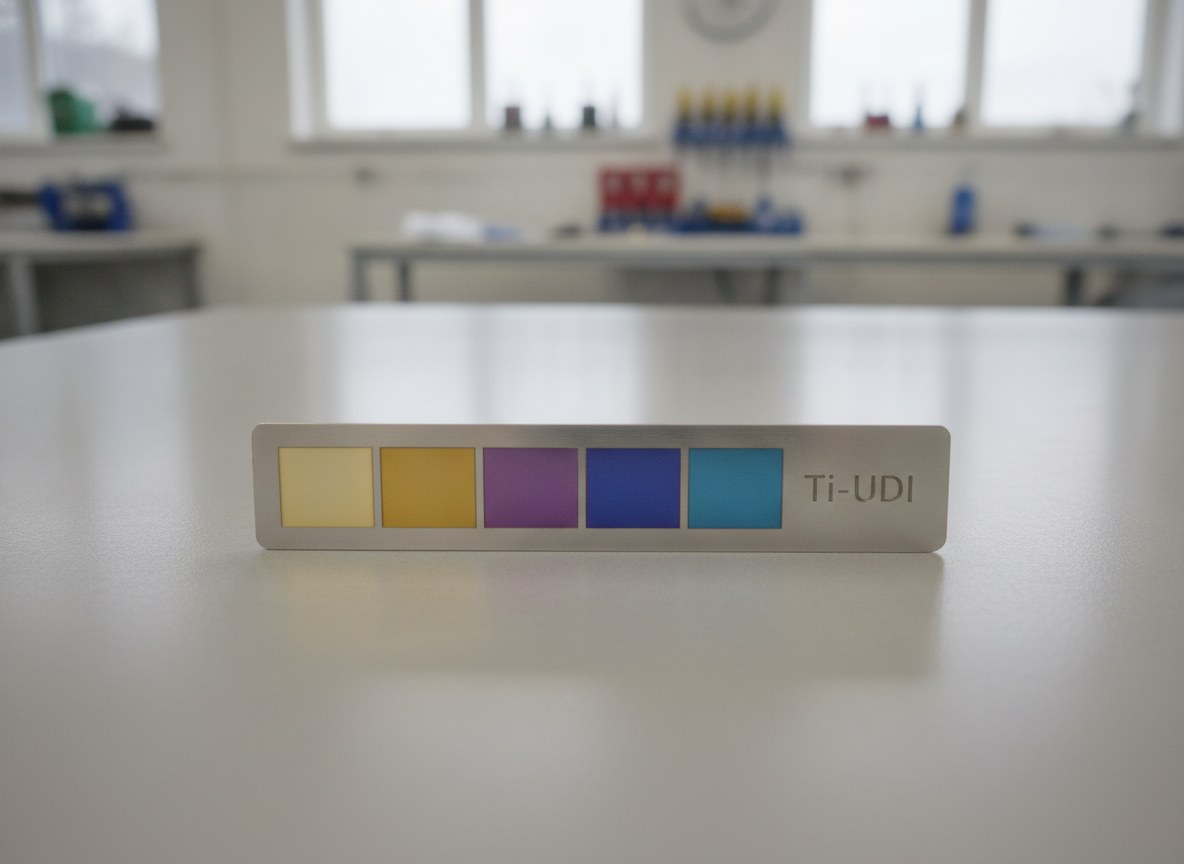
Interference color: how it forms on titanium
When a 1064 nm beam sweeps across the titanium surface without removing it, it heats the metal for the very brief time of the pass and accelerates its local oxidation. This grows a transparent oxide film of controlled thickness. The light striking this film is partly reflected off its outer surface and partly off the oxide-metal interface: the two waves recombine and, depending on the thickness traversed, some wavelengths reinforce each other while others cancel out. This is the phenomenon of thin-film interference, the same one that colors a film of oil on water.
The technical point to hold firm is that here the color is not a pigment and not a paint: it is a structural property of the oxide. By varying the energy density, the film thickness varies, and with the thickness the hue changes — from straw yellows to brasses, to purples, to blues. These are the real hues that titanium produces as it oxidizes, not arbitrary “print-like” colors. This distinction matters at the specification stage: a palette of repeatable shades tied to process parameters can be defined, not just any free color.
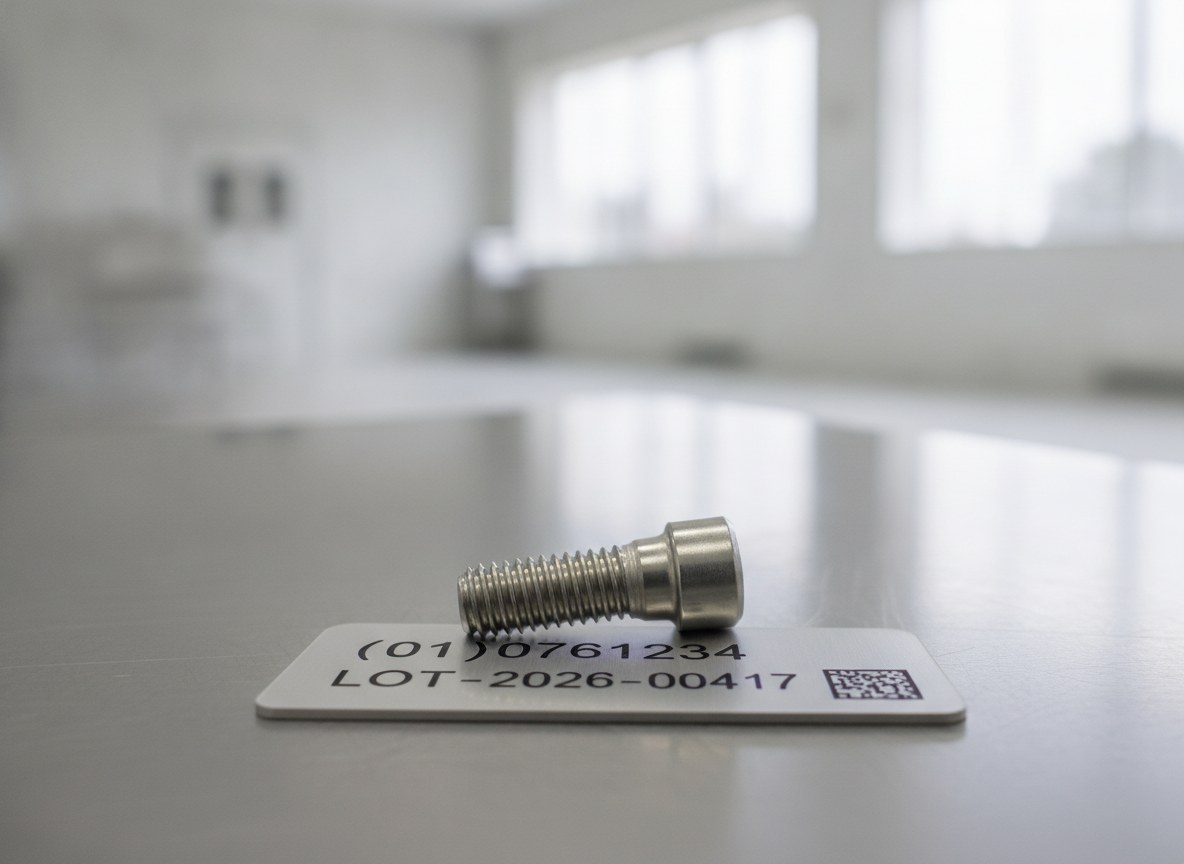
Oxidation without removal: no residue, no particulate
The decisive difference from engraving is that controlled oxidation does not cut into the material. The surface remains continuous: no grooves, burrs or dust are generated, and no filler material is introduced. For an implantable component this means not creating geometries that trap contaminants and not leaving particulate on the surface that the surface texturing of implantable components and subsequent washing would then have to manage.
It must be stated with technical precision: oxidation is by its very nature a controlled thermal process — an oxide is grown by locally heating the metal — so it is not correct to speak of zero thermal input. The value lies in governing it: energy metered to grow the required oxide without altering the substrate in depth, without melting and without re-melting the edge. The marking stays on the surface, where it is needed, and the core of the component is not affected.
Oxidation, ink and engraving compared
Placed side by side, the three techniques differ precisely in what they do to the oxide layer. Laser oxidation grows it in a controlled way, without adding anything and without removing anything: it leaves no residue or particulate, maintains high permanence after passivation and sterilization because the contrast is part of the surface itself, and introduces no contaminants that would disturb any downstream anodizing.
Ink marking, by contrast, does not modify the oxide but deposits foreign material on top of it: a deposit that then has to be removed, that tends to degrade with washing and sterilization cycles, and that in downstream anodizing risks interfering with the bath. Mechanical engraving, on the other hand, offers high permanence, but achieves it by removing metal: it creates grooves and burrs, geometries that are difficult to clean and passivate, with dust and edges that trap contaminants and alter the growth of the anodic film. This is the comparison that explains why, on implantable parts, the right technique is chosen on the basis of its effect on the oxide and not on aesthetic appearance.
Color repeatability as a process parameter
On an implant, hue is not aesthetics: it is information. A color can encode a size, a family or a stage, and to serve as encoding it must be repeatable part after part and batch after batch. Since the hue depends on the oxide thickness, and the thickness depends on the deposited energy density, repeatability is a matter of parameter control: power, frequency, scanning speed, line spacing and focus must be set and kept stable.
Two mechanical and optical factors weigh in here. First, focus stability on the actual geometry of the part: on curved surfaces or on screws the working distance changes, and with it the energy density, hence the hue. Second, the consistency of the source and of the starting surface: a homogeneous surface state at the input is the prerequisite for a homogeneous oxide at the output. Color repeatability, in short, is built upstream through the definition of the cycle; it cannot be recovered downstream.
Permanent UDI and its verification
In terms of traceability, controlled oxidation also produces the dark contrast needed for a legible DataMatrix marked directly on the part, without removal. Permanence is the central requirement for implantable parts: the code must remain legible after passivation and after repeated sterilization cycles, conditions under which a merely deposited marking tends to degrade. A contrast obtained by oxide, and not by removal, is born from the start as part of the surface.
On quality control, a distinction that is substantial in the medical field must be maintained: grading and verification of codes are two different things. Grading according to the applicable ISO/IEC standard is the quality assessment that can be performed in line, part by part, to ascertain that the DataMatrix falls within the required class; verification in the strict sense requires controlled laboratory conditions. Documenting which of the two is performed, and with what instrumentation, is an integral part of managing compliance and the causes of UDI non-conformities on metal.
Compatibility with downstream anodizing
Many titanium components undergo downstream anodizing, typically for color coding or surface conditioning. Since anodizing also works on oxide growth, the marking stage must leave nothing on the surface that would interfere with the bath or with the homogeneous growth of the anodic film. This is exactly the advantage of laser oxidation: it deposits no material and leaves no residue, so it introduces no contaminants that would compromise the subsequent treatment. The sequence between marking and anodizing must nonetheless be defined and validated together, because both act on the same layer and both must be documented.
How to document the process for the technical file
For an implantable device, marking enters the technical file as a process, not as a detail. This means setting and recording the parameters that determine the oxide — power, frequency, speed, spacing, focus, wavelength — and linking them to the hue and grading class obtained, so that the result can be traced back to known conditions. It means validating the cycle on real samples, verifying the permanence of the code after passivation and sterilization, and documenting that the marking does not alter the state of the oxide relevant to biocompatibility, according to the applicable criteria.
Process traceability closes the loop: versioned parameters, locked recipes, grading results archived per batch. It is the same documentary compliance logic already discussed for direct UDI marking on metal, applied to the specific case of implantable titanium, where the stakes are not only legibility but the integrity of the surface that makes the part fit for use.
Who it is designed for (and who it isn’t)
Controlled oxidation on titanium is the natural choice when a permanent identifier and the guarantee of not altering the surface oxide are needed at the same time: dental screws and abutments, plates, implantable components in titanium and its alloys, with a requirement for repeatable color coding or for a high-contrast DataMatrix marked directly on the part. It is also suitable when a downstream anodic treatment is planned, precisely because it leaves no residue.
It is not, however, the right answer for every medical need. Where a matte, non-iridescent black marking is needed on steel instruments destined for multiple aggressive passivations, or where the requirement is maximum contrast resistance to repeated sterilization cycles, the most suitable configuration is the picosecond source: ultra-short pulses that produce a deep, stable black marking with a negligible thermal impact on the substrate, without iridescent hues and without the micro-cavities of engraving. This is the technology we explore in depth when discussing picosecond for medical devices, where the priority is a dark contrast that withstands washing more than an interference hue matters. And if the component is not made of titanium, the interference color mechanism simply does not apply: the reasoning must be redone on the actual material. In summary: if the part is implantable titanium and the constraint is to mark it without touching the oxide that makes it biocompatible, controlled oxidation is the technique built exactly around that constraint.

Public Relations Manager | LASIT
Public Relations Manager at LASIT since 2019, Claudia Neri is responsible for managing the Marketing and Communications department. She handles the company’s communication strategy, coordinating public relations, brand promotion and institutional communication activities for the Italian and international market.