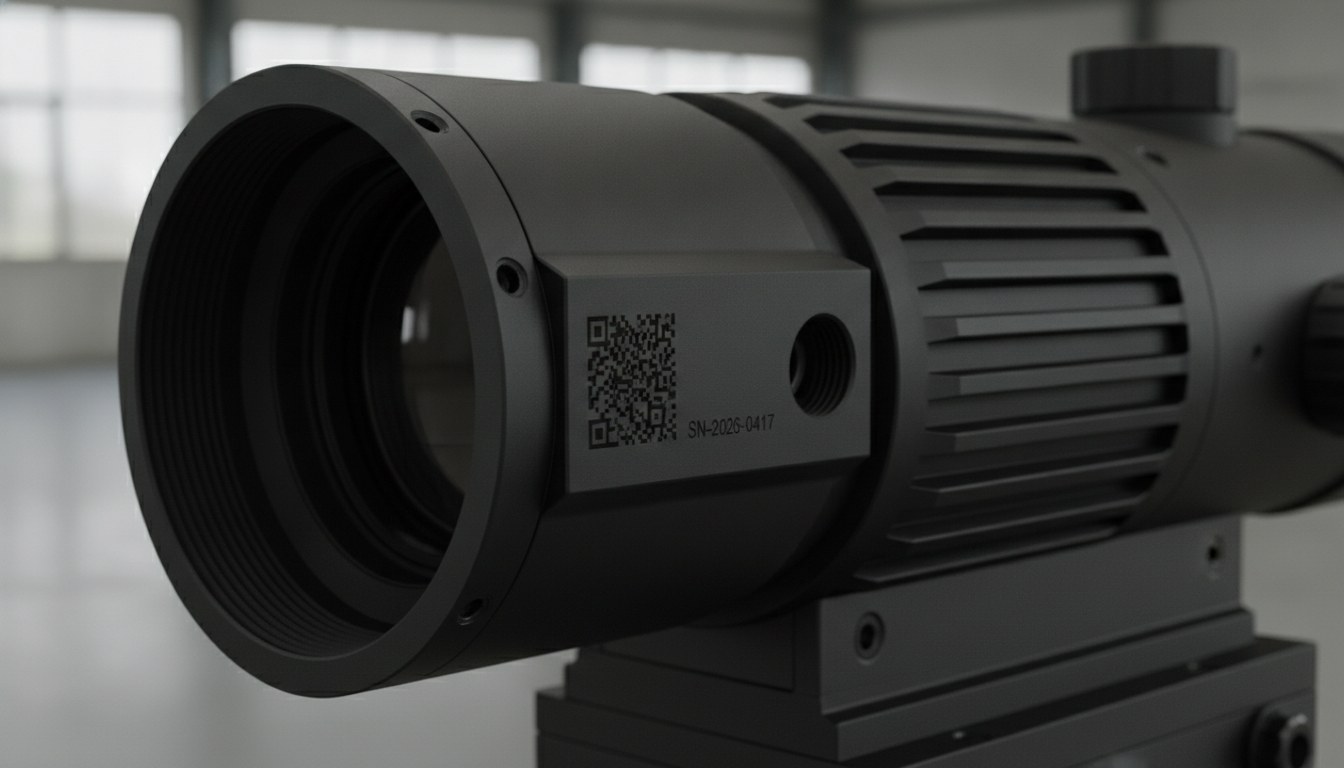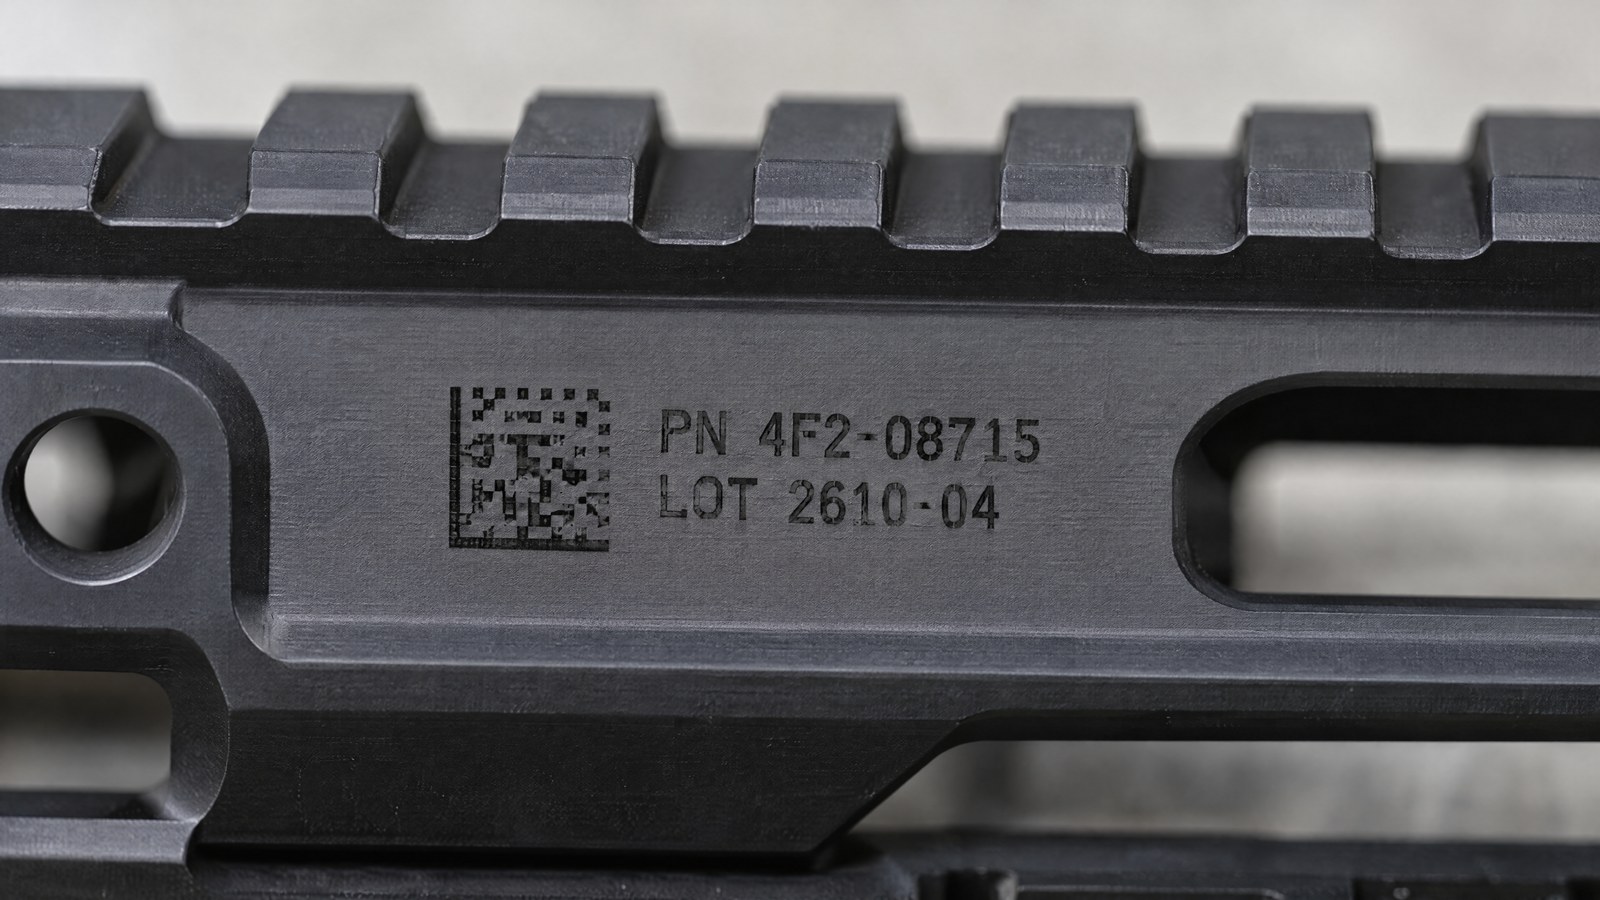
In the defense sector, a mark isn’t just data to be read: it’s also an element that can be seen. On a weapon, a mount, or a component that operates in the field, a mark that’s too shiny produces a directional reflection, and under certain operating conditions that reflection is a problem. Add to this the operating environment: aggressive cleaning solvents, constant abrasion, temperature swings between cold and heat. The mark has to stay legible for the entire life of the part without ever becoming a point that glints.
Anyone industrializing these components knows the dual constraint. The mark needs enough contrast for an operator or a reader to resolve it, but it must not introduce a specular surface. It’s a requirement that a standard industrial mark — designed to maximize contrast regardless of finish — doesn’t address: there the only goal is that the code be visible, not that it stay matte.
On two surface families typical of this sector — black anodized aluminum and blued steels — the answer lies in treating the mark’s reflectance as a process parameter and not as a side effect. With the right parameter window, the laser produces a permanent matte black on both substrates, keeping legibility without adding glint.
Reflectance is a parameter, not a side effect
The difference between a mark that glints and one that doesn’t is the nature of the reflection. A smooth, glazed surface reflects light in a specular way, like a mirror: from a certain angle it becomes a bright, visible spot. A micro-irregular surface scatters it in all directions and appears matte from every side. When the beam melts the metal and then lets it resolidify into a smooth layer, the specular component increases; when instead it works through controlled oxidation or micro-texturing, it knocks that component down.
This is where fine pulse management becomes decisive. MOPA fiber sources let you independently adjust pulse duration and frequency, and this shifts the result from a glossy melt toward a matte, uniform mark. The same goal is reached with picosecond pulses, which transfer the energy in a time so short that thermal glazing becomes negligible, leaving a cold, diffuse black. In both cases, the low reflectance isn’t a lucky accident: it’s the parameter window that produces it.
Black anodized aluminum: marking within the layer without creating a point that reflects
On anodized aluminum, the mark works inside the anodized layer, which is already matte on its own. The risk, with the wrong parameters, is opening a glossy point where the beam removes too much and exposes the metal underneath: in that zone the reflection comes back and defeats the matte finish chosen upstream. Process control serves exactly this purpose — to modulate the interaction so that the mark stays legible while keeping a diffuse appearance consistent with the rest of the surface.
At 1064 nm, fiber is the natural technology on this substrate, because aluminum absorbs this wavelength well. The lever isn’t peak power, but the precision with which the energy is metered pulse after pulse: a crisp mark, with enough contrast, that doesn’t become a reflective window onto bare aluminum.
Blued steels: annealing that stays in the black
Blued steels start from a surface conversion to black oxide. On an already dark surface, adding contrast without adding shine is a specific task. The most consistent route is annealing: the beam locally heats the metal and grows an oxide layer below the surface, without removing material. The mark forms inside the part, is flush, has no raised edges, and keeps a matte look that blends with the surrounding bluing.
Compared to a mark that removes material, annealing avoids exposing shiny steel and avoids creating edge microfractures that can trigger rust on a component destined for a harsh environment. The mark is part of the surface, not a layer added on top of it.
Permanence: solvents, abrasion, temperature swings
Permanence depends on where the mark sits. A mark obtained through oxidation or substrate modification isn’t a coating laid on top of the part: it’s a transformation of the material itself. That’s why a cloth soaked in solvent or degreaser doesn’t carry it away as it would with ink, and repeated abrasion doesn’t wear it down like a surface print. An annealing mark, being flush and free of raised features, offers no edges for abrasion to attack first.
Temperature swings also weigh less on a stable oxide already formed by the process than on a paint or a label. That’s the reason why, in defense as in medical, sub-surface marking is preferred when the part has to go through aggressive cleaning and thermal cycles while staying identical to itself. The same resistance principle applies to weapon components: we find it in marking on ammunition and in traceability on barrels and rifle components, where the mark has to survive the entire life cycle.
Low-reflectance marking qualificationMaterial analysisParameter windowReflectance testResistance testIn-line grading
Legibility without glint: diffuse contrast and in-line grading
A low-reflectance mark calls for rethinking legibility. With a matte mark you don’t rely on reflection to make the characters stand out, but on a diffuse contrast that’s stable from every viewing angle and under any lighting. For 2D DataMatrix codes, this means tending to the regularity of the cells and the quality of the edge, so that a reader locks on even when the surface doesn’t return light.
To keep the result under control in production, in-line grading is used, which evaluates code quality against applicable standards directly on the part during the cycle. It’s distinct from metrological verification, which requires controlled laboratory conditions: grading accompanies the marking batch after batch, while verification certifies in a separate context. Keeping both clear avoids confusing a process check with a conformity measurement.
What changes compared to a standard industrial mark, and who it’s designed for
The difference from a standard industrial mark is clear-cut and comes down to one added constraint. In common manufacturing, you optimize contrast, and if the mark turns out a bit glossy, it’s not a defect. In defense, reflectance enters the specifications: the mark has to be readable and at the same time stay matte, because one more specular surface on a component is a piece of information you don’t want to give. The parameter ignored elsewhere becomes the acceptance criterion here.
This approach makes sense where the finish is black and matte to begin with — black anodized aluminum, blued steels — and where the part faces solvents, abrasion, and temperature swings. It’s the natural evolution, on the materials side, of what was covered for low-reflectance marking in defense: there the heart of it was the source, here it’s the behavior of the mark on the sector’s two typical substrates.
It is not, however, the approach to pursue when maximum visibility is needed and a reflection isn’t a problem, or on light surfaces where a full-contrast black is simply the most legible result. In those cases, standard marking logic remains the most rational. But when the requirement is that the mark not glint and not reveal, and that it withstand cleaning and field use without changing, controlling reflectance on anodized and blued surfaces is what separates a mark suited to defense from one that is merely legible.

Applications Manager | LASIT
Applications Manager at LASIT for over 20 years, Mario Palmieri oversees the management and development of the company’s laser laboratory. He is responsible for conducting sample tests for customers, supporting the automotive, medical, aerospace and electronics sectors in identifying the most suitable laser marking solution for their needs.