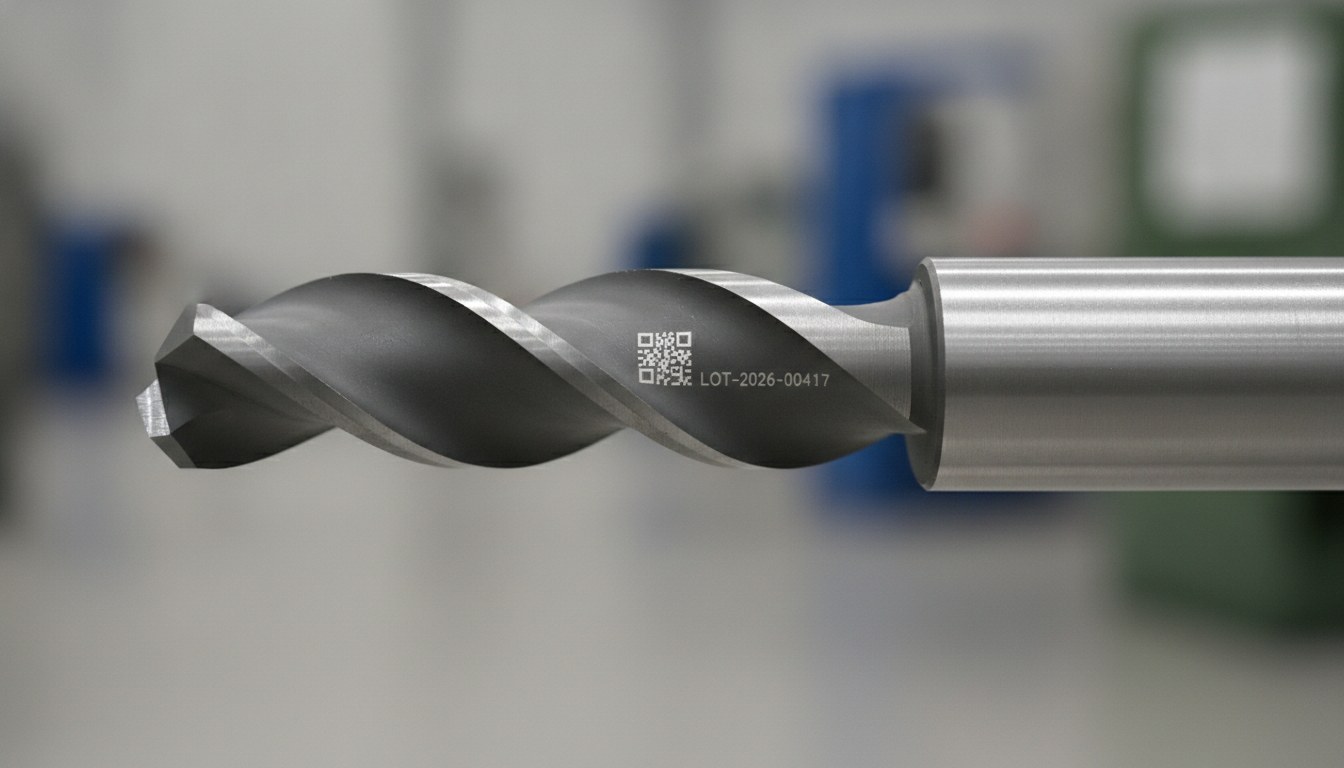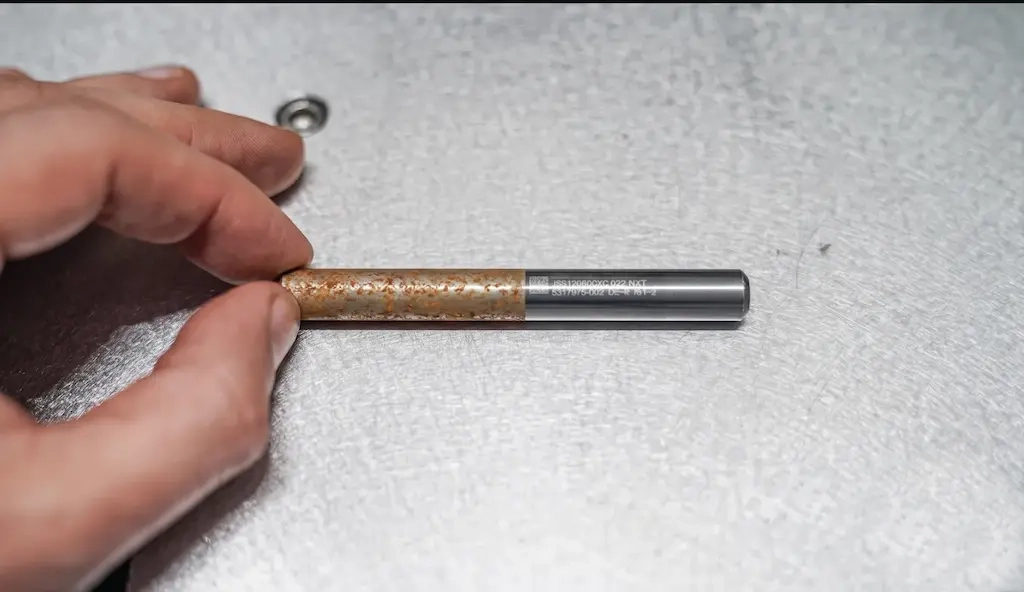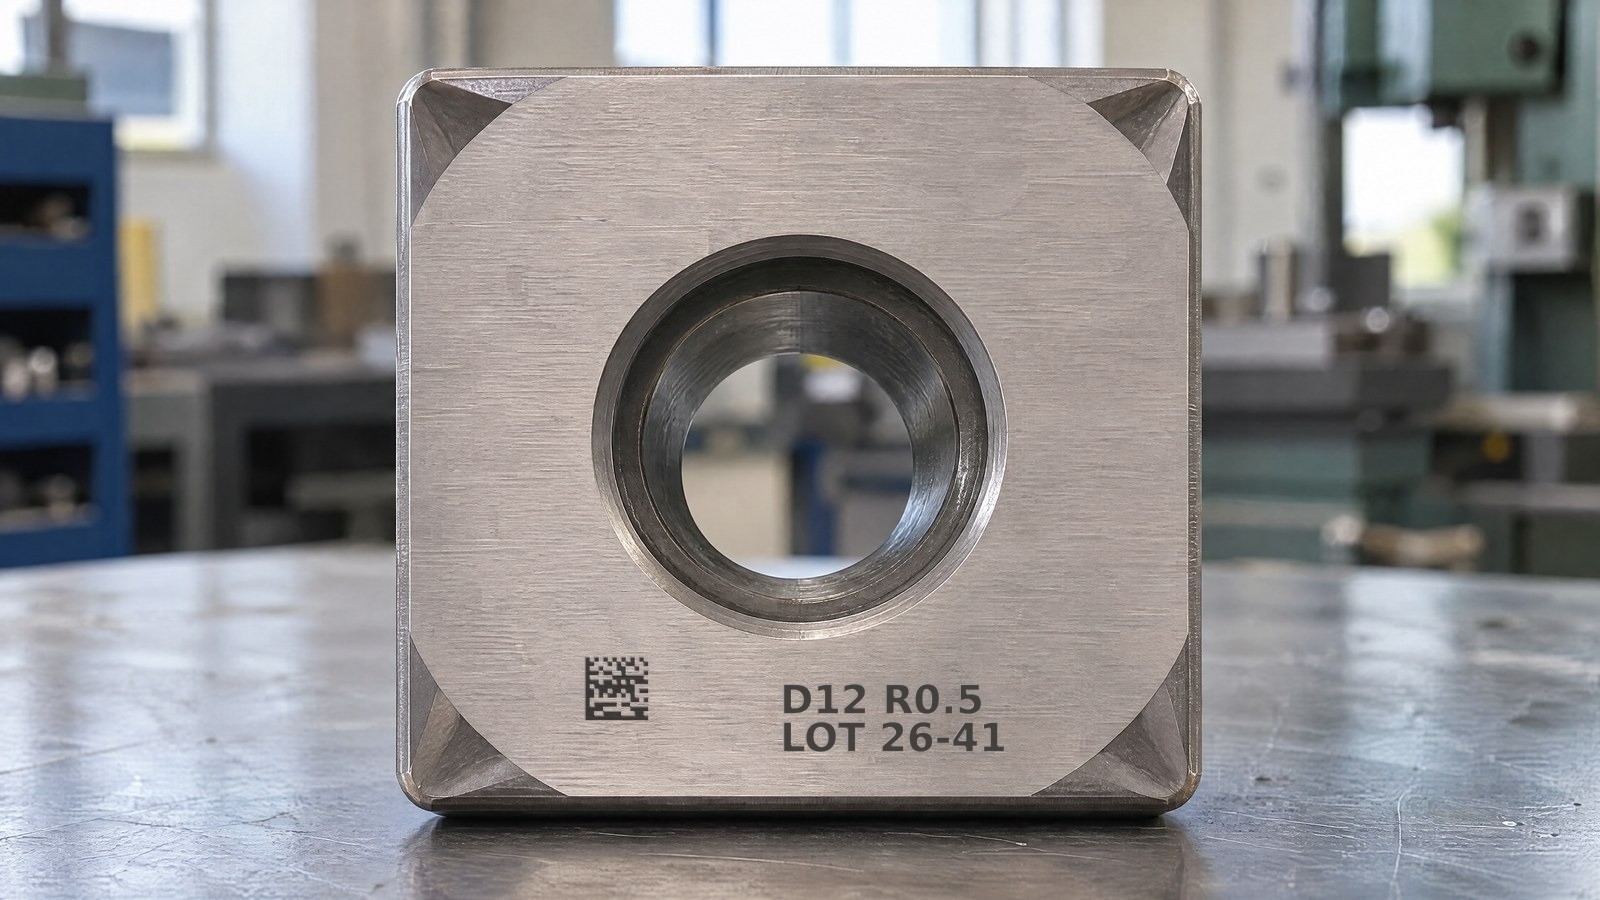
Anyone who makes turning inserts, solid end mills, or small cutting tools knows the same constraint well: fitting a legible DataMatrix and an alphanumeric string into a fraction of a square inch, on a face that sometimes measures less than half an inch on a side. The code has to stay readable for an inline reader even after sharpening, coating, and the first hours of use; the string has to be readable by eye or with an OCR system. On surfaces this small, the margin for error is minimal.
The instinct, when a mark “won’t read,” is to turn up the power. At these sizes that is almost always the wrong move: more energy widens the track, tends to burn the edges of the modules, and reduces the contrast between a filled cell and an empty one—making worse the very thing you were trying to improve. The factor that decides whether a DataMatrix with a cell below a few hundredths of an inch is readable—or whether a line of text a few hundredths of an inch tall stays crisp—is not the number of watts, but the spot size, that is, the focal length and the scanning optics.
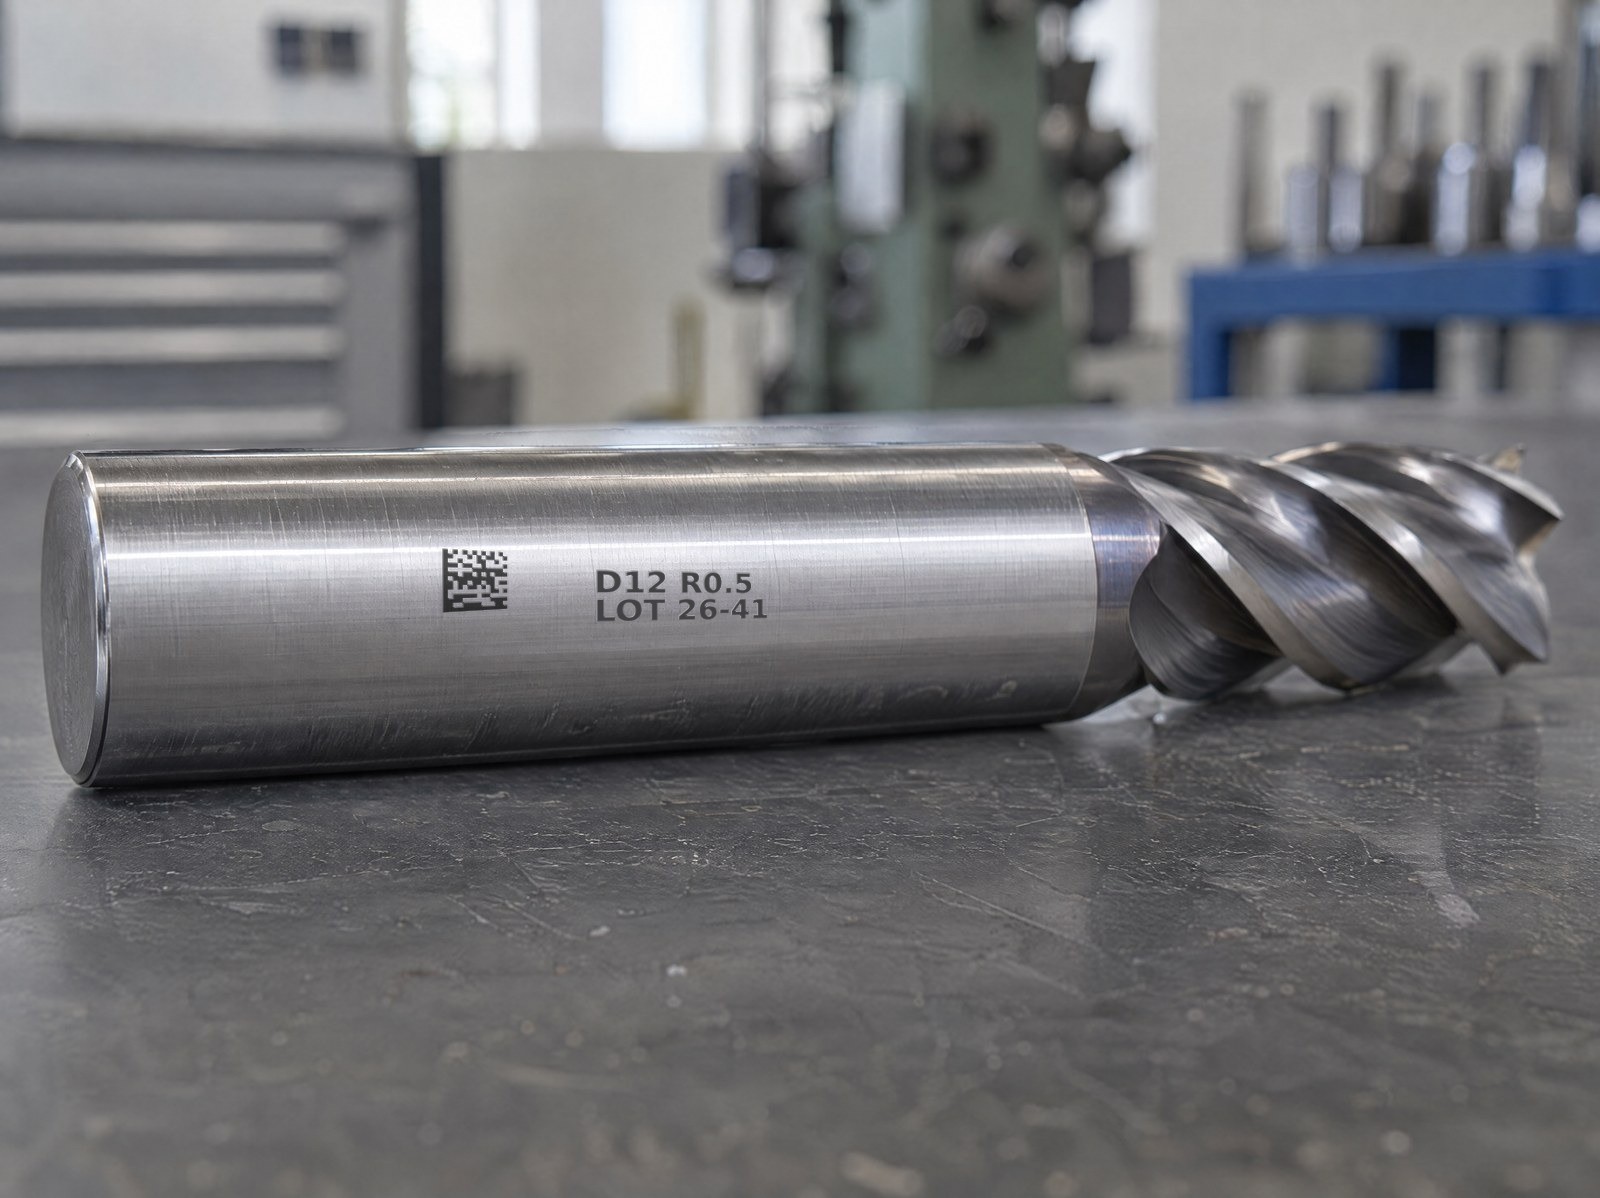
Why watts don’t make the micro-engraving
Power governs how much energy reaches the material per unit of time: it sets the contrast, the depth, and the process speed, but not the fineness of the line. The smallest detail the laser can write is fixed by the diameter of the focal point: for a given spot, raising the power widens the zone actually worked—thermal edge, module bleed—it does not make it finer. On a tool, moreover, you want the least possible material removal so as not to weaken the cutting edge or damage the coating: the goal is maximum contrast at minimum fluence. Micro-engraving is therefore first and foremost a problem of optical resolution, not of energy.
Spot, focal length, and field: the relationship that governs resolution
The spot gets smaller the shorter the wavelength and the focal length of the optics, and the wider the beam entering the lens. It is a zero-sum relationship with the working field: a short focal length concentrates the beam into a small, high-density spot, ideal for fine detail, but it narrows the marking field and reduces the depth of field; a long focal length covers a wide field but with a larger spot. Telecentric lenses keep the beam perpendicular across the entire field, with a uniform spot from center to edges—a valuable condition when marking on tiny surfaces. Anyone who wants to dig deeper into the link between focal distance and depth of field will find the full picture here.
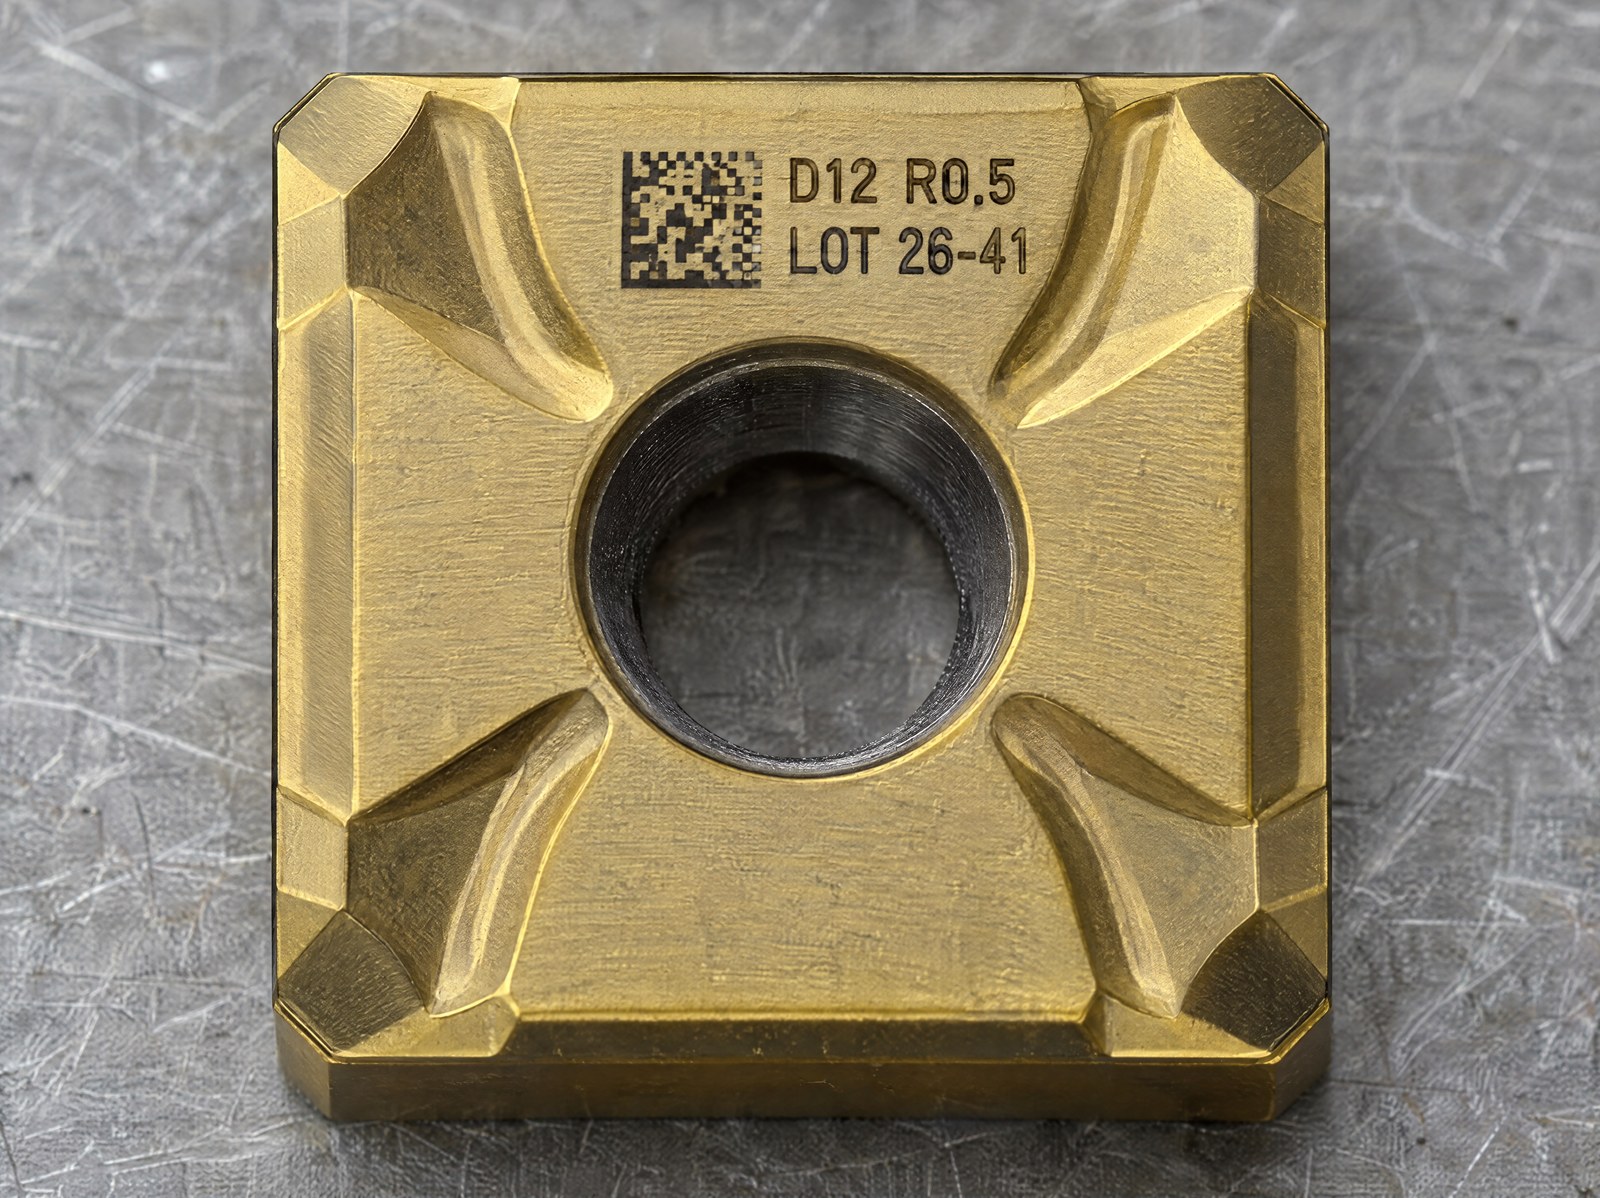
This is exactly the operating point: on an insert or an end-mill shank the usable field is tiny, so you can choose a short-focal-length, narrow-field optic and get a fine spot. The lever is the optics, not the power supply.
Minimum line width and DataMatrix cell
The minimum width of a line coincides, in practice, with the spot size plus the process spread: you cannot go below that value, no matter how much power you use. For a DataMatrix the same reasoning applies to every single cell: for the code to be resolvable both in marking and in reading, the module must stay comfortably larger than the spot, so that a filled cell and an empty one come out clearly distinct. When the cell drops below a few hundredths of an inch, the margin between spot and module thins out and the quality of the code suffers. The process rule is to size the code so that each module is worth several spots, never just one: if there is no room, you either reduce the spot—shorter focal length, or a shorter wavelength—or reduce the data to be encoded to leave larger cells.
The right fonts for micro-engraving
Below a fraction of an inch, the typographic choice weighs as much as the laser parameters. Fonts with a uniform stroke width work best, where every line is the same width as the spot and the result is predictable; serif fonts and fonts with strong contrast between thick and thin strokes should be avoided, because the fine strokes disappear as soon as they drop below the spot size. It helps to favor open counters and a good x-height, so the letters don’t close up into a single solid mass. And above all keep the text short: lot and serial number, not lengthy descriptions. Fewer characters means each one is larger, and therefore more readable—by eye and for OCR alike.
When you need UV at 355 nm
As long as the surface allows it, the fiber source at 1064 nm handles the great majority of markings on tools. But when the spot itself becomes the bottleneck—the smallest cell, the thinnest line—the wavelength comes into play. At 355 nm the beam focuses into a smaller spot than at 1064 nm with the same optics, because the minimum spot diameter scales with the wavelength. On top of that, the interaction of UV with the material is markedly “cold,” with limited heat input: an advantage on sensitive coatings and delicate cutting edges. UV remains the choice reserved for the most extreme detail and delicate materials, not the first-resort solution.
| Parameter | Fiber 1064 nm | UV 355 nm |
|---|---|---|
| Wavelength | 1064 nm | 355 nm |
| Minimum focusable spot | Larger | Smaller |
| Heat input at the edge | Higher | Limited |
| Role in micro-engraving | Standard for most cases | Most extreme detail and delicate materials |
Inline grading, laboratory verification: two different checks
When you push a code to the limit of its size, you need to know whether it is really readable—and the two available checks answer different questions. Grading evaluates the quality of the code according to a standardized scale (ISO/IEC 15415 for 2D codes, AIM DPM for direct part marking) and can be performed inline with a vision system, assigning a grade to every part that goes by. Verification is another matter: it requires controlled laboratory conditions—calibrated lighting, optics, and instrument—and certifies compliance in a repeatable way. It is not an inline check. On micro-engraved codes the distinction is decisive: a DataMatrix that earns an acceptable inline grade may require laboratory verification to confirm that it reaches the grade required by the customer. The difference between reading, grading, and verification is the point not to get confused about.
When it pays to keep only the code (and who it’s designed for)
There is a point where text and 2D code compete for the same fraction of a square inch. When the DataMatrix module is already close to the spot limit, adding a readable line of text forces you either to enlarge the code area—space the insert doesn’t have—or to shrink both below the reliability threshold. In those cases the correct engineering choice is to drop the plain text and keep only the DataMatrix, which packs lot, serial, and part number into a footprint a scanner resolves better than the eye. Keep the text only when an operator has to read it without an instrument.
Spot-optimized micro-engraving is designed for those who mark inserts, end mills, and small cutting tools with traceability requirements on small surfaces, where marking end mills and tools must stay readable downstream of coatings and wear. There is no need to push toward the smallest spot or toward UV when the surface is large and standard fiber already resolves the code with margin: in those cases you complicate the process with no gain. But when the face to be marked is tiny and the code has to withstand reading and grading, the factor to work on is the spot—the focal length and the optics—not the watts.

Applications Manager | LASIT
Applications Manager at LASIT for over 20 years, Mario Palmieri oversees the management and development of the company’s laser laboratory. He is responsible for conducting sample tests for customers, supporting the automotive, medical, aerospace and electronics sectors in identifying the most suitable laser marking solution for their needs.