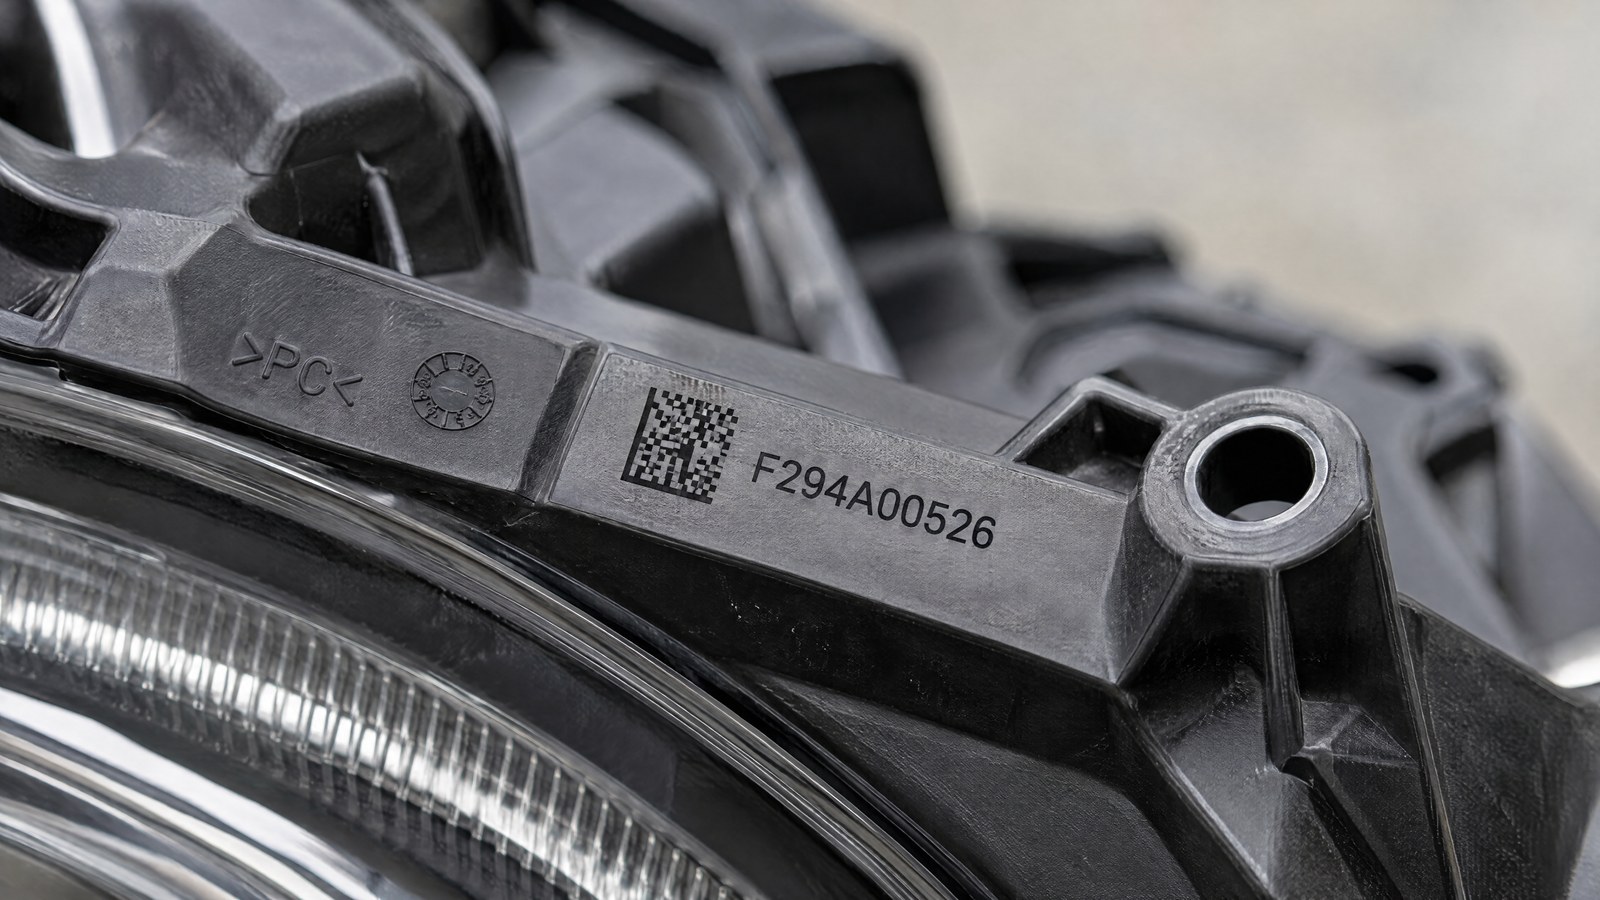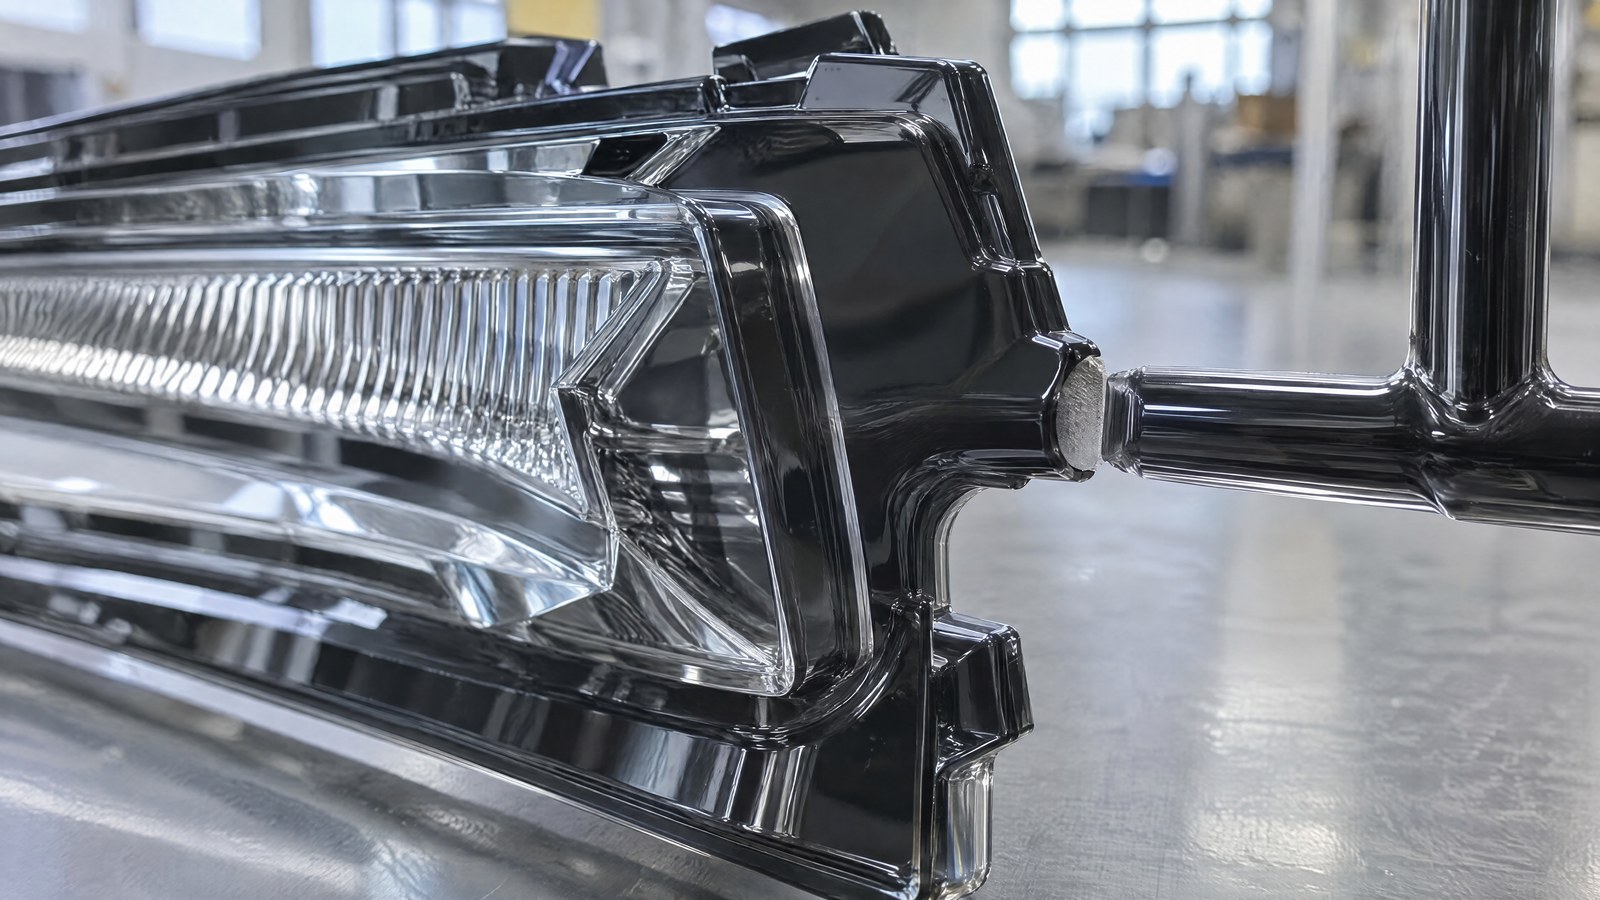
Anyone who injection-molds automotive components knows the path a sprue takes after the press: the part comes out of the mold with the feed channel still attached, gets collected in a bin, and is carried to a separate station where an operator or a trimming press removes the gate. It’s an operation that lives off-line, and like everything off-line it adds material handling, work-in-process buffers, and waiting times between molding and finishing.
Bringing degating back downstream of the press, inside the same cell, is technically possible with the laser, which cuts the gate without contact. But doing it doesn’t simply mean placing a source next to the mold: it means designing a cell that removes the sprue in the time the press takes to produce the next molding, without becoming the bottleneck of the line.
The in-line degating cell rests on five design choices that have to be decided together: how the part reaches the laser, how it is positioned, how the fumes are managed, how the station talks to the press, and how the cut edge is inspected. None of these choices is independent of the others.
Why mechanical sprue cutting shows its limits
Mechanical trimming removes the gate with a blade or a pincer. It works, but it transfers a cutting stress to the part, and on rigid or brittle materials — reinforced engineering polymers, polycarbonate, the PMMA of optical parts — that stress turns into microcracks starting from the gate point, into burrs, and into a residual edge that varies from part to part as the tool wears. On a cosmetic or optical component, where the gate is close to a functional surface, these defects become scrap.
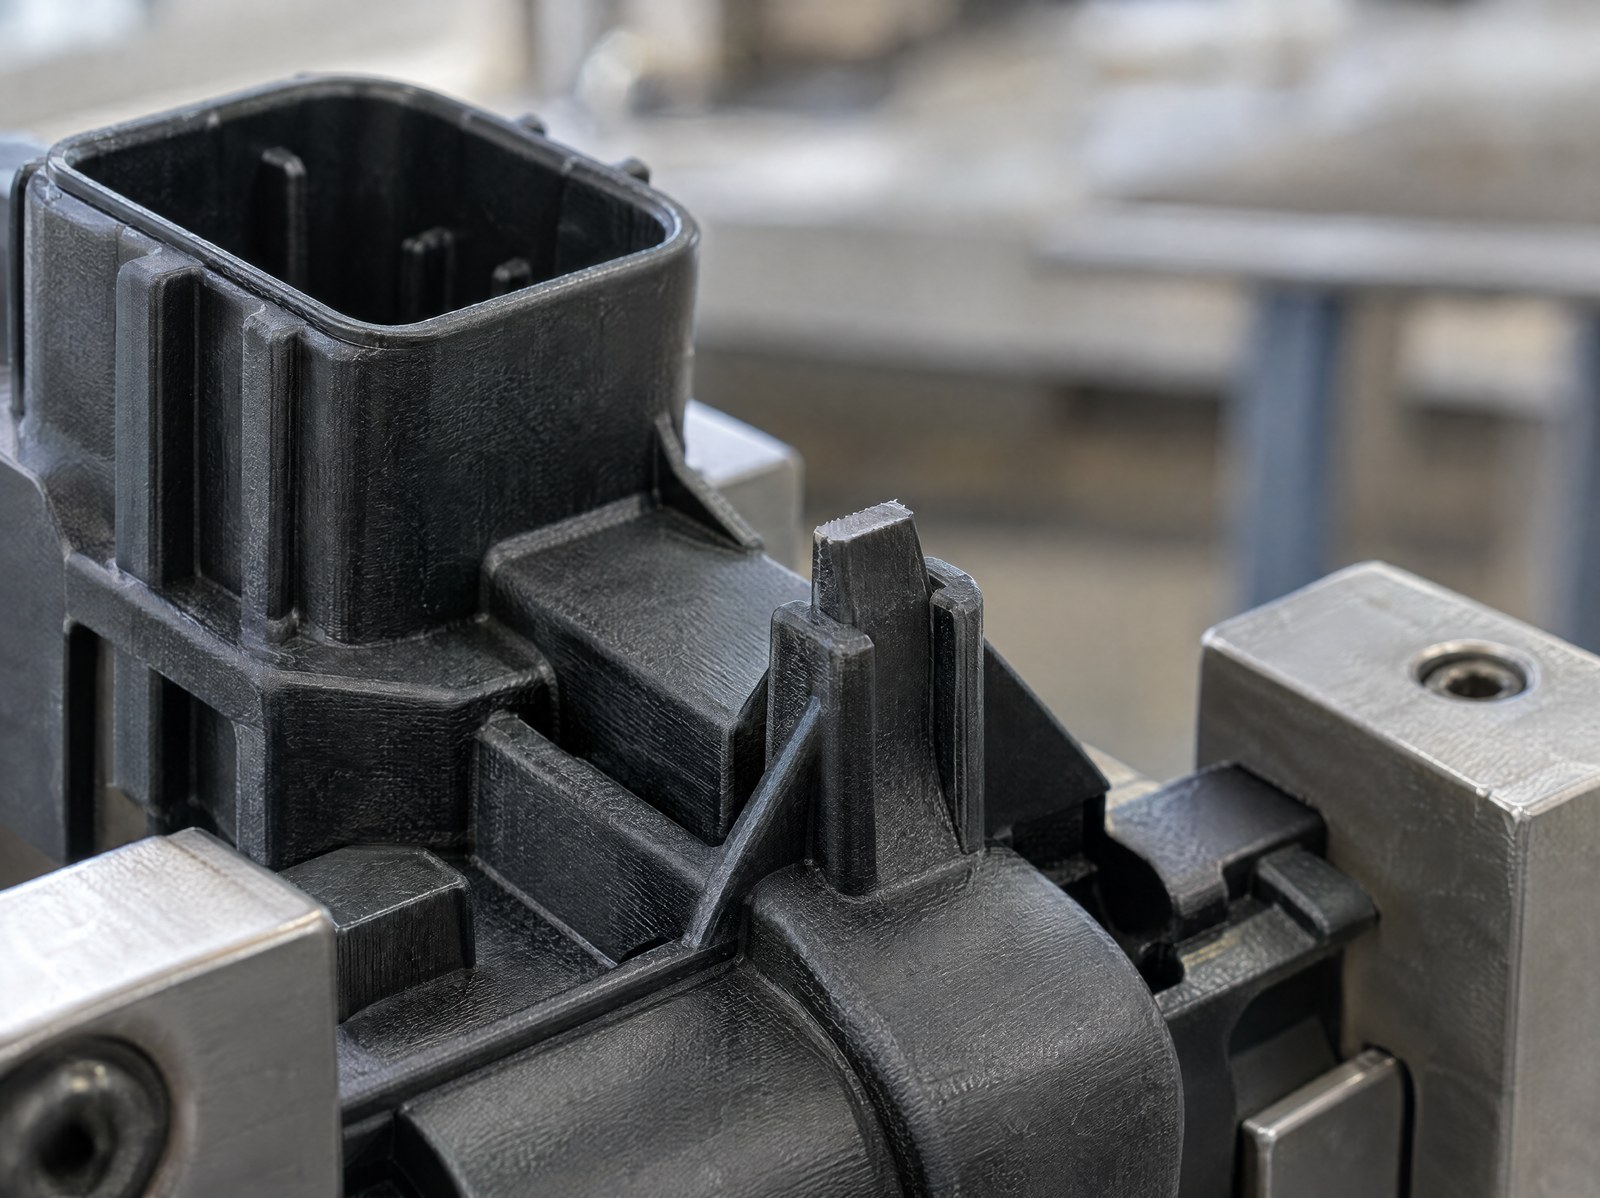
The laser works differently: it ablates the material at the gate point with no mechanical force on the part. The result is a repeatable separation line, with a clean, well-defined edge that doesn’t depend on the sharpness of a blade. On delicate geometries the advantage isn’t theoretical: it’s the absence of the stress that generates cracks. Anyone who wants to dig deeper into the principle of cutting the gate with the beam can start from the article dedicated to degating and sprue removal, which describes its physics.
Staying within the press cycle time: the constraint that decides everything
The parameter that governs the entire cell is the molding cycle time. The press produces a molding at regular intervals, and the degating cell has to complete its own work — pick-up, cut, unload — within that window, otherwise it slows the press down. This is why an in-line cell isn’t designed starting from the laser, but starting from the rhythm of the machine it hooks onto.
The principle that makes this manageable is masked time: while the press closes the mold and injects the next cycle, the robot and the laser station work on the molding just extracted. Degating doesn’t add to the molding time, it hides inside it. When the window is tight, the sequence is optimized by reducing the robot’s movements and bringing the beam onto the gate point with the scan head, without moving the part.
Cell sequence within press cycle timeMold ejectionRobot pickupSprue cuttingFume extractionEdge inspectionPick-up and positioning: where repeatability is won
Laser cutting is as repeatable as the position of the gate point in front of the beam. This is where the robotic pick-up comes in: the gripper picks up the molding just extracted and brings it to the station, or holds the part while the head works. In both cases the geometry of the gate has to present itself to the laser in the same place every time, because a gate that drifts by a few thousandths of an inch relative to the focus produces an incomplete cut or a residue.
For this reason the gripper and the tooling are designed around the specific part, referencing stable zones of the molding — not the gate itself, which is precisely what has to be removed. In cases where the mold family changes often, the reference can be re-acquired with a vision system, so the station locates the gate even in the face of small variations in the part’s position in the gripper.
Fume extraction and optics protection
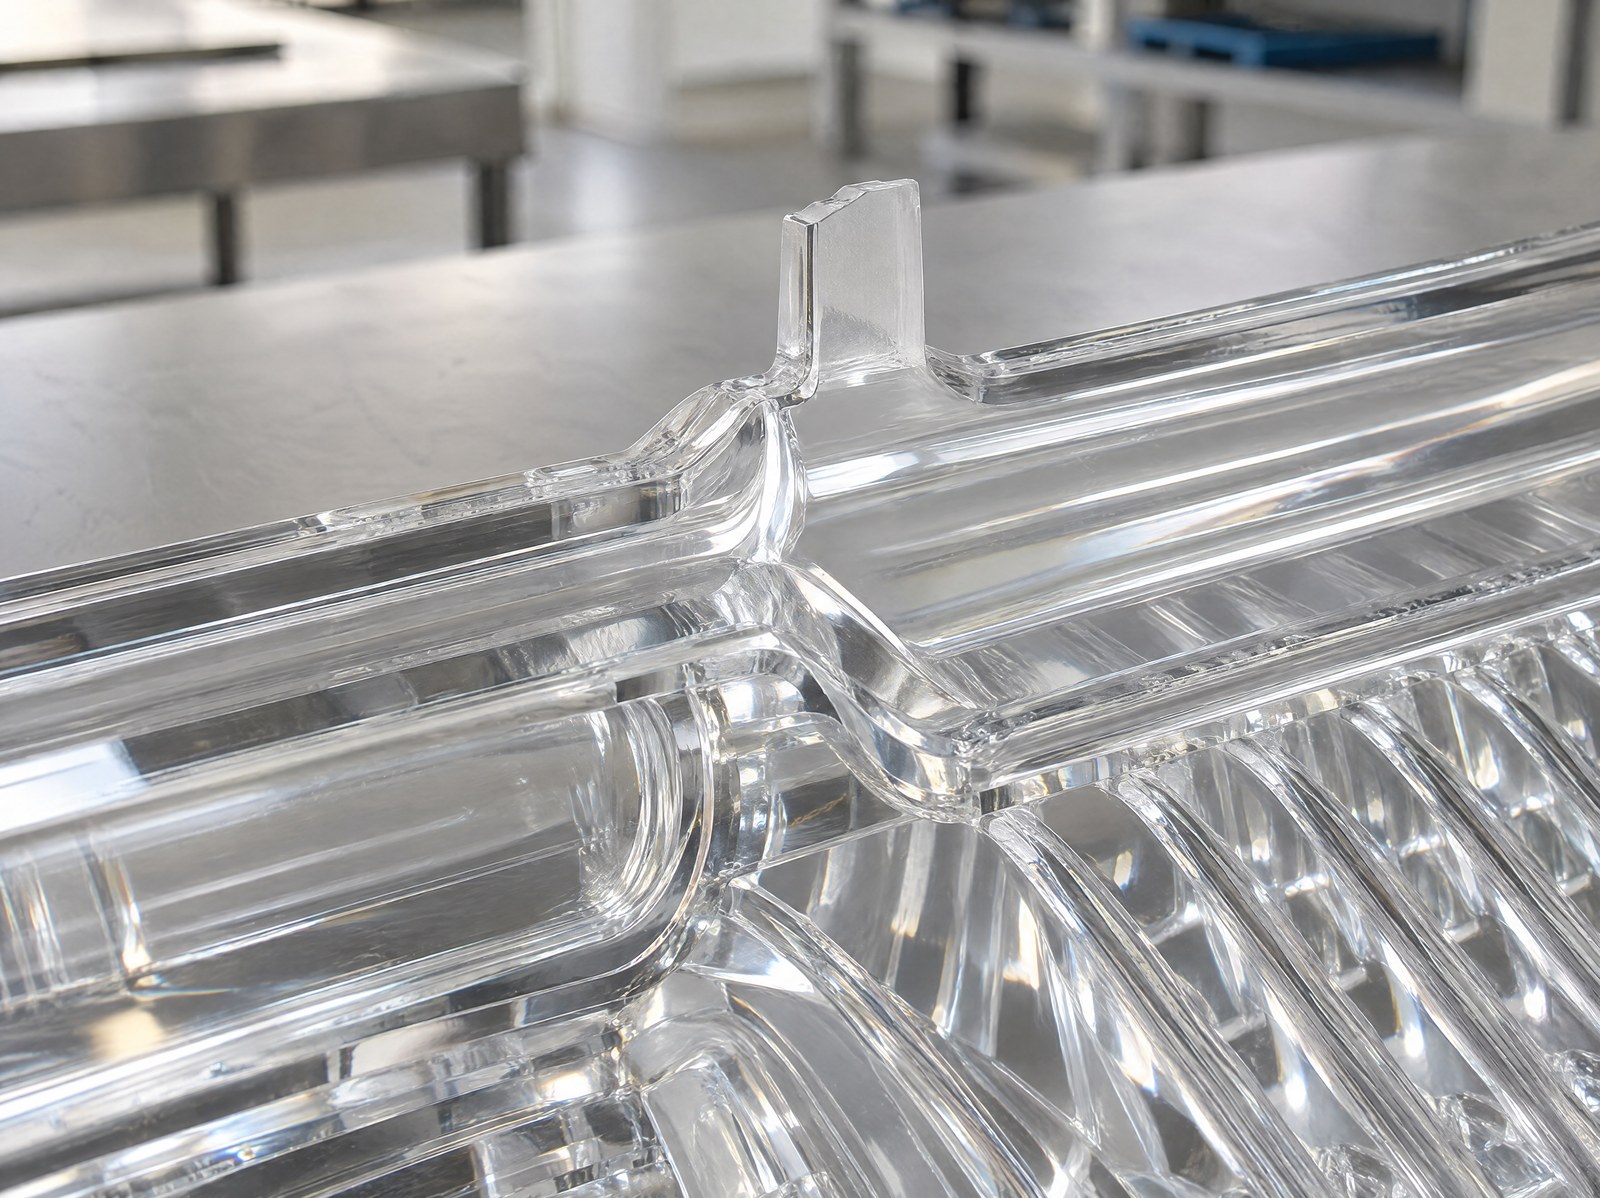
Cutting a polymer with the laser generates fumes and particulate. In a closed cell, if they aren’t captured the instant they form, those products settle on nearby surfaces and on the head’s lens, degrading cut quality over time. On transparent optical parts the problem even has a precise name: the condensation haze that can veil the surface around the worked point, the so-called foggy effect, which on automotive lighting components is an unacceptable cosmetic defect.
The countermeasure is a fume extraction sized and aimed at the cut point, with a flow that drives the particulate away from the worked zone and the optics rather than just refreshing the air in the cell. It’s a detail that decides process consistency across tens of thousands of parts: effective capture keeps the lens clean and stabilizes cut performance, while a generic extraction lets quality slowly slip cycle after cycle.
Synchronization with the press: the handshake that holds the cell together
An in-line cell isn’t a station that works on its own: it’s a node that exchanges signals with the press. The molding control communicates when the mold is open and the part available; the cell confirms it has taken charge, executes, and signals when it is free for the next cycle. This dialogue — the handshake between the two controls — is what guarantees that robot, laser, and press never conflict on timing.
In terms of integration, the laser station behaves like any other automated island on the line and hooks onto the factory systems through standard industrial protocols. The same approach with which LASIT integrates marking and downstream checks into a single cell downstream of a press is described in the case of the FlyPress cell for automotive turbochargers, where laser and test station coexist in a single synchronized cycle.
In-line edge inspection
The final element is verifying the result. At an off-line station the inspection is often visual and on a sampling basis; in-line it pays to make it part of the cycle, with a vision system that inspects the gate zone right after the cut and verifies that the sprue has been removed correctly and that the edge is intact. The part that fails inspection is scrapped before moving on, so the defect doesn’t propagate downstream.
This inspection remains a geometric and cosmetic check of the edge, and should not be confused with a laboratory validation: it serves to keep the process within the limits set during setup, cycle after cycle, and to give the line an objective data point on every part worked.
Who it’s designed for (and who it isn’t)
The integrated laser degating cell makes sense where the volume is continuous and off-line degating is already a bottleneck: series molding of automotive components, optical and cosmetic parts where mechanical cutting leaves cracks or burrs, parts where the gate is close to a functional surface. In these cases bringing the operation back inside the cell eliminates material handling, buffers, and the variability of manual cutting.
It is not, however, the obvious choice for low-volume production, for very large gates on tough materials where a sturdy trimming press does its job without penalizing the part, or for mold families so heterogeneous that a repeatable tooling becomes impractical. In those contexts a dedicated station, even off-line, remains the most rational solution. The laser is worth it when the edge has to be clean and repeatable, when the material suffers under mechanical stress, and when the rhythm of the press demands that the flow not be broken.

Business Development Director | LASIT
Business Development Director at LASIT, Giandomenico Ievoli is responsible for the commercial direction and strategic development of the company. He leads business development activities at national and international level, contributing to the growth and expansion of LASIT in global markets.