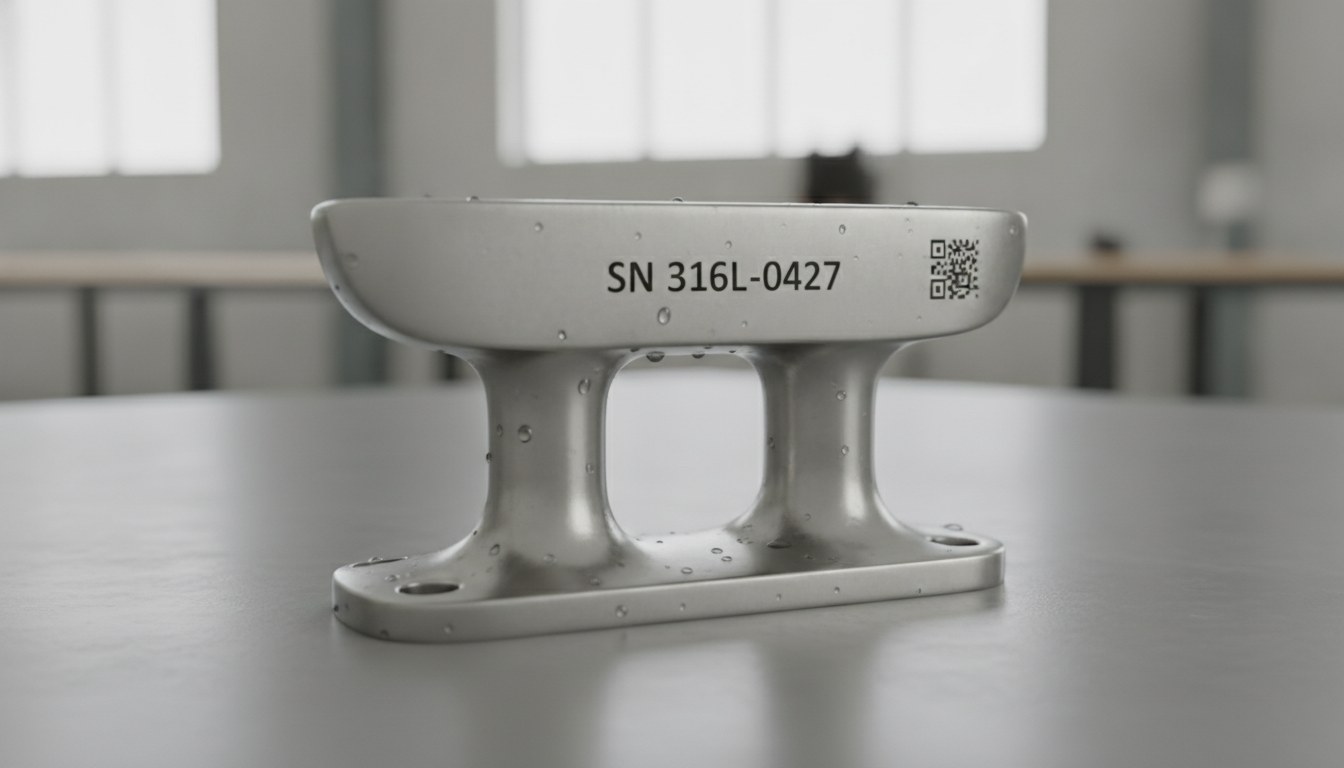
Companies that produce blocks, stanchions, pulpit bases, cleats and deck identification plates work with a constraint that has nothing to do with aesthetics: the HIN code, the serial number and the manufacturer’s data must remain legible for decades, in continuous service under salt fog, UV rays and wet-dry cycles. On some of these components marking is not a choice, it is a regulatory obligation.
The problem is that the sea does not forgive process errors. A marking designed with industrial logic — deep, high-contrast, “clearly visible at inspection” — on a marine component can become the point where corrosion begins. And once localized corrosion attacks the bottom of a character or of a DataMatrix module, the code stops being legible long before the end of the part’s service life.

Fiber laser marking tackles exactly this trade-off: obtaining a permanent, high-contrast mark without compromising the layer that protects the metal from corrosion. But it requires thinking about the material, not about the character.
Deck materials and how they react to fiber
Deck hardware centers on three families of materials, each with a different corrosion-protection mechanism. Marine stainless steel, typically AISI 316L, resists thanks to a thin passive layer of chromium oxide that reforms spontaneously in the presence of oxygen. Marine aluminum is almost always anodized: the protection is the compact anodized layer obtained electrochemically. Fiberglass, finally, entrusts the barrier to the gelcoat.

The fiber laser at 1064 nm works well on the two metals, because its wavelength is efficiently absorbed by metal surfaces and allows the heat input to be modulated from simple surface oxidation all the way to ablation. On fiberglass, however, that same wavelength is poorly absorbed by the gelcoat and glass fibers: the result is inconsistent, and it is one of the reasons why on these components a dedicated metal plate is often preferred.
Why marking that is too deep opens corrosion pathways
On stainless steel the industrial temptation is to engrave deep, to ensure the code “won’t wear off”. In a marine environment this is counterproductive. Removing material means locally removing the passive layer and creating micro-grooves with an irregular surface: geometries that promote crevice corrosion and pitting, the two localized attack mechanisms typical of salt water. The bottom of an engraved character becomes a trap where chlorides stagnate.

Then there is the thermal issue. Excessive and prolonged heat input can bring the steel into the sensitization range, in which chromium precipitates as carbides at the grain boundaries and depletes the chromium in the adjacent zones — precisely those that should ensure passivity. A marking that is too “thermal” can therefore weaken the corrosion resistance around the mark, even without removing much material.
The process rule that follows is counterintuitive with respect to industrial habit: at sea the best marking is often the least invasive, not the deepest. What matters is the stability of the contrast over time, not the depth of the groove.
Controlled annealing: marking stainless steel without breaking its passivity
On stainless steel the approach consistent with marine life is annealing marking: the beam heats the surface in a controlled way and generates a dark, adherent oxide layer, without removing metal. The character or module stays flush with the surface, which remains smooth and continuous. There are no grooves where chlorides can trigger pitting, and the surrounding passive layer remains essentially intact.
The delicate point is that annealing must be calibrated: an oxide layer that is too thick or a poorly distributed energy density can themselves become a defect. This is where the choice of parameters — power, frequency, speed, line overlap — stops being an aesthetic matter and becomes a matter of durability. The verification question is not “is it legible today?”, but “is it legible after a prolonged cycle in salt fog according to ISO 9227 and after UV exposure?”.
Anodized aluminum: marking without exposing the metal
On anodized aluminum the reasoning is the mirror image. The anodized layer is the protection: engraving it down to the base metal exposes bare aluminum right at the marking point, which becomes a corrosion trigger and, on colored anodized parts, a light stain. The goal is to obtain contrast by modifying the anodized layer, not removing it.
With fiber you work at low fluence, to create contrast within the anodizing thickness while keeping the barrier continuous. It is a tighter balance than on stainless steel, because the anodized layer has reduced thicknesses: the process window must be found on the customer’s actual material, taking into account the type of anodizing and any coloring.
The marine requirement and the industrial requirement are not the same thing
Many marking specifications are born for the industrial environment, where the reference test is passing a salt fog cycle in the laboratory: a one-off qualification. The marine component, on the other hand, lives in that environment for decades, continuously, with the added burden of UV irradiation and mechanical stress. The difference is not one of degree, it is one of nature: at sea the marking must not only survive the test, it must not introduce a weak point itself in the part’s corrosion resistance.
| Aspect | Industrial requirement | Marine requirement |
|---|---|---|
| Environment | Salt fog test in the laboratory | Continuous exposure for decades to salt and UV |
| Purpose of the mark | Legibility and contrast at inspection | Permanence without triggering localized corrosion |
| Depth | Often greater to guarantee the mark | Minimal: preserve the passive or anodized layer |
| Verification | Immediate legibility of the code | Legibility after ISO 9227 salt fog and UV exposure |
On top of this comes the obligation. For recreational craft, European regulation requires the permanent application of the hull identification number (HIN/CIN) and of the builder’s plate, with indelibility and tamper-resistance requirements defined by industry standards. Traceability here is not a process bonus: it is a compliance requirement that the mark must guarantee for the entire life of the boat.
When a plate is enough and when direct marking is needed
Direct fiber marking makes sense on metal deck components — blocks, bases, stanchions, stainless steel and aluminum hardware — where the mark can be integrated into the material without compromising its protection. It is the natural choice when the part is metal, the surface allows it, and you want to eliminate the risk of an applied label or plate detaching in service.
It is not, however, the universal answer. On fiberglass and composites, where fiber works inconsistently, a marked metal plate in stainless steel or anodized aluminum, permanently fixed, remains the most solid and verifiable solution. The same applies when regulation requires a specific location or format that the component does not offer.
In short: at sea the criterion is not how deep or conspicuous the mark is, but how long it stays legible without itself becoming a corrosion trigger. Defining this balance — material by material, with real resistance testing — is what separates a marking that lasts a season from one that lasts as long as the boat.

Applications Manager | LASIT
Applications Manager at LASIT for over 20 years, Mario Palmieri oversees the management and development of the company’s laser laboratory. He is responsible for conducting sample tests for customers, supporting the automotive, medical, aerospace and electronics sectors in identifying the most suitable laser marking solution for their needs.