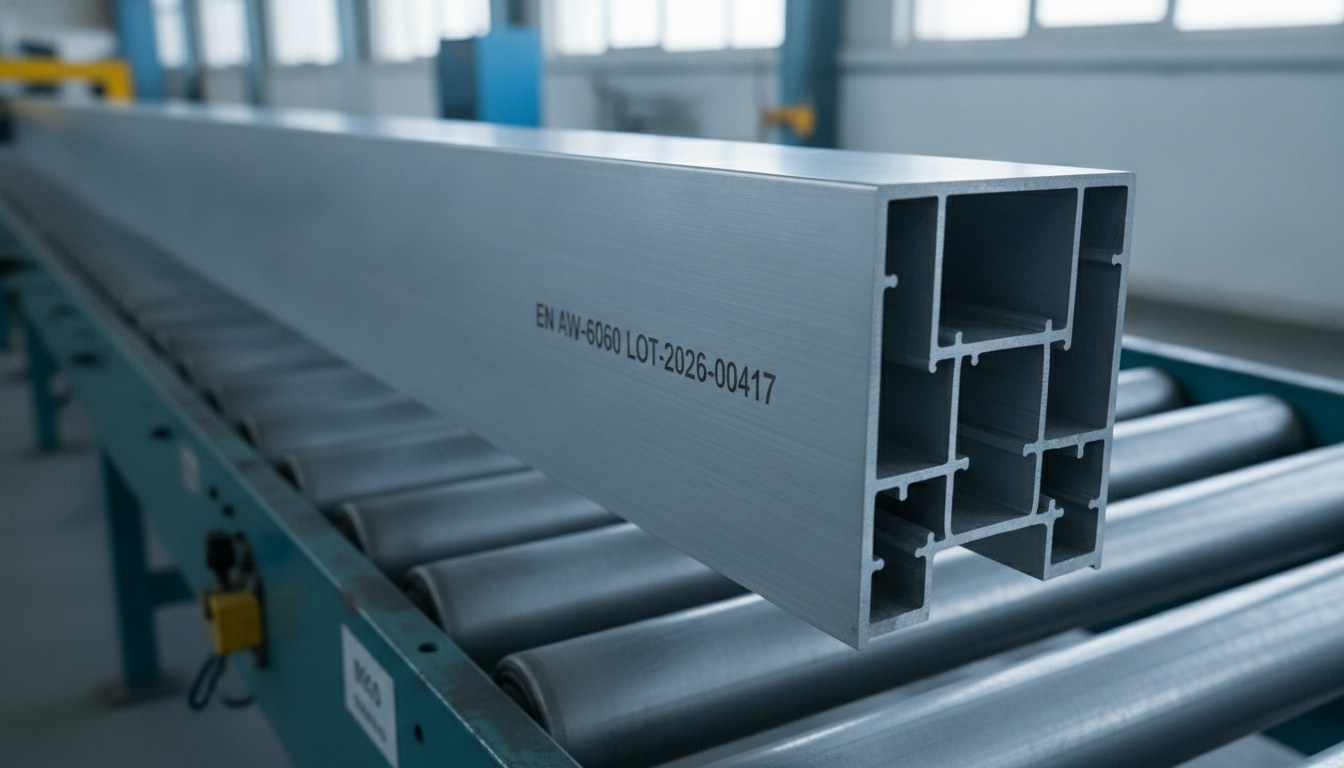
Anyone who extrudes aluminum profiles for window and door frames knows the rhythm of the line: the bar comes off the press, passes through the cooling table and the stretcher, and reaches the cut-to-length station in a flow that does not tolerate interruptions. Within this flow the identification marking — alloy, batch, cast, order reference — has to find its place without becoming the station that slows everything else down.
The problem is not marking aluminum: a fiber source has been doing that for years with contrast and permanence. The problem is marking it while it moves, on a product that is continuous by nature and often cannot be stopped bar by bar. This is where on-the-fly marking comes in — marking on the move, synchronised with the actual advance of the line.
Marking on the move is not simply marking faster: it is a matter of synchronisation, of controlling graphic distortion and of integrating with the upstream and downstream stations. Getting it right means deciding where, how and at what speed marking enters the extrusion process.
The continuous product that never stops
An extruded bar is not a discrete part that presents itself to the laser, stops, gets marked and starts again. It is a semi-finished product several yards long that runs along a roller conveyor at a speed set by the upstream stations. Stopping the advance in order to mark means introducing a build-up, a buffer or a dead time that propagates across the whole line. At low volumes this is acceptable; in continuous production it becomes the bottleneck.
This is the same logic that governs the marking of coil materials, where the strip never stops: anyone familiar with continuous production on tape will find the same underlying constraint on the extruded profile. The difference is that here the substrate is solid, rigid metal, with a visible face that will end up before the eyes of the window fabricator and the end customer.
Encoder synchronisation: what marking on the fly really means
On-the-fly marking rests on a simple yet decisive component: an encoder fitted to the drive mechanism, which reports the linear displacement of the bar in real time. The marking controller reads this position instant by instant and shifts the deflection of the galvanometer head so that the beam follows the part while drawing the character. The text stays fixed relative to the metal even though the metal is moving beneath the head.
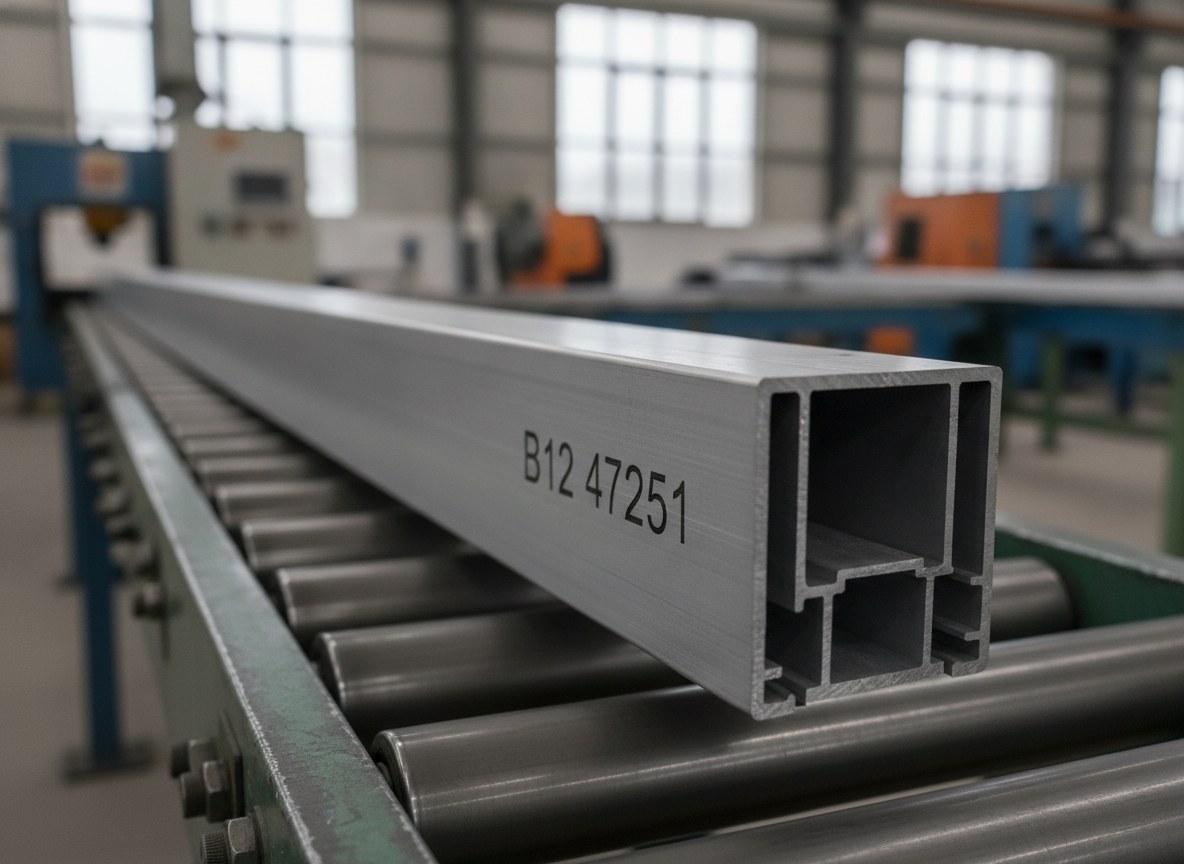
The critical point is that speed must not be estimated, it must be measured: if the software works from a nominal speed while the line slows down or speeds up, the calculated position diverges from the real one and the marking shifts. The encoder closes this loop. The 1064 nm wavelength of the fiber and the galvanometer optics remain the same as in static marking: what changes is that the reference frame is no longer the stationary part, but the dynamic coordinate supplied by the encoder.
Graphic distortion and the line speed limit
Without compensation, marking a moving part produces a typical artefact: the characters lean in the direction of travel, like an unwanted italic, and two-dimensional codes lose their orthogonality. On-the-fly compensation corrects this drift by reconstructing the geometry in dynamic coordinates, but the correction has a physical limit. Every marked element requires a minimum tracing time: the faster the line, the more the part advances during that time, and the more the system has to chase it.
Beyond threshold: switch to stop&markThe result is a threshold: up to a certain line speed the quality remains stable, beyond that threshold the usable window narrows and the result deteriorates, especially with dense content. A short alphanumeric string withstands higher speeds than a DataMatrix, which packs many cells into a fraction of an inch and requires more marking time to stay legible. Defining this threshold on the actual content — not on a catalog figure — is part of the fine-tuning work.
Anodised, painted or raw: how the marking changes
The window and door profile arrives at the marking station in three very different states, and each responds in its own way. On raw extruded material the fiber works through surface alteration and localised oxidation, producing a dark, permanent mark. On anodised material the beam acts on the oxide layer: on colored anodised profiles the selective removal of the color leaves a clear contrast, while on natural anodised material the result is a lighter, matt mark. On painted profiles — typically powder coating in a RAL shade — the laser removes the coating film, exposing the substrate.
These are well-established mechanisms on aluminum, and we covered them in detail in our in-depth article on laser marking on aluminum. The practical consequence, on the line, is that the parameters are not the same for all three states: if the same line handles raw, anodised and painted profiles, the cycle has to recall the correct parameter set based on the type of bar passing through.
Alloy, batch and the choice of the non-visible face
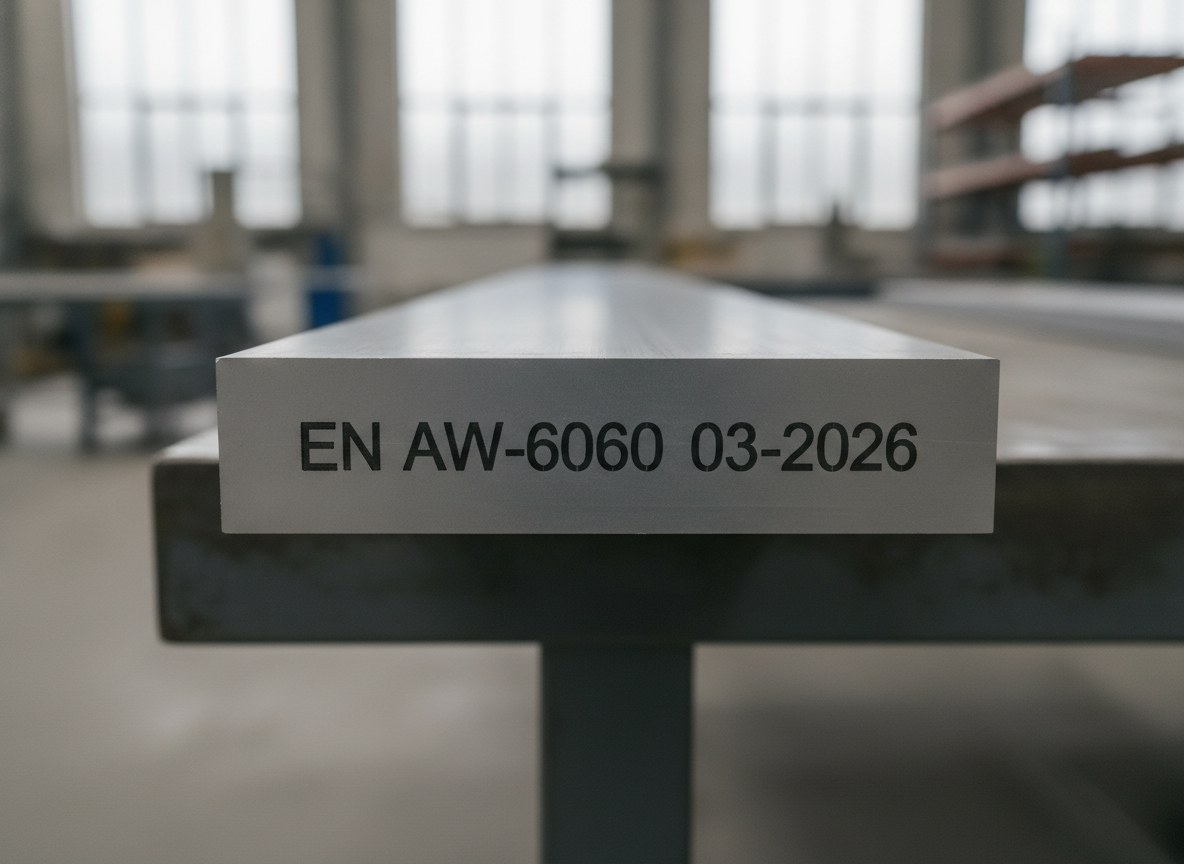
The content to be marked, in window and door frames, is almost always the same core of information: the alloy designation — EN AW-6060 and EN AW-6063 prevail on architectural profiles — cast number, batch and order reference. This data accompanies the profile towards cutting, assembly with thermal break and mechanical checks, and must stay associated with the right bar throughout the entire chain.
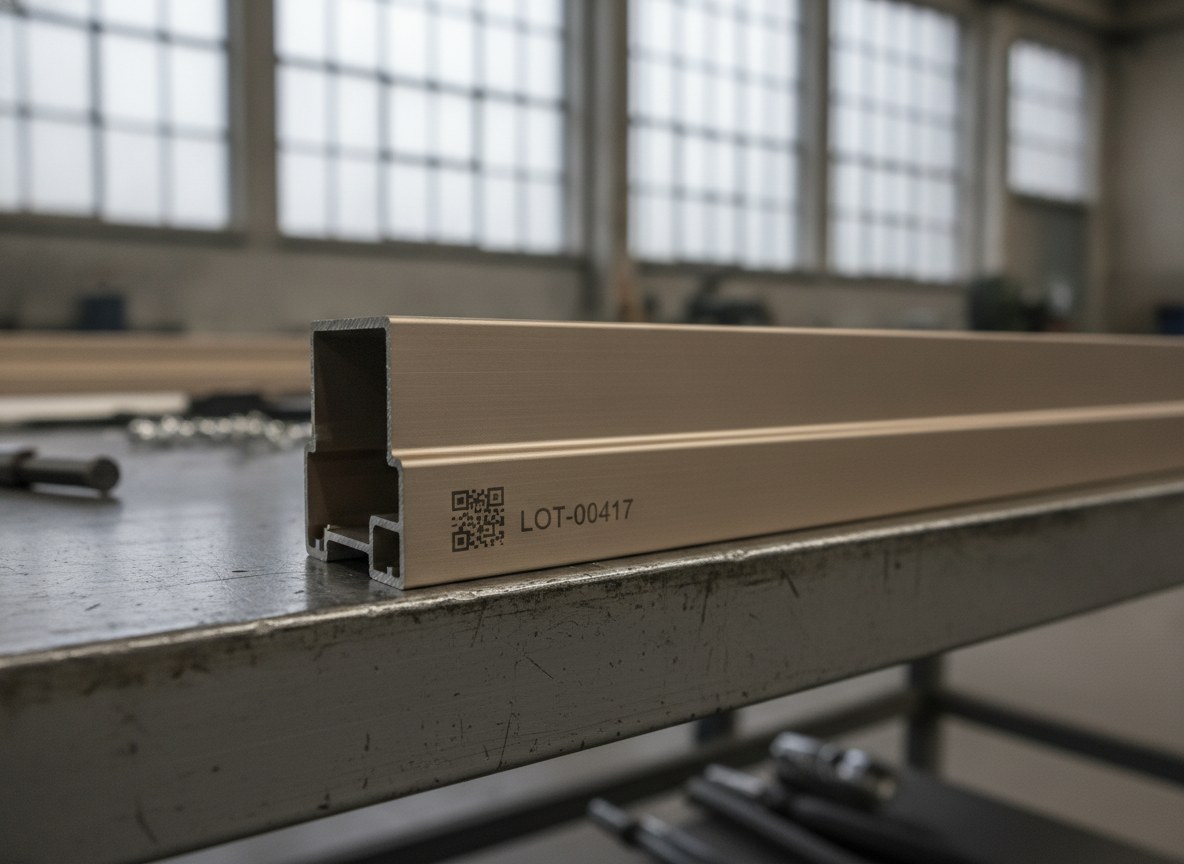
Here a decision comes into play that is as much technical as aesthetic: where to mark. The profile has a visible face, meant to remain exposed once the frame is fitted, and internal channels or grooves that disappear under gaskets, brush seals and joints. Placing the marking on a non-visible face preserves the appearance of the profile without giving up traceability: the code is there, legible during processing, but it does not compromise the visible finish of the completed frame.
On legibility, a distinction is worth keeping clear: code grading is the quality check that can be applied in-line, whereas formal verification requires controlled laboratory conditions. On the line, grading is monitored to catch a degraded marking immediately; for the difference between the levels of control we devoted an article to the difference between reading, grading and code verification.
Integration with cut-to-length
On-the-fly marking only makes full sense if it communicates with the neighbouring stations, and the most critical of these is cut-to-length. The continuous bar becomes segments, and each segment must carry its own identification: this makes it necessary to coordinate the repetition of the marking with the cutting pitch, so that no cut piece is left without a code or carries one truncated in half. On-the-fly marking makes it possible to write on the moving bar and to synchronise the information with the cutting logic, with no dedicated stops.
It is the same principle by which marking, when well integrated, ceases to be an isolated station and becomes an intelligent node of the production line. On this kind of integration, where a laser to be inserted into the existing chain receives data and commands from the line controller, we have also described the case of a fiber laser integrated into a production line: the logic can be transferred from components to the continuous profile.
On-the-fly or stop&mark? Where the threshold lies (who it is for and who it is not)
The final question is an honest one: do you really need to mark on the fly? The answer depends on a comparison between two ways of working. In stop&mark the profile halts for the marking time and then restarts: it is the simplest choice, it delivers the highest quality because it marks on a stationary part, and it makes sense when the line can index, volumes are limited, format changes are frequent or the content is complex. In on-the-fly the bar never stops: it is the mandatory choice when the extrusion is genuinely continuous and every stop propagates a build-up upstream.
The threshold, then, is not a universal number but a crossing point between three factors: the required productivity, the real possibility of stopping the line and the density of the content to be marked. As long as the line tolerates micro-stops and volumes allow it, stop&mark remains the rational solution. When stopping costs more than the simplicity is worth, or when the flow admits no pauses, on-the-fly becomes the only viable route.
On-the-fly marking of aluminum profiles is designed for those who extrude continuously, mark alloy and batch on every bar and integrate a high-rate cut-to-length downstream. It is not, on the other hand, the choice to pursue for those working in short batches, with many profile changes and a line that stops anyway for other reasons: in that context a stop&mark station, simpler to manage, meets the need with less complexity. The right choice is decided on the process, not on the principle.

Business Development Director | LASIT
Business Development Director at LASIT, Giandomenico Ievoli is responsible for the commercial direction and strategic development of the company. He leads business development activities at national and international level, contributing to the growth and expansion of LASIT in global markets.