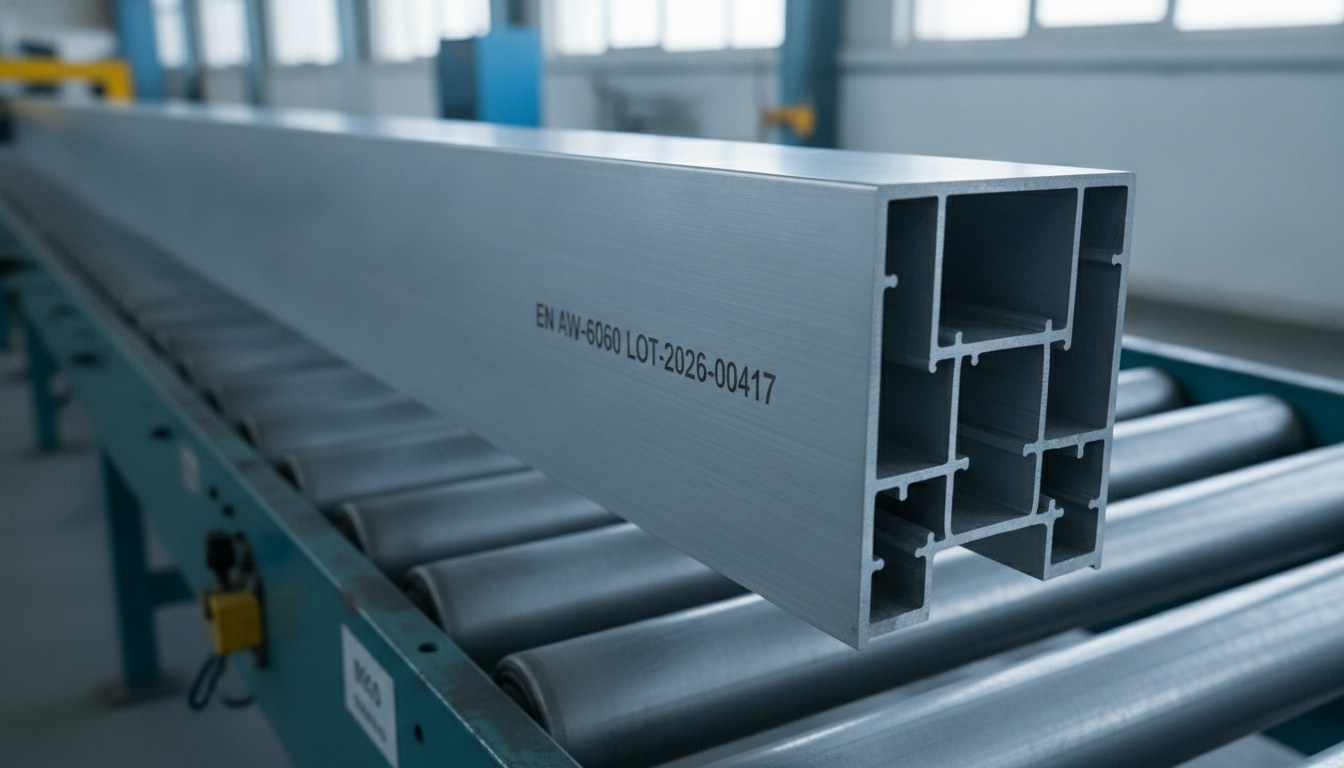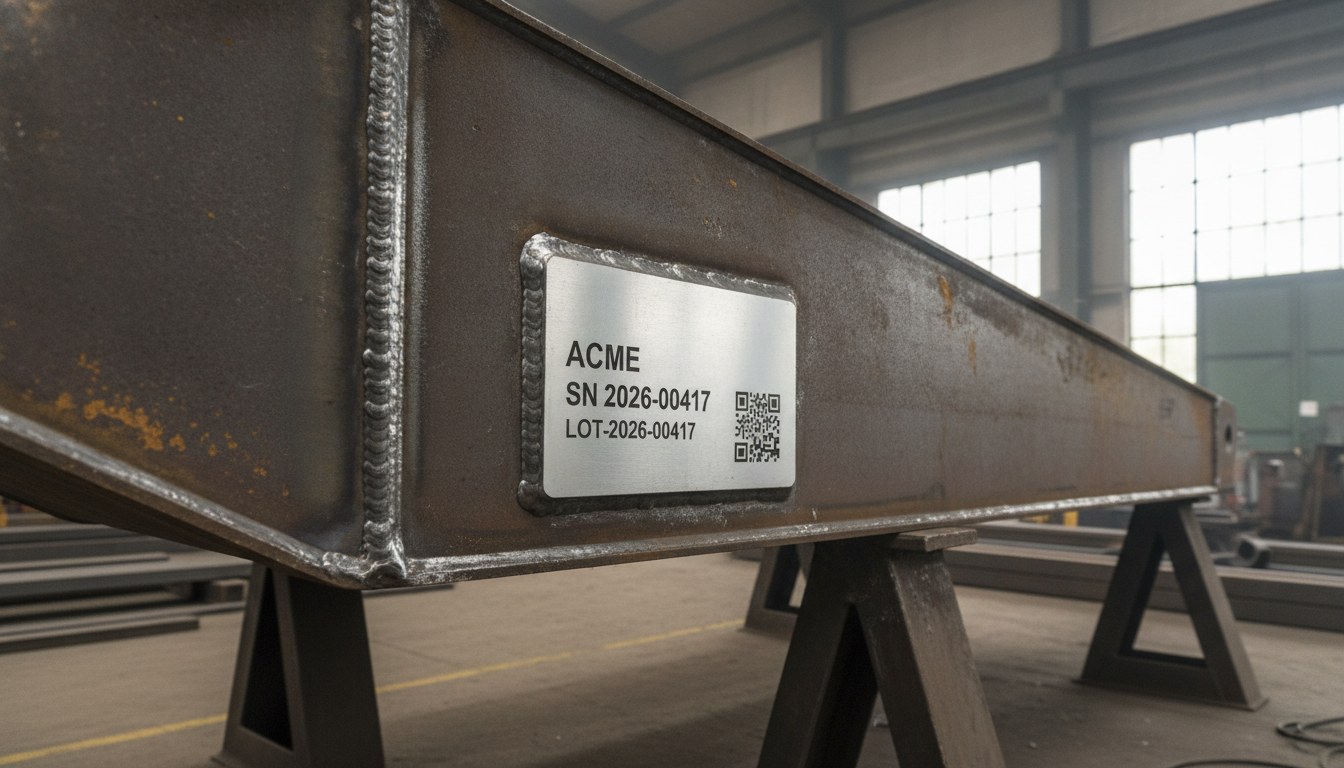
Companies that design and build frames, arms, side rails, buckets and chassis for earthmoving and agricultural machinery work every day with welded structures that weigh hundreds of pounds and easily exceed five feet in length. Marking is the last operation in the cycle, but it is the one that imprints on the component the data meant to last for its entire life: manufacturer identifier, serial number, batch references and the nameplate data required for compliance. On these parts, marking steel is not the problem — a 1064 nm fiber laser has been engraving raw carbon steel without difficulty for decades.
The problem is reaching it. An excavator arm or a tractor side rail does not fit into a standard marking cabin, and handling it means an overhead crane, slings and downtime that fragments the cycle. On a large part the constraint is not the physics of marking, but the access geometry: where the point to be marked is located, how the beam reaches it and how the code is read once the metal is welded, oxidized and covered in scale.
The logic flips: when the part can’t come to the laser, it’s the laser that must come to the part. It is around this choice that the right system is built.
The constraint isn’t the metal, it’s the accessibility of the marking point
On a benchtop component the marking point is always in focus, under the head, perpendicular to the beam. On a welded structure weighing several hundred pounds this condition has to be created: the point to be marked may sit on a plate recessed between two crossmembers, on the back of an angled arm or on a downward-facing flange. The operator can’t rotate the part the way they would with small components, and every repositioning with the overhead crane introduces play and time.
That is why the assessment starts from the physical map of the part: overall size, weight, center of gravity, and above all the position and orientation of the marking area relative to how the component arrives at the workstation. Two frames with the same nameplate data, but with the identification plate positioned differently, require different access solutions. It is a manufacturing consideration, not a laboratory one.
Bringing the beam to the part: gantry, robot and large-volume cabins
When the component is too large or too heavy to be handled, the system takes on the movement. There are three approaches and they often combine. The first is the gantry structure: the marking head moves on motorized axes above a wide work surface, reaching distant areas without touching the part, which stays where the overhead crane set it down. This is the approach of large-format machines like Fly Gantry MAG, built precisely to work on oversized parts.
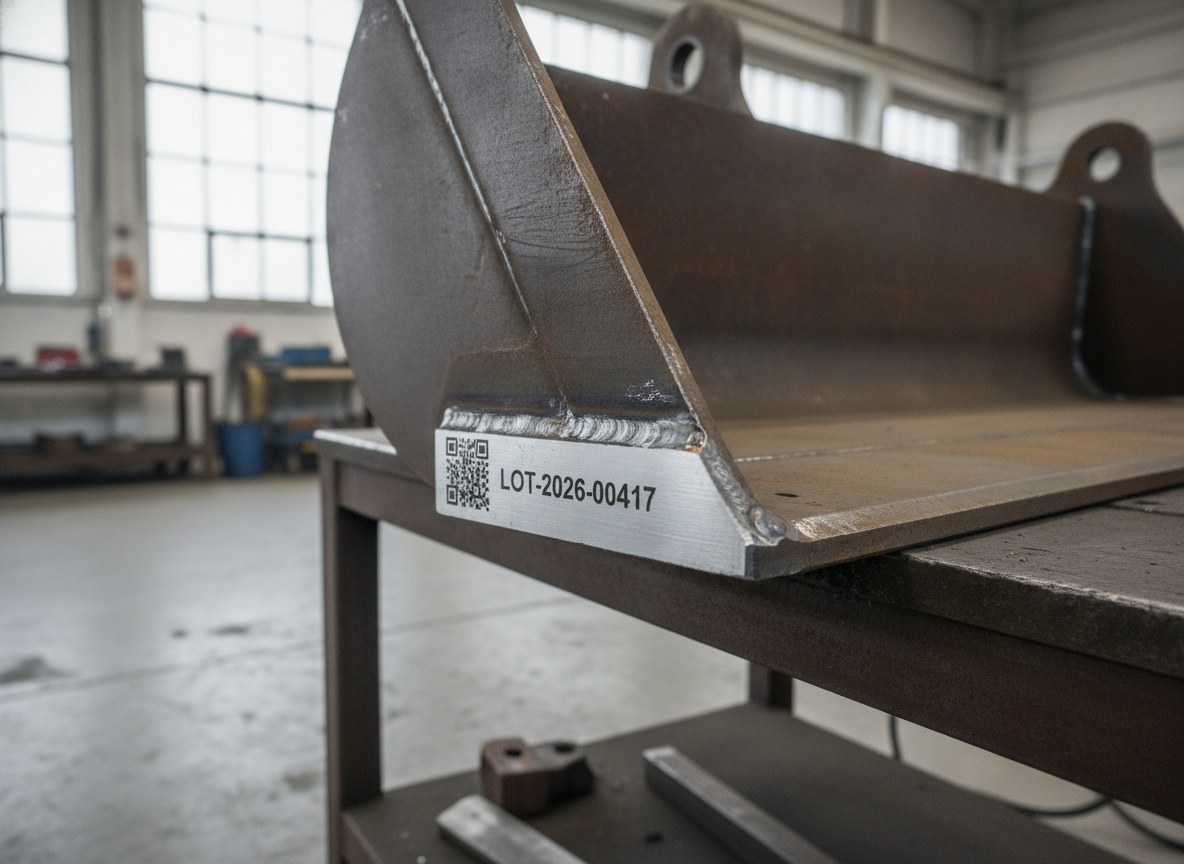
The second is robotic integration: an articulated arm brings the scan head to the point to be marked, following paths that navigate around complex geometries — useful when the marking area faces awkward directions. The third is the large-volume cabin with facilitated loading: systems like TowerSwipe, with side loading, are designed to move heavy and bulky components in and out without lifting them over a threshold. In every case marking can be handled as a standalone station or integrated in line, downstream of welding or surface treatment.
On extended marking fields, where a deep part presents different focus heights from point to point, hybrid XY-axis plus pre-scan configurations are used: the motorized axes cover the travel, while the head handles dynamic focusing along the surface. This is the correct way to keep the beam perpendicular and in focus without sacrificing the work area.
Nameplate data and compliance: what must stay legible
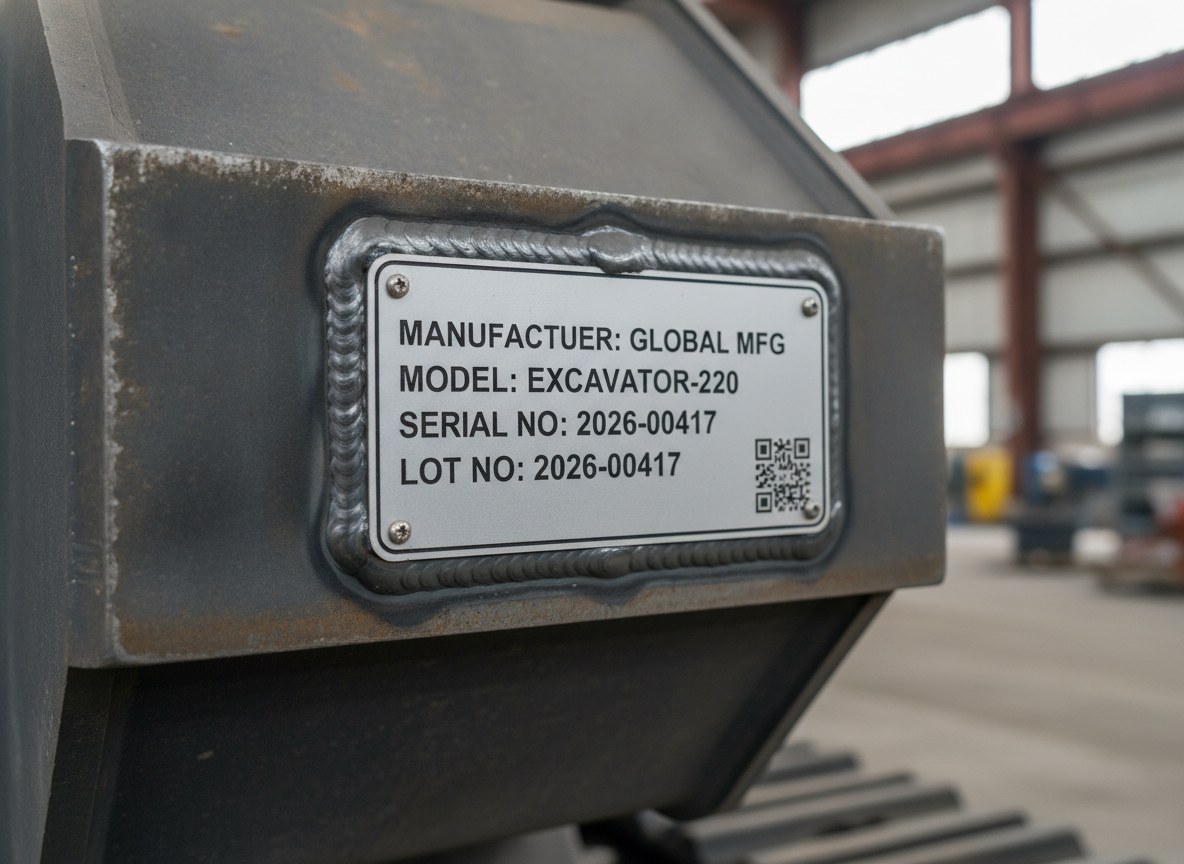
On an agricultural or earthmoving machine, marking the structural components serves a documentary function. On the frame or the identification plate appear the manufacturer’s company name, serial number, model references and the nameplate data required by the machine’s compliance. These are pieces of information that follow the component through the entire supply chain and must stay legible after painting, exposure to weather, mud, impacts and high-pressure washing.
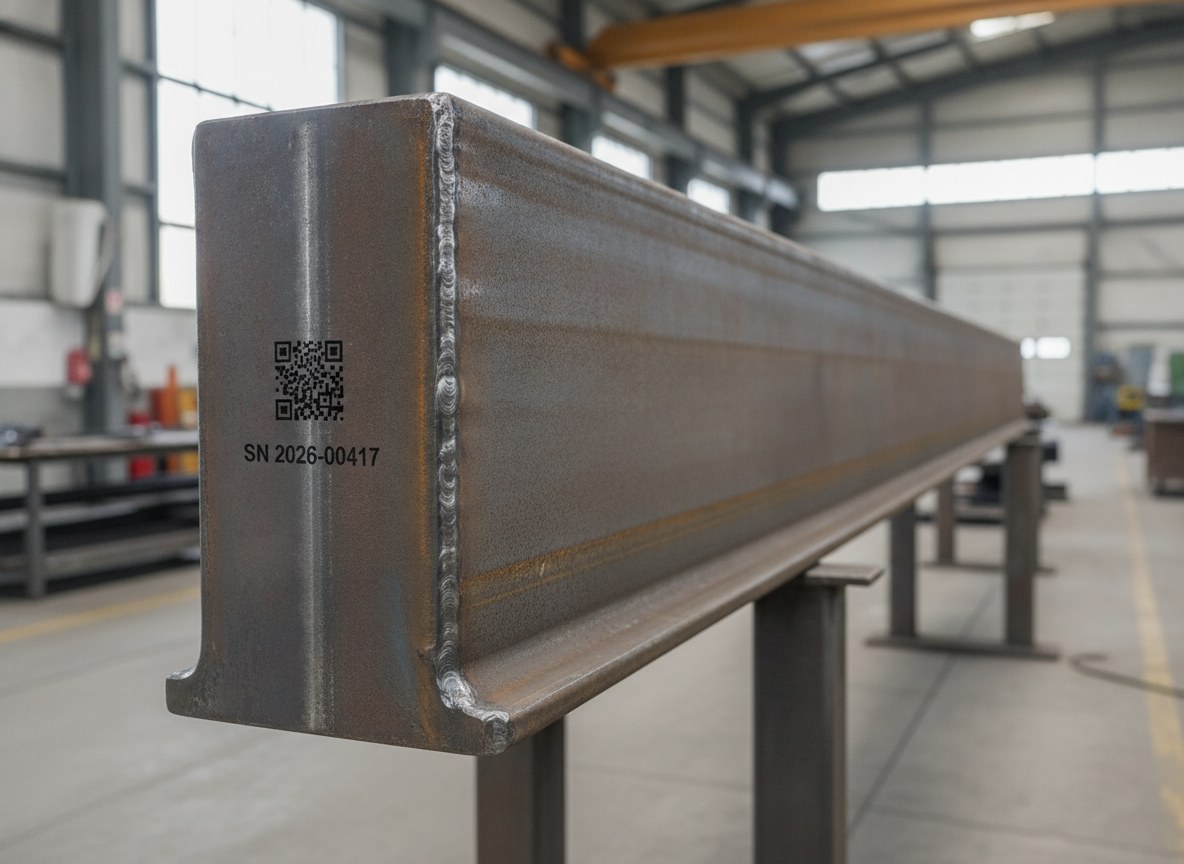
Here direct laser marking has a structural advantage over labels and stamping: it is part of the metal, not a layer applied on top. A DataMatrix code engraved to sufficient depth survives cycles that a label cannot withstand, and stays uniquely associated with that individual part. The topic of verifying code quality — the distinction between simple reading, in-line grading and laboratory verification — is decisive when the data must be guaranteed along the supply chain, as we explored when discussing the difference between reading, grading and code verification.
Reading on welded and oxidized surfaces
The surface of a welded structure is anything but regular. Weld beads, scale, oxide, oxy-cutting traces and uneven roughness create a background on which the contrast of the marking is not a given. A code engraved on a freshly welded edge may sit next to a heat-affected zone with completely different reflectivity, and this tests both the marking and the subsequent optical reading.
The answer lies in process, not brute force. The fiber laser generates contrast through localized material removal and alteration, and the choice of parameters — pitch, fill, number of passes — must be calibrated on the real background, not on an ideal sample. Where needed, the marking area is prepared with a laser cleaning pass that removes oxide and scale before engraving the code, restoring a uniform surface that raw metal does not offer. The result is a DataMatrix with clean modules, readable by an industrial scanner even years and weather later.
Curved or angled geometries add a further layer: marking over a wide field with varying angles of incidence degrades code quality. The techniques for maintaining focus and perpendicularity on non-flat surfaces are the same ones that govern marking on curved and irregular surfaces, and on a welded structure they become an integral part of the marking project.
| Aspect | Direct marking on the part | Attached metal nameplate |
|---|---|---|
| Point accessibility | Requires gantry, robot or large-volume cabin | Marked separately, under controlled conditions |
| Surface quality | Welded and oxidized background, may require preparation | Perfectly flat, uniform contrast |
| Code reading and grading | To be validated on the real background | Simpler and more repeatable |
| Traceability | Code is part of the metal, no attached element | One extra link: fastening and risk of detachment |
Direct marking or attached nameplate
Direct marking on the part is not always the best route. When the point to be marked is entirely inaccessible, when the surface is too irregular to guarantee reliable grading, or when the manufacturer wants a standardized data plate uniform across the whole range, the metal nameplate marked separately and then fixed to the component remains a technically valid solution.
The nameplate is marked under controlled conditions, on a perfectly flat surface at constant focus, which greatly simplifies code reading and grading. The downside is that it introduces an attached element — with its own fastening, the risk of detachment and one extra link in the traceability chain. The choice between direct marking and a nameplate is not ideological: it depends on point accessibility, surface quality and documentary requirements. Often the most robust solution combines the two, with nameplate marking handled by the same system that marks the part.
How to assess marking point accessibility, already at the quotation stage
The typical mistake, when starting a marking project on large structures, is to reason first about the source and then about access. That is the reverse of the correct order. The question to ask at the quotation stage is: where is the point to be marked, how does the part arrive at the workstation and with what movement — of the part or of the beam — is it reached in focus and perpendicular.
That is why a serious assessment starts from the component drawings and from real samples: the marking area is mapped, the overall size is checked, the choice is made between gantry, robot or large-volume cabin, it is established whether the surface requires preparation, and code reading is tested on the actual background, welded and oxidized. Defining these points before supply avoids discovering in production that the robot arm doesn’t reach, or that the DataMatrix can’t be read on the weld bead. Marking point accessibility is a project requirement, exactly like the serial number to be engraved.
Who it’s for (and who it isn’t)
This approach is the natural choice for those who produce heavy and bulky welded structures — frames, arms, buckets, chassis, side rails for earthmoving and agriculture — and need permanent nameplate data and traceable codes on raw, welded and oxidized steel. It is designed for those who today move enormous parts toward a marking station and pay for that transfer in time and complexity.
It is not, however, the right answer for those marking small, easily handled parts, where a benchtop or rotary-table machine remains faster and more efficient in terms of cycle time, nor for those with volumes high enough to instead call for a cell dedicated to a single repetitive component. In short: if your part doesn’t fit in a cabin and the point to be marked is hard to reach, the real issue isn’t which laser to choose, but how to bring the beam to the part and how to read the code where the metal is less cooperative. That is where the success of the project is decided.

Business Development Director | LASIT
Business Development Director at LASIT, Giandomenico Ievoli is responsible for the commercial direction and strategic development of the company. He leads business development activities at national and international level, contributing to the growth and expansion of LASIT in global markets.