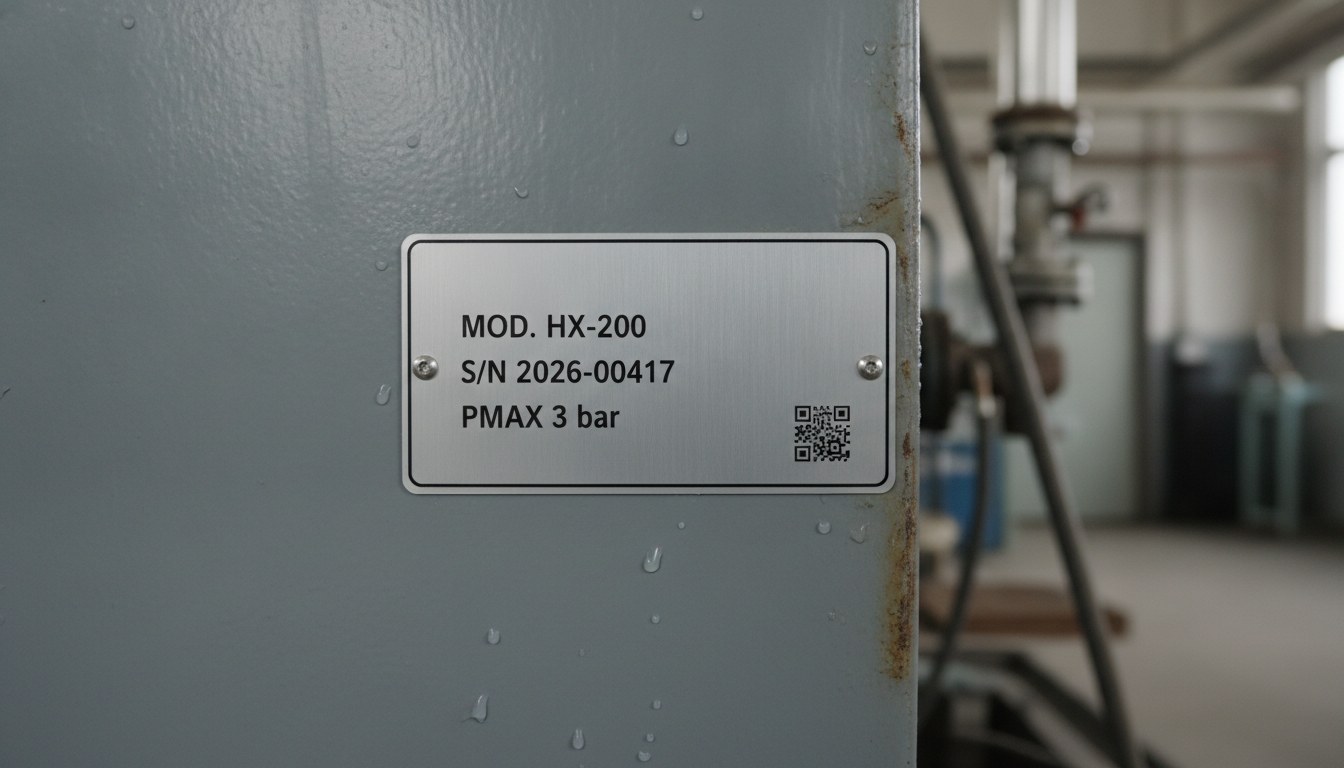
In the heating and plumbing sector, the data plate operates in one of the harshest environments for printed information, and it is often the component given the least attention during design. On a boiler, a heat pump or a heat exchanger installed years ago, the manufacturer, serial number, maximum pressure, output and efficiency class must remain legible precisely when they are needed: during an inspection, a maintenance operation or a compliance check. If by that point the adhesive label has peeled off or the ink has faded, the data is lost, and with it the ability to order the correct spare part or to document the equipment.
The reason lies in the environment. In technical rooms the air is warm and saturated with moisture, and the metal surface continuously crosses above and below the dew point: condensation forms, lingers, evaporates and returns, cycle after cycle. It is a constant stress that acts throughout the equipment’s entire life precisely on the carriers — the glue of an adhesive, the film of an ink — that are supposed to hold the data firmly in place.
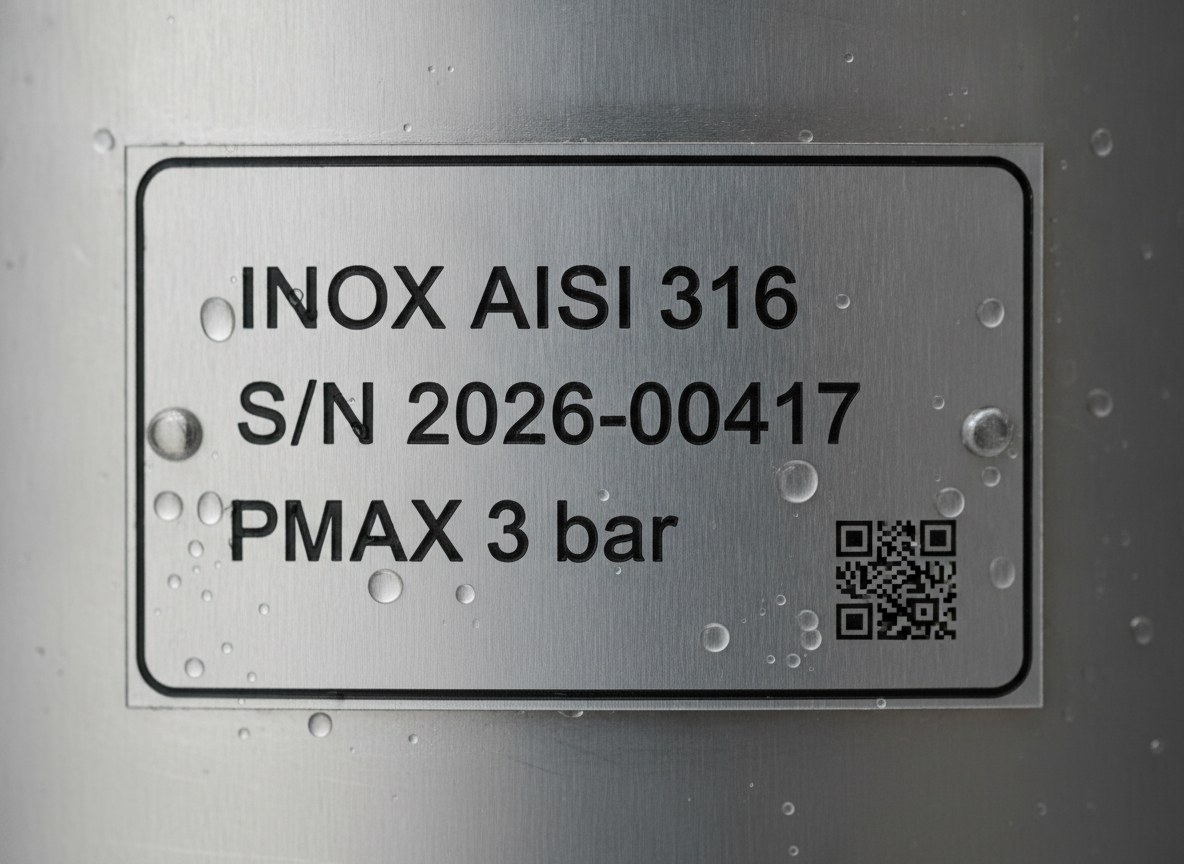
Direct laser marking tackles the problem at its root, because it adds nothing to the surface: it modifies the metal itself. It is not, however, the right answer for every surface and every layout, and it is worth seeing where it truly wins and where a plate or screen printing remains preferable.
Why adhesive and ink fail where condensation is present
The adhesive label depends on its layer of glue, and in a technical room moisture almost always finds a path beneath the film. When the temperature drops below the dew point, water condenses right at the interface, the expansion cycles between metal and adhesive work the edge until it lifts, and from there the peeling advances, carrying with it the oxide that clouds the reading. Ink, whether inkjet or screen-printed, is by definition a thin applied layer: moisture, slightly acidic condensation, cleaning agents and abrasion wear it away. Screen printing with baked inks holds up better than a solvent inkjet, but it remains a film on top of the surface, not part of it. This is where direct laser marking compared to inkjet printing starts from a structural advantage: there is no layer to lose.
The mark is the material, not an applied layer
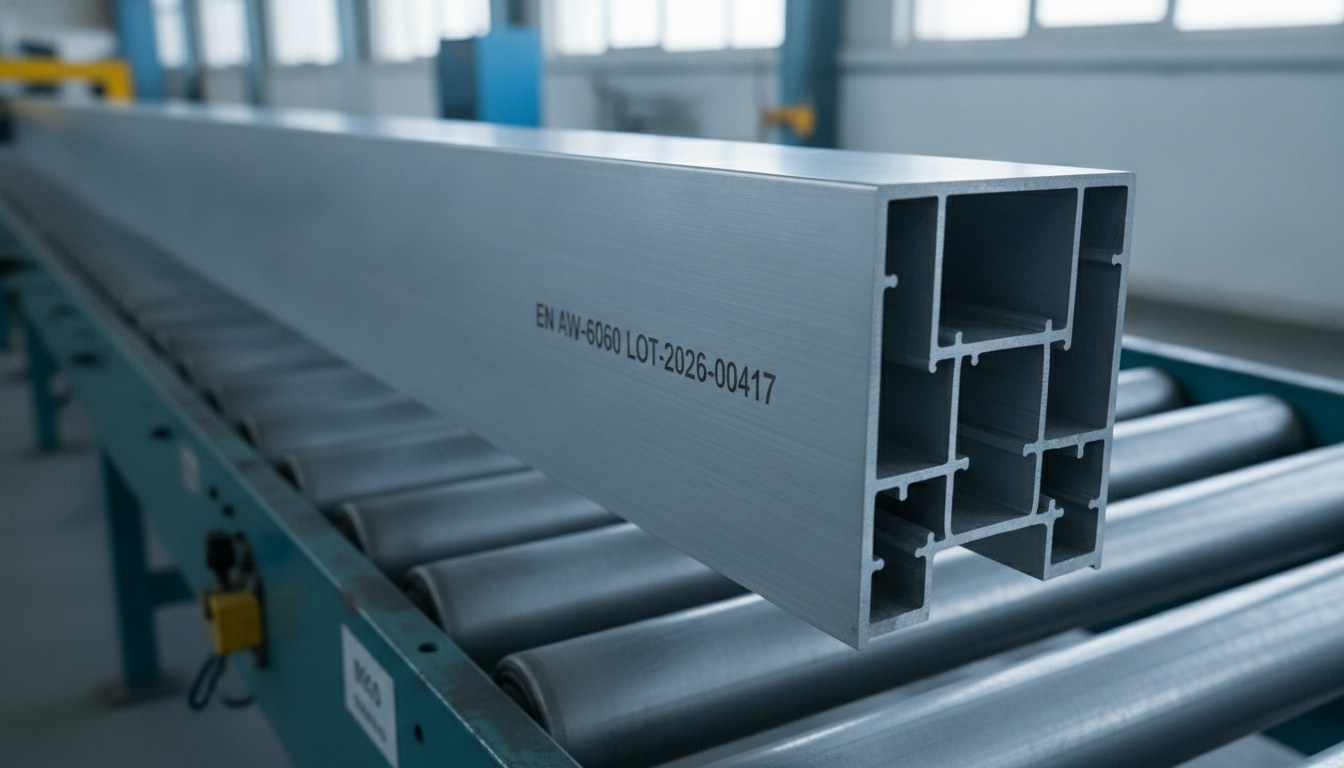
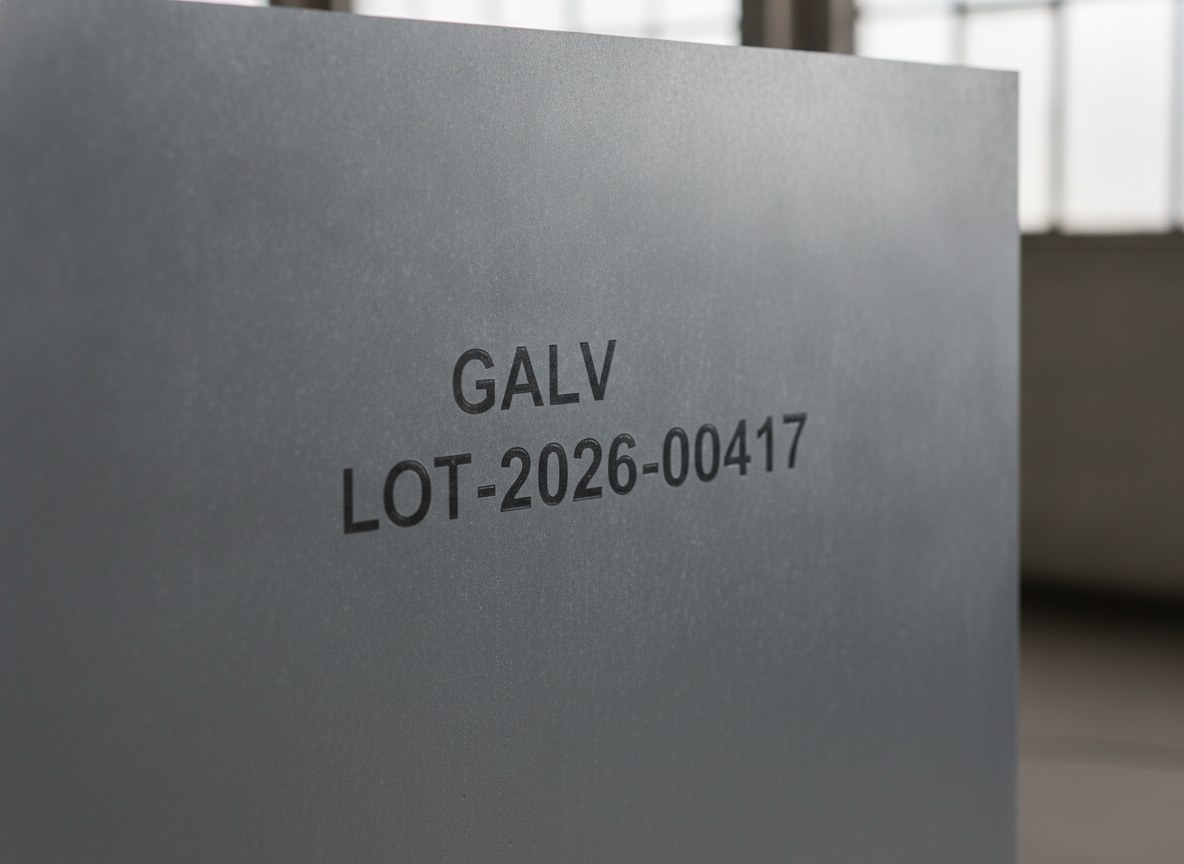
The laser deposits nothing; it modifies the metal’s surface layer. Depending on the parameters, the mark can be a dark oxide grown through annealing — a coloring of the oxide lattice without material removal — or a micro-engraving that removes a few microns of material. In either case there is no glue and no pigment, and condensation, thermal shocks and cleaning agents find no coating to attack. An annealing mark maintains stable contrast from any angle and under any light, an essential condition both for human reading of the plate data and for automatic reading of codes. Its behavior, however, changes sharply from one metal to another, and that is where it is decided whether direct marking is truly the correct choice.
Galvanized and painted sheet metal: marking without opening gateways to corrosion
On galvanized sheet the temptation is to mark by contrast, removing the zinc down to the exposed steel. In a room with condensation this is exactly what must not be done: a spot without protection is created, and rust starts right from the marking. The correct approach is to modulate the thermal input — a controlled pulse, typically with a MOPA source — to darken the layer without removing it, preserving the continuity of the corrosion protection.
The same applies to painted or powder-coated sheet metal: ablating the paint down to the metal gives immediate contrast but exposes the substrate to moisture at a localized point, whereas it is better to act on the coating without exposing the underlying metal. It is the fine control of the parameters, more than power itself, that distinguishes a durable marking from one that becomes a trigger for corrosion.
Stainless steel and plate heat exchangers: black annealing and stable contrast
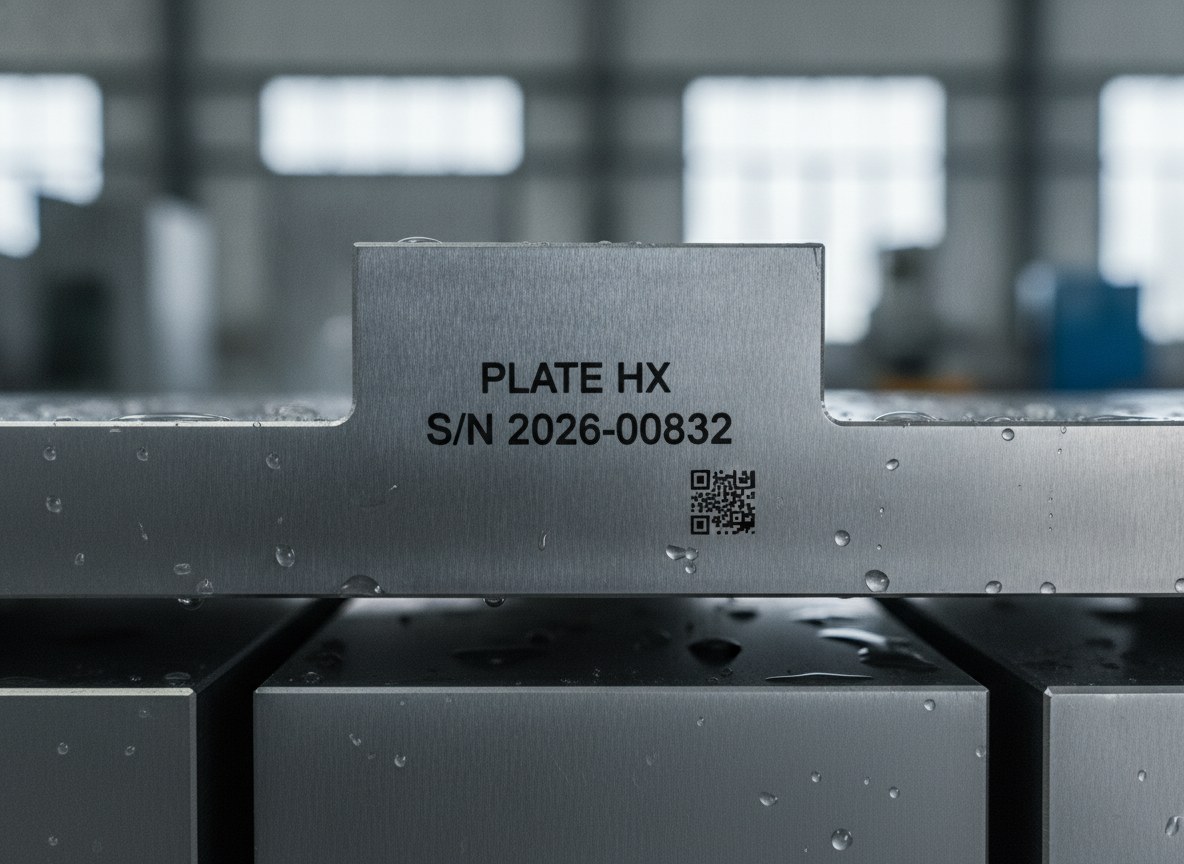
Stainless steel is the ideal material for direct laser marking in humid environments. Annealing produces a deep black mark, integrated into the surface, that survives condensation and thermal cycles without degrading. The caution lies in dosing the energy: overly aggressive annealing can locally alter the passive layer, so the parameter must be calibrated to obtain the necessary contrast while preserving corrosion resistance, as is generally considered in the surface treatment of steel with the laser. Plate heat exchangers are the emblematic case: packs of thin stainless steel sheets where the serial number and data must be engraved permanently without adding thickness or carriers. The mark remains part of the plate and accompanies it throughout its entire life, including washing phases and the temperature cycles of operation.
Copper and reflective alloys: the source makes the difference
Copper, widespread in piping, manifolds and heat exchangers, is the most difficult metal. At the fiber’s 1064 nm wavelength it is highly reflective and conducts heat away too quickly, and the mark comes out inconsistent. The correct path is to change the wavelength: the green source at 532 nm is absorbed far better by copper and delivers clean, repeatable marking even on shiny surfaces. On brass and bronze, typical of valves and fittings, fiber becomes suitable again and produces sharp, stable markings. In heating and plumbing there is no single laser that is good for everything, but rather the right source for each metal: defining it in advance, on the product’s actual materials, is what prevents weak markings that later fail in the field.
The legibility of mandatory data, measured over time
The requirement is not “to mark,” it is to remain legible years later, when the equipment has already operated for a long time in a humid environment. Alongside alphanumeric data, more and more plates carry a DataMatrix or a QR that links the serial number to the technical documentation and energy data: an unreadable code is lost data. The stable contrast of laser marking is what makes the code reliable over time and enables in-line grading — the control standard applicable during production — while formal verification of code quality remains an operation for controlled laboratory conditions. A mark that does not peel and does not fade is the prerequisite for both checks to remain meaningful.
When a plate or screen printing remains the right choice
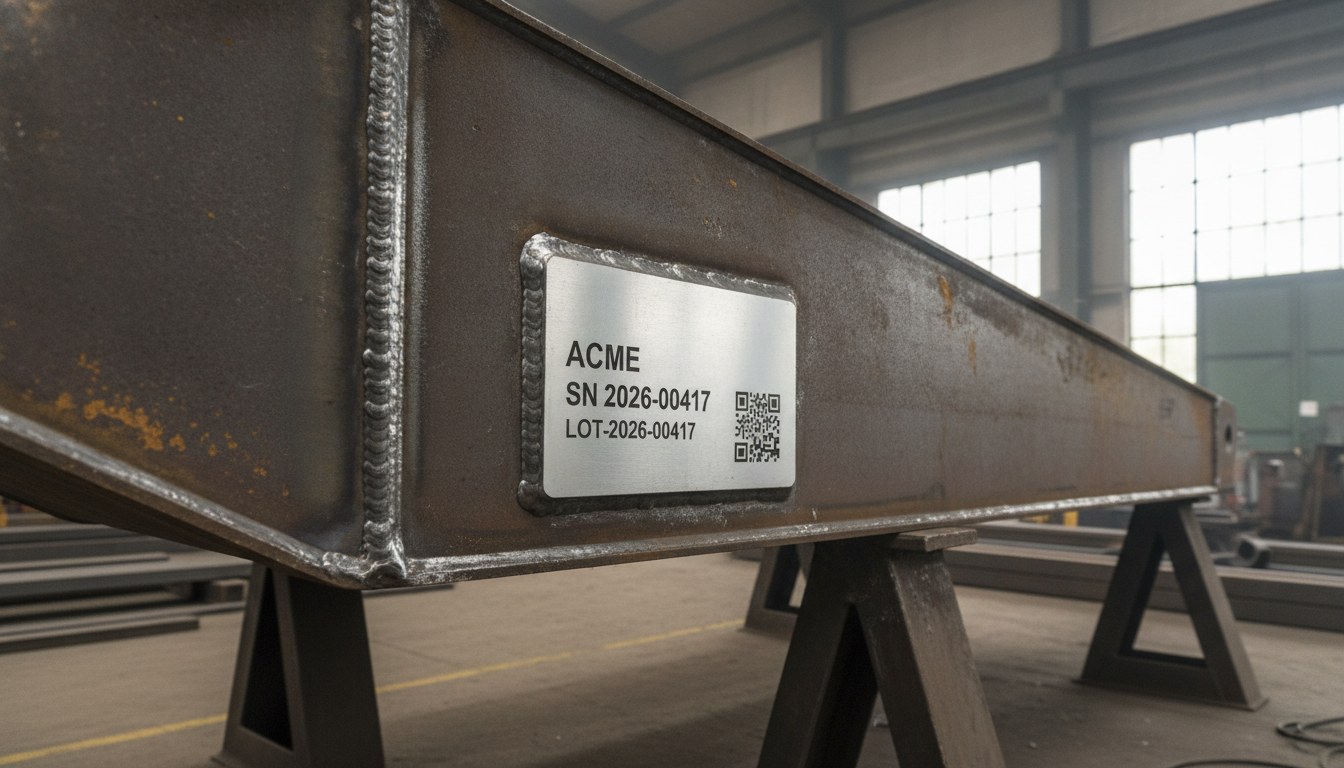
Direct marking does not cover every case. There are surfaces that one does not want to, or cannot, alter — aesthetic finishes, certain technical coatings, plastic housings — and points that the laser head can no longer reach after assembly. In these situations the robust solution is a laser-marked metal plate then fixed to the part: the permanence of the mark engraved in the metal is retained, but the marking is decoupled from the product’s surface.
Then there are the layout constraints. When there is a great deal of mandatory data, or when regulated colored logos and safety pictograms are required, the natural field is screen printing or a pre-printed plate, because marking on metal works on the contrast of the surface and does not reproduce full-color graphics. In short: where the data must last as long as the equipment, in environments with condensation and thermal cycles, direct laser marking is the most reliable; where the surface is not markable or the layout requires color and graphics, laser-marked plates and screen printing remain complementary, not competing.

Public Relations Manager | LASIT
Public Relations Manager at LASIT since 2019, Claudia Neri is responsible for managing the Marketing and Communications department. She handles the company’s communication strategy, coordinating public relations, brand promotion and institutional communication activities for the Italian and international market.