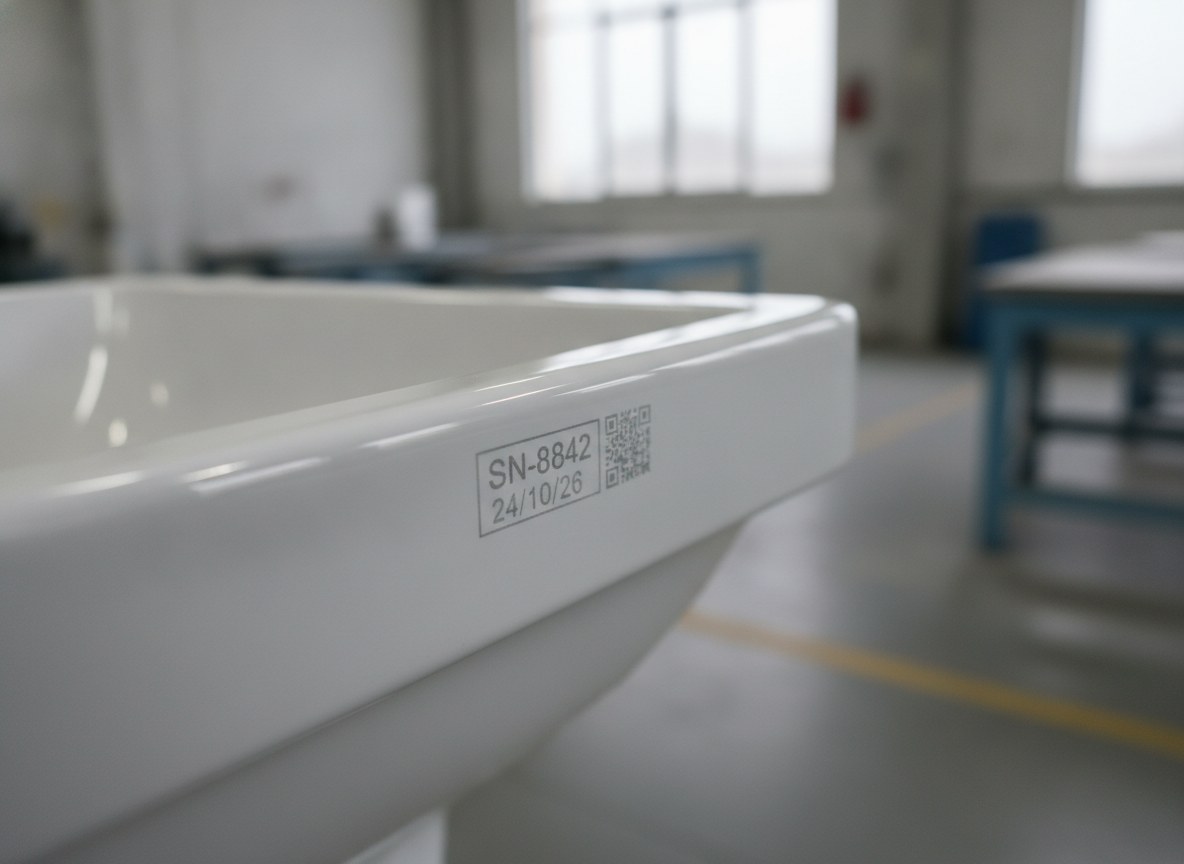
Manufacturers of sanitaryware, glazed ceramic items or components coated with vitreous enamel know the problem well: brand, batch reference and date must go onto a visible part, and enamel is one of the toughest layers to work on. It is hard, glossy and glass-like, but also brittle: under localized thermal stress it tends to behave like glass, not like a metal.
This gives rise to two typical risks. The first is mechanical: a marking that is too aggressive, or done with the wrong wavelength, opens microfractures in the enamel and can lead to chipping that compromises a part meant to stay on view for years. The second is aesthetic: on white enamel, contrast is the real challenge, because a poorly controlled marking comes out weak, inconsistent from part to part or almost invisible depending on the light.
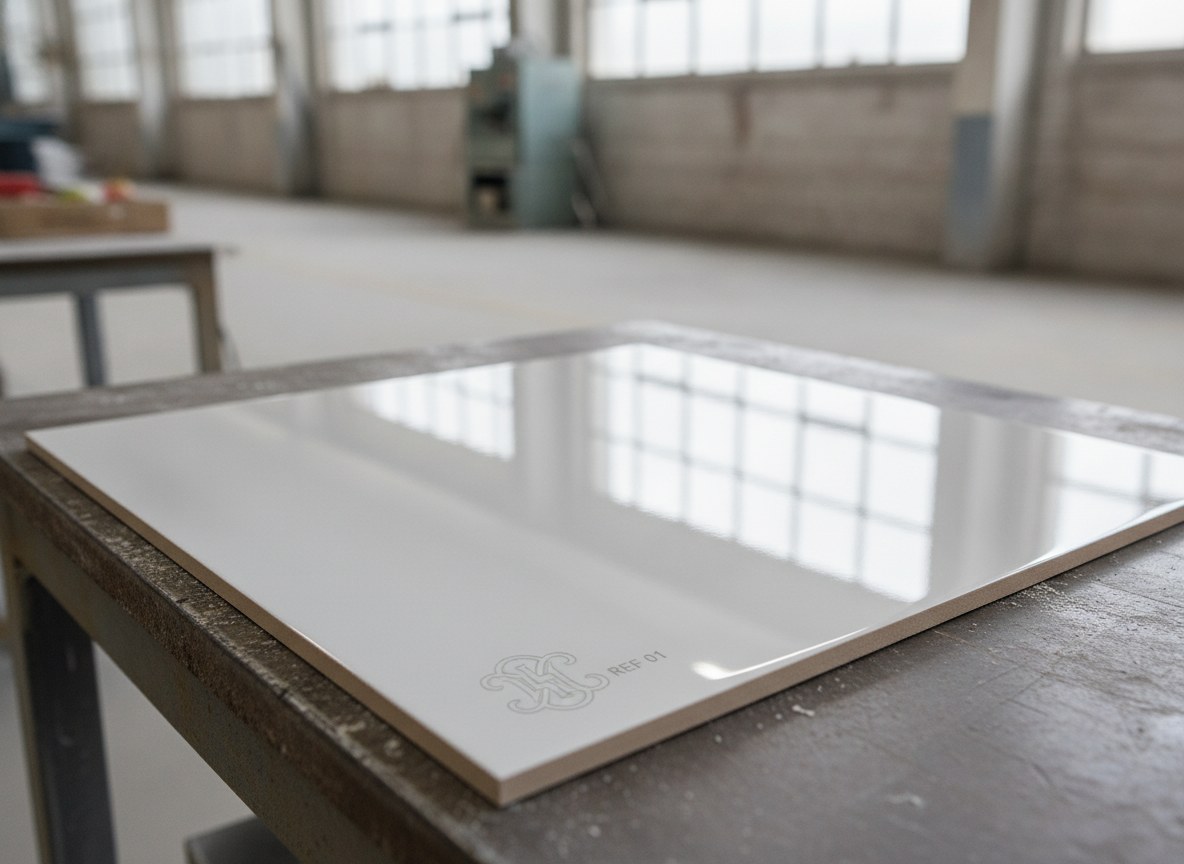
UV laser marking tackles exactly this issue: not raising the power to “beat” the hardness of the enamel, but controlling how the energy is absorbed by the glass to obtain a legible and repeatable mark without cracking the surface.
How vitreous enamel reacts to the laser
Ceramic enamel is, to all intents and purposes, a vitreous layer: a silicate matrix vitrified during firing, with opacifiers and pigments dispersed within it. Like glass, it has low thermal conductivity and brittle behavior. When it absorbs energy in a concentrated and mainly thermal way, local expansion generates stresses that the material cannot relax plastically: the result is microcracks that start from the marked point and, at the edges, can develop into chipping.
The decisive factor is how much and how the enamel absorbs the radiation, and this depends on the wavelength. A fiber source works at 1064 nm, in the near infrared: on clear glass or white enamel that radiation is poorly absorbed and tends to heat rather than cleanly modify the surface, with a reduced margin of control right where the material is most fragile. Moving toward the ultraviolet, the picture changes radically.
Why ultraviolet controls the interaction with glass
The UV source emits at 355 nm. The short wavelength corresponds to a higher photon energy, and this is why UV interacts well with materials that infrared “passes through” or merely heats: glass, transparent plastics and vitreous enamels. The energy is absorbed in a very thin surface layer, where it is needed, instead of spreading as heat through the volume of the part. It is the same principle that makes UV the go-to choice on delicate materials — it is worth recalling what a UV laser is for the full physical picture.
The practical consequence is a limited heat input and a “colder” interaction with the enamel: the surface is modified without generating the thermal gradient that cracks the glass. This does not mean zero thermal impact — there is always some residual — but a level low and controllable enough to prevent the propagation of microcracks. On vitreous enamel this is the difference between a stable mark and a part at risk of scrap. The same reasons explain why UV has become established in glass marking.
Pre- and post-firing marking
In ceramic production there are two routes. The first is pre-firing decoration: the graphics are applied to the bisque or to the raw glaze and then vitrified during firing, remaining embedded beneath the surface. It is the traditional method for logos and decorations, extremely robust because the mark becomes part of the enamel itself.
The second is post-firing laser marking, on the already finished part. Here the UV laser acts on the vitrified enamel, modifying its surface layer in a controlled way. The advantage is flexibility: brand, batch, date or a variable identifier can be applied without touching the decoration stage, and the content can be changed part by part without producing new decorations or screen prints. It is the natural route when the information to be marked changes often or arrives downstream of the ceramic process.
| Aspect | Pre-firing decoration | Post-firing UV laser marking |
|---|---|---|
| Moment in the cycle | Before firing, on the raw glaze | On the finished, already fired part |
| Bond with the part | Vitrified within the enamel | Controlled surface modification of the enamel |
| Variable data (batch, date, serial) | Impractical: requires new decorations | Immediate, managed by software |
| Extensive multicolor decoration | The natural domain of decoration | Not its function |
Contrast on white enamel
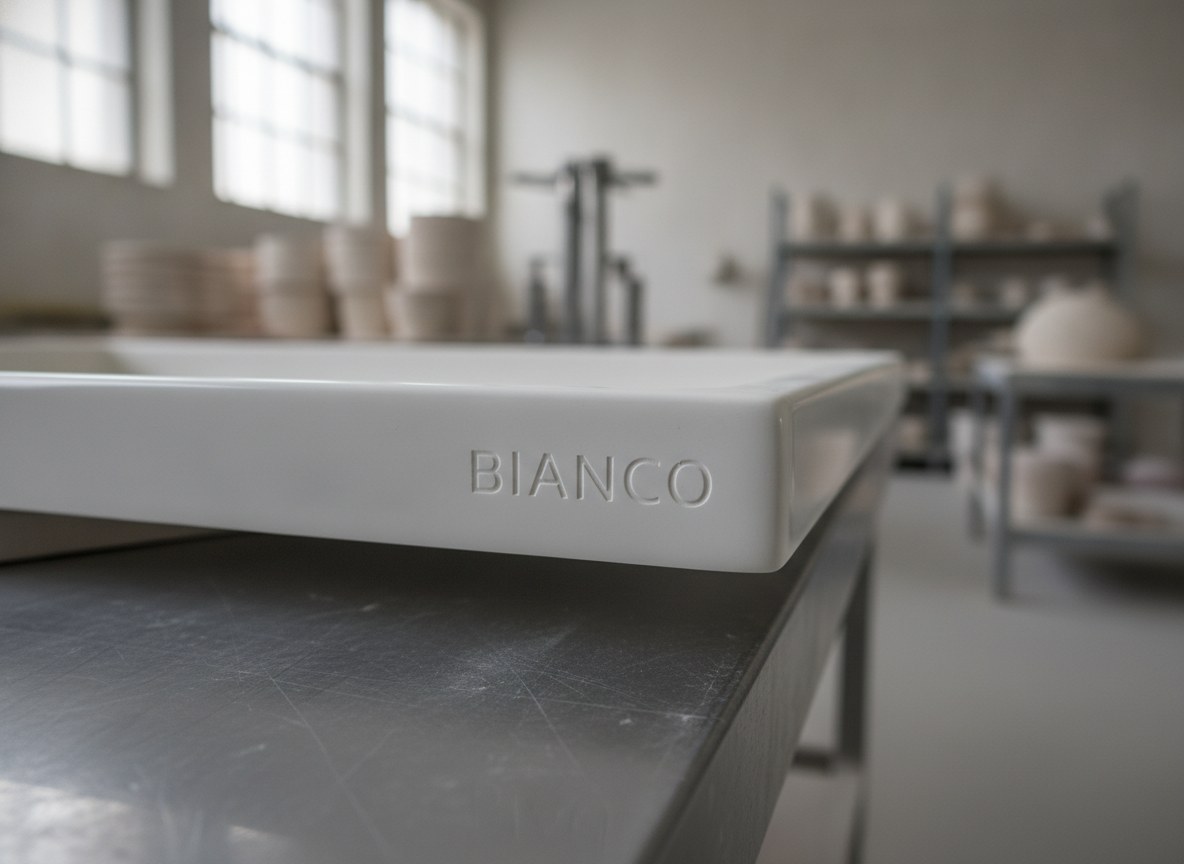
On white, contrast is not achieved by adding a color: there is no pigment here and no oxidation to exploit as on metals. Instead, UV works on the finish, controlledly transforming a portion of glossy enamel into a matte micro-texture. The mark becomes legible because it scatters light differently from the specular surface around it: it appears as a satin-finish engraving, crisp, with a slight tonal shift. It is a contrast of finish and micro-relief, not of color, and it is exactly what a brand or a batch code needs to be legible at a glance.
The critical point is that this micro-texture stays constant: parameters pushed too far slide toward cracking, parameters that are too mild give a pale mark that disappears under certain lights. The correct working window is identified on real samples, and it is what holds together legibility and enamel integrity.
Aesthetic repeatability on visible parts
On a visible part, repeatability is no small detail: the brand must look the same on the first and the last part of the batch, and from batch to batch. Once the marking recipe is set — energy, speed, fill strategy — the FlyCAD software recalls it identically at every cycle, removing the operator variability that afflicts manual methods. The same attention to aesthetics on delicate surfaces guides the articles on laser marking on ceramic in the promotional field.
Geometry and focus matter too: many glazed ceramic parts have curved surfaces or raised edges, where keeping the beam in the correct working plane is what ensures a uniform mark across the whole area. It is a job of process control, before power.
Who it is designed for (and who it is not)
UV laser marking is the rational choice when you need to mark brand, batch, date or identifiers on already fired glazed ceramic and sanitaryware, with a permanent mark, legible on white and with no risk of chipping — especially if the content changes often and marking takes place at the end of the line. It withstands cleaning agents and the typical use of these products, and it avoids burdening the decoration stage.
It is not, however, the right route when the goal is an extensive multicolor decoration or large-format graphics: that is the territory of pre-firing decoration, which vitrifies the color into the enamel and remains the best solution for the decorative appearance of the part. Likewise, on very dark enamels or on geometries that make an at-a-glance reading difficult, it is advisable to assess the specific case with sample tests before defining the process.

Applications Manager | LASIT
Applications Manager at LASIT for over 20 years, Mario Palmieri oversees the management and development of the company’s laser laboratory. He is responsible for conducting sample tests for customers, supporting the automotive, medical, aerospace and electronics sectors in identifying the most suitable laser marking solution for their needs.