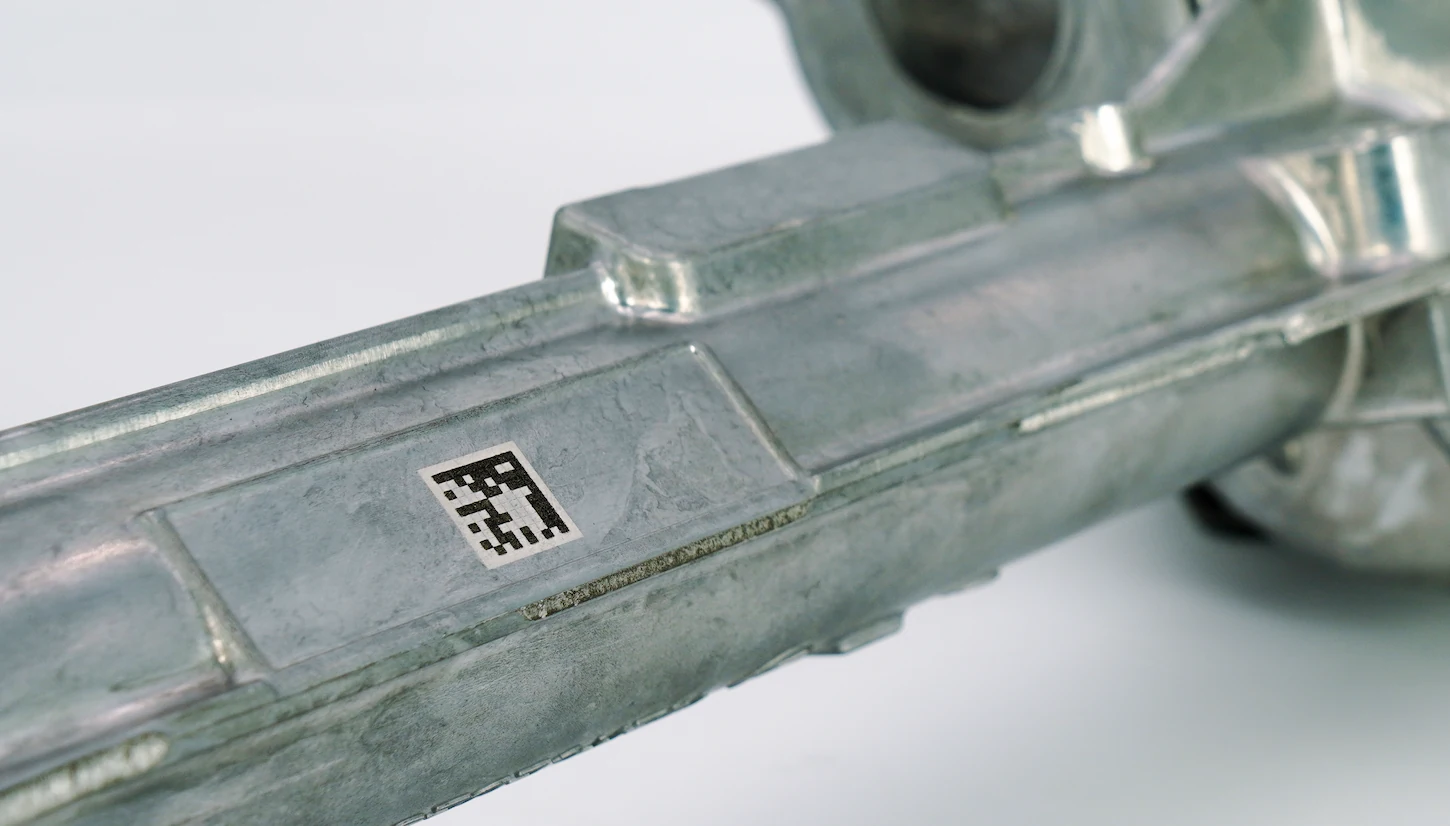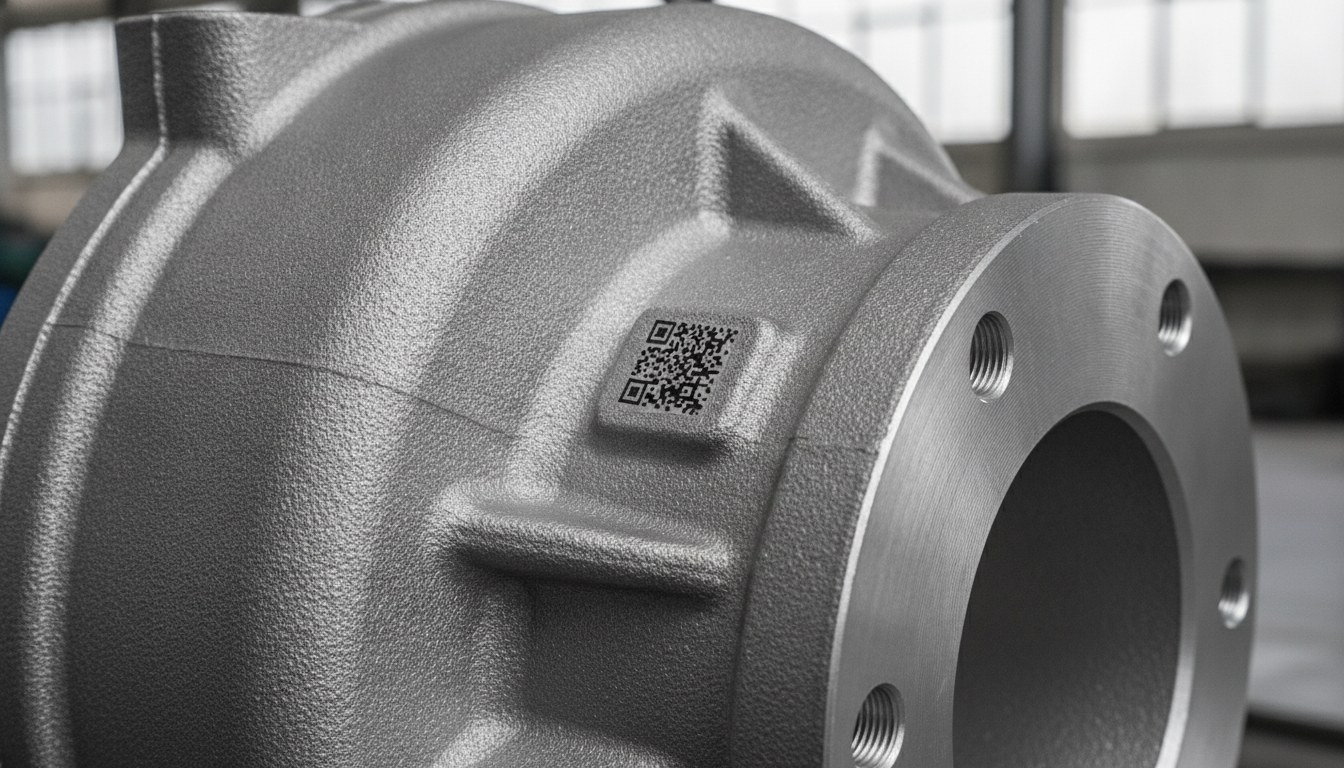
Anyone who produces die-cast components in zamak or aluminum alloy knows a recurring scene at the end of the line: the same marking recipe that left a crisp DataMatrix and a satisfied scanner on the part just marked returns, on the next part, a washed-out, blotchy code with entire areas that vanish against the background. No one touched the parameters, yet the contrast has changed.
The instinctive reaction — raising the power, slowing the scan, dwelling on the same spot — almost never solves the problem, and often makes it worse. The reason is that the variability doesn’t originate in the machine: it originates in the part. The surface of a raw casting isn’t as uniform as that of a rolled or turned piece, and the laser marks exactly what it finds under the beam, defects included.
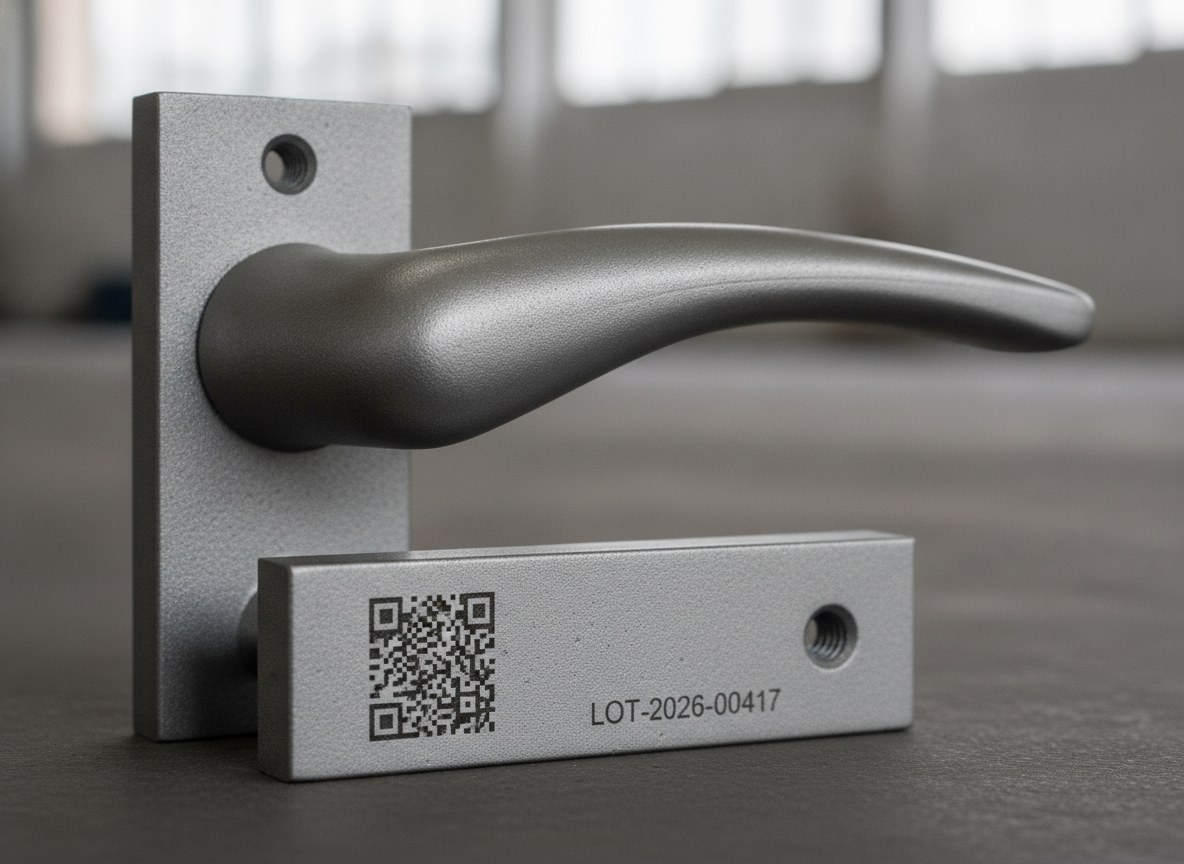
Insufficient and uneven contrast on die-cast parts is, first and foremost, a metallurgical and surface defect, not a calibration error. Addressing it means changing the marking strategy and, when needed, moving the point where you mark — not chasing a perfect parameter that doesn’t exist on that raw casting.
The skin effect: why a raw casting isn’t a homogeneous surface
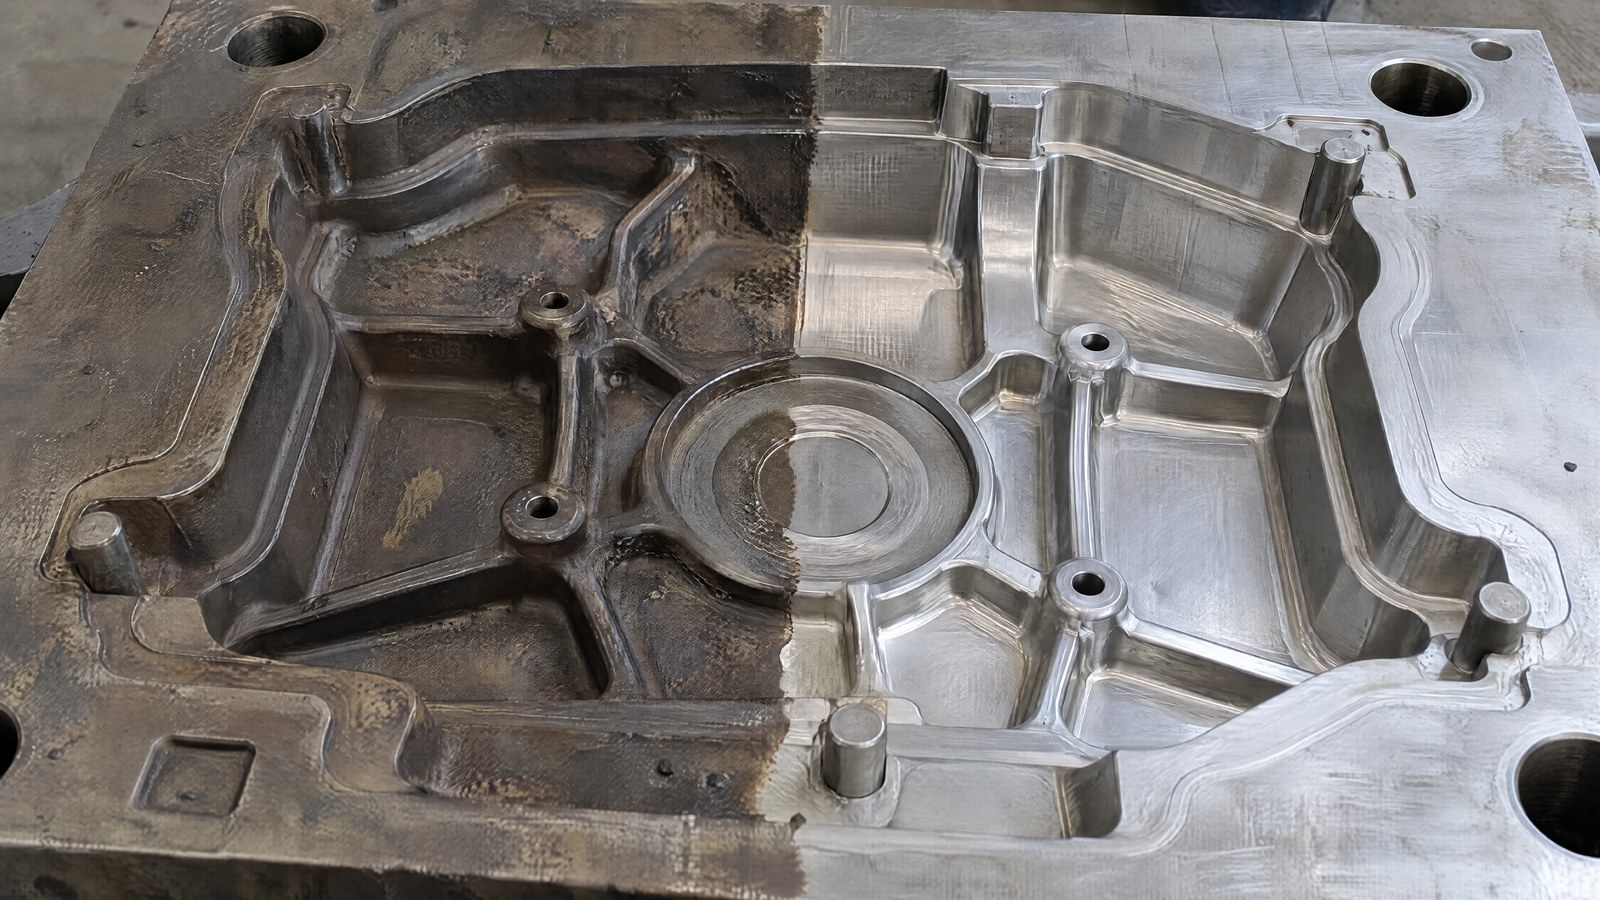
Every part that comes out of the mold carries a casting skin: a thin surface layer, yet decisive for marking, formed during solidification in contact with the wall of the die or mold. This layer is chemically different from the core of the part — richer in oxides, release-agent residues and trapped microporosity — and its thickness and compactness vary from zone to zone and from pour to pour.
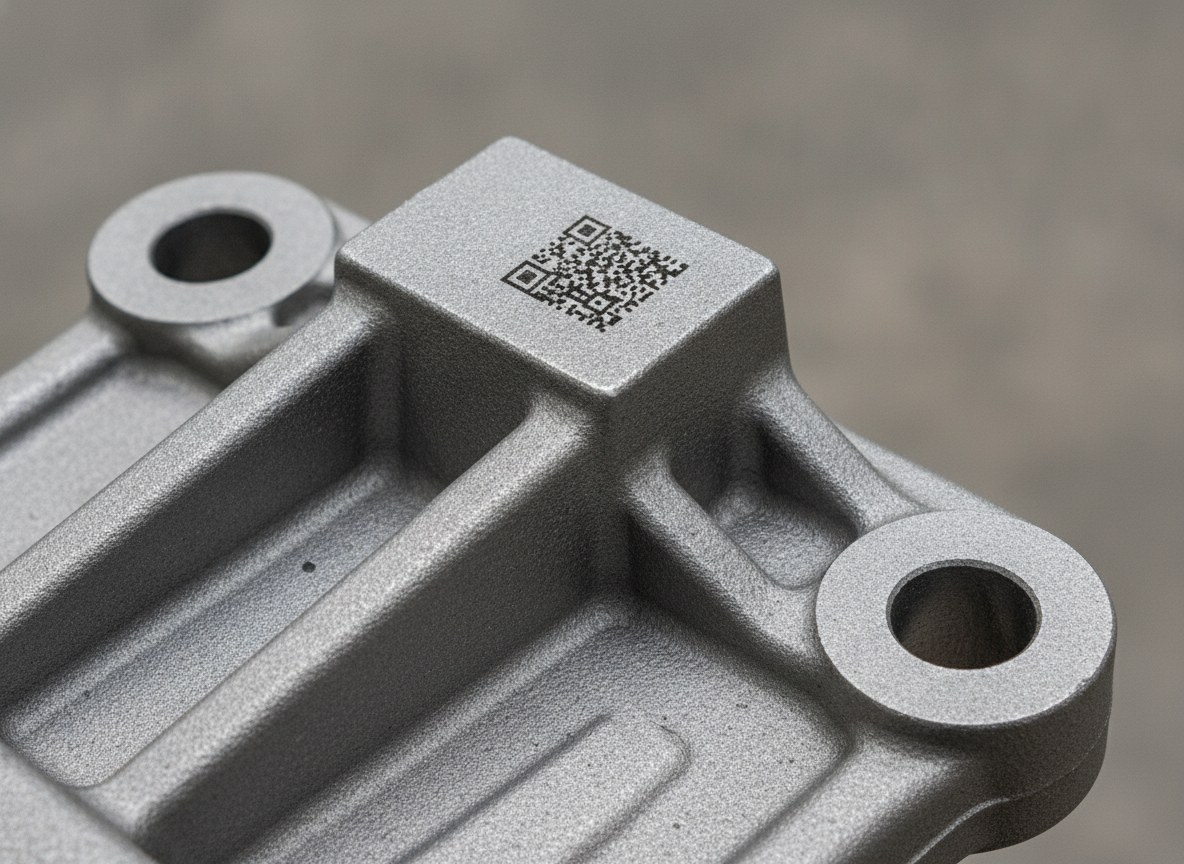
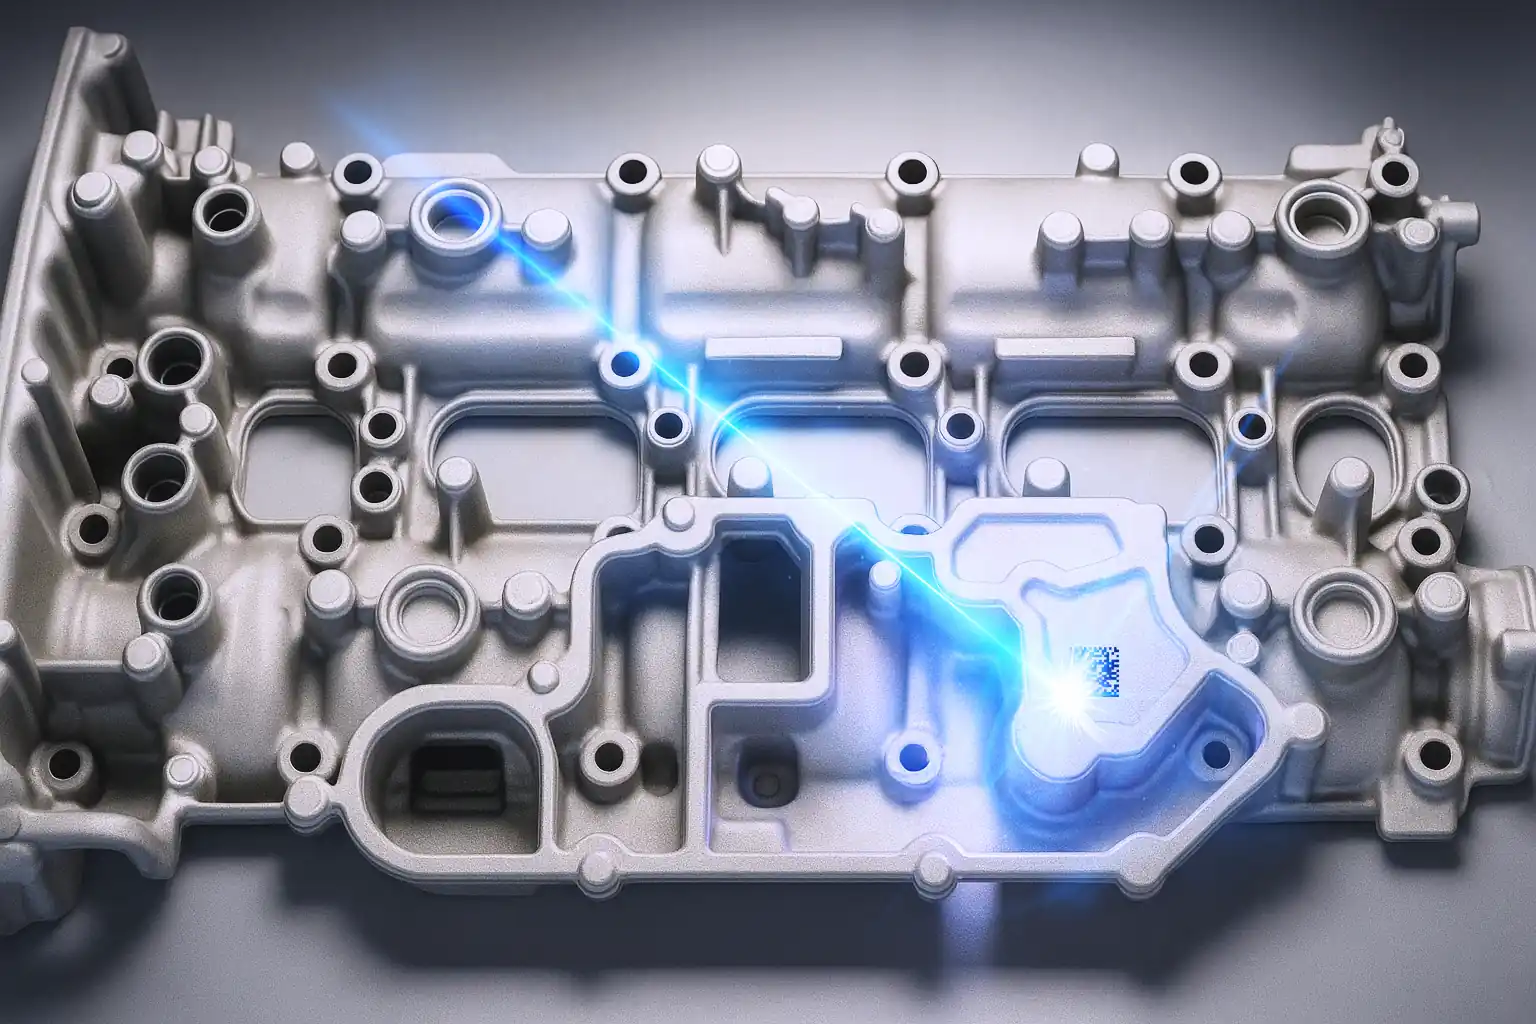
The laser interacts with the first few microns of the material. When marking occurs through oxidation or annealing, the contrast is the result of a controlled reaction on that outer layer: if the layer changes — because there’s sub-surface porosity under the beam, a lifting of the skin, an alloy segregation — the color that comes out changes too. It’s the same principle by which a flawless mark on a polished sample behaves unpredictably on a raw casting fresh from the die.
It isn’t, then, a problem of machine repeatability, which on a single point stays constant, but of surface repeatability. It’s a distinction that completely changes the approach: you don’t chase the calibration, you design the mark taking into account how the part is made. The same reasoning that guides laser engraving in the foundry industry applies, with different constraints, to contrast as well.
Why raising the power doesn’t solve it (and often makes it worse)
The most common temptation is to raise the power to “force” contrast on the difficult parts. On a raw casting this produces the opposite effect. Beyond a certain threshold the beam doesn’t blacken more: it punches through the casting skin, opens up the porosity beneath the surface, and generates craters, burrs and specular reflections that disturb the very optical reading you were trying to improve.
Laser power Mark contrast Below the surface, porosity opensThe contrast between mark and background depends on the quality of the surface reaction, not on the depth of material removal. A deeper groove on a porous alloy creates shadows and jagged edges that a scanner reads as noise, not as data. Adding energy means adding heat, and on zamak and die-cast aluminum more heat means more local melting, more halos and more visual variability — the exact opposite of the uniformity you need. The right lever isn’t depth: it’s how the energy is distributed across the surface.
Increase the area, not the depth: fills and hatch
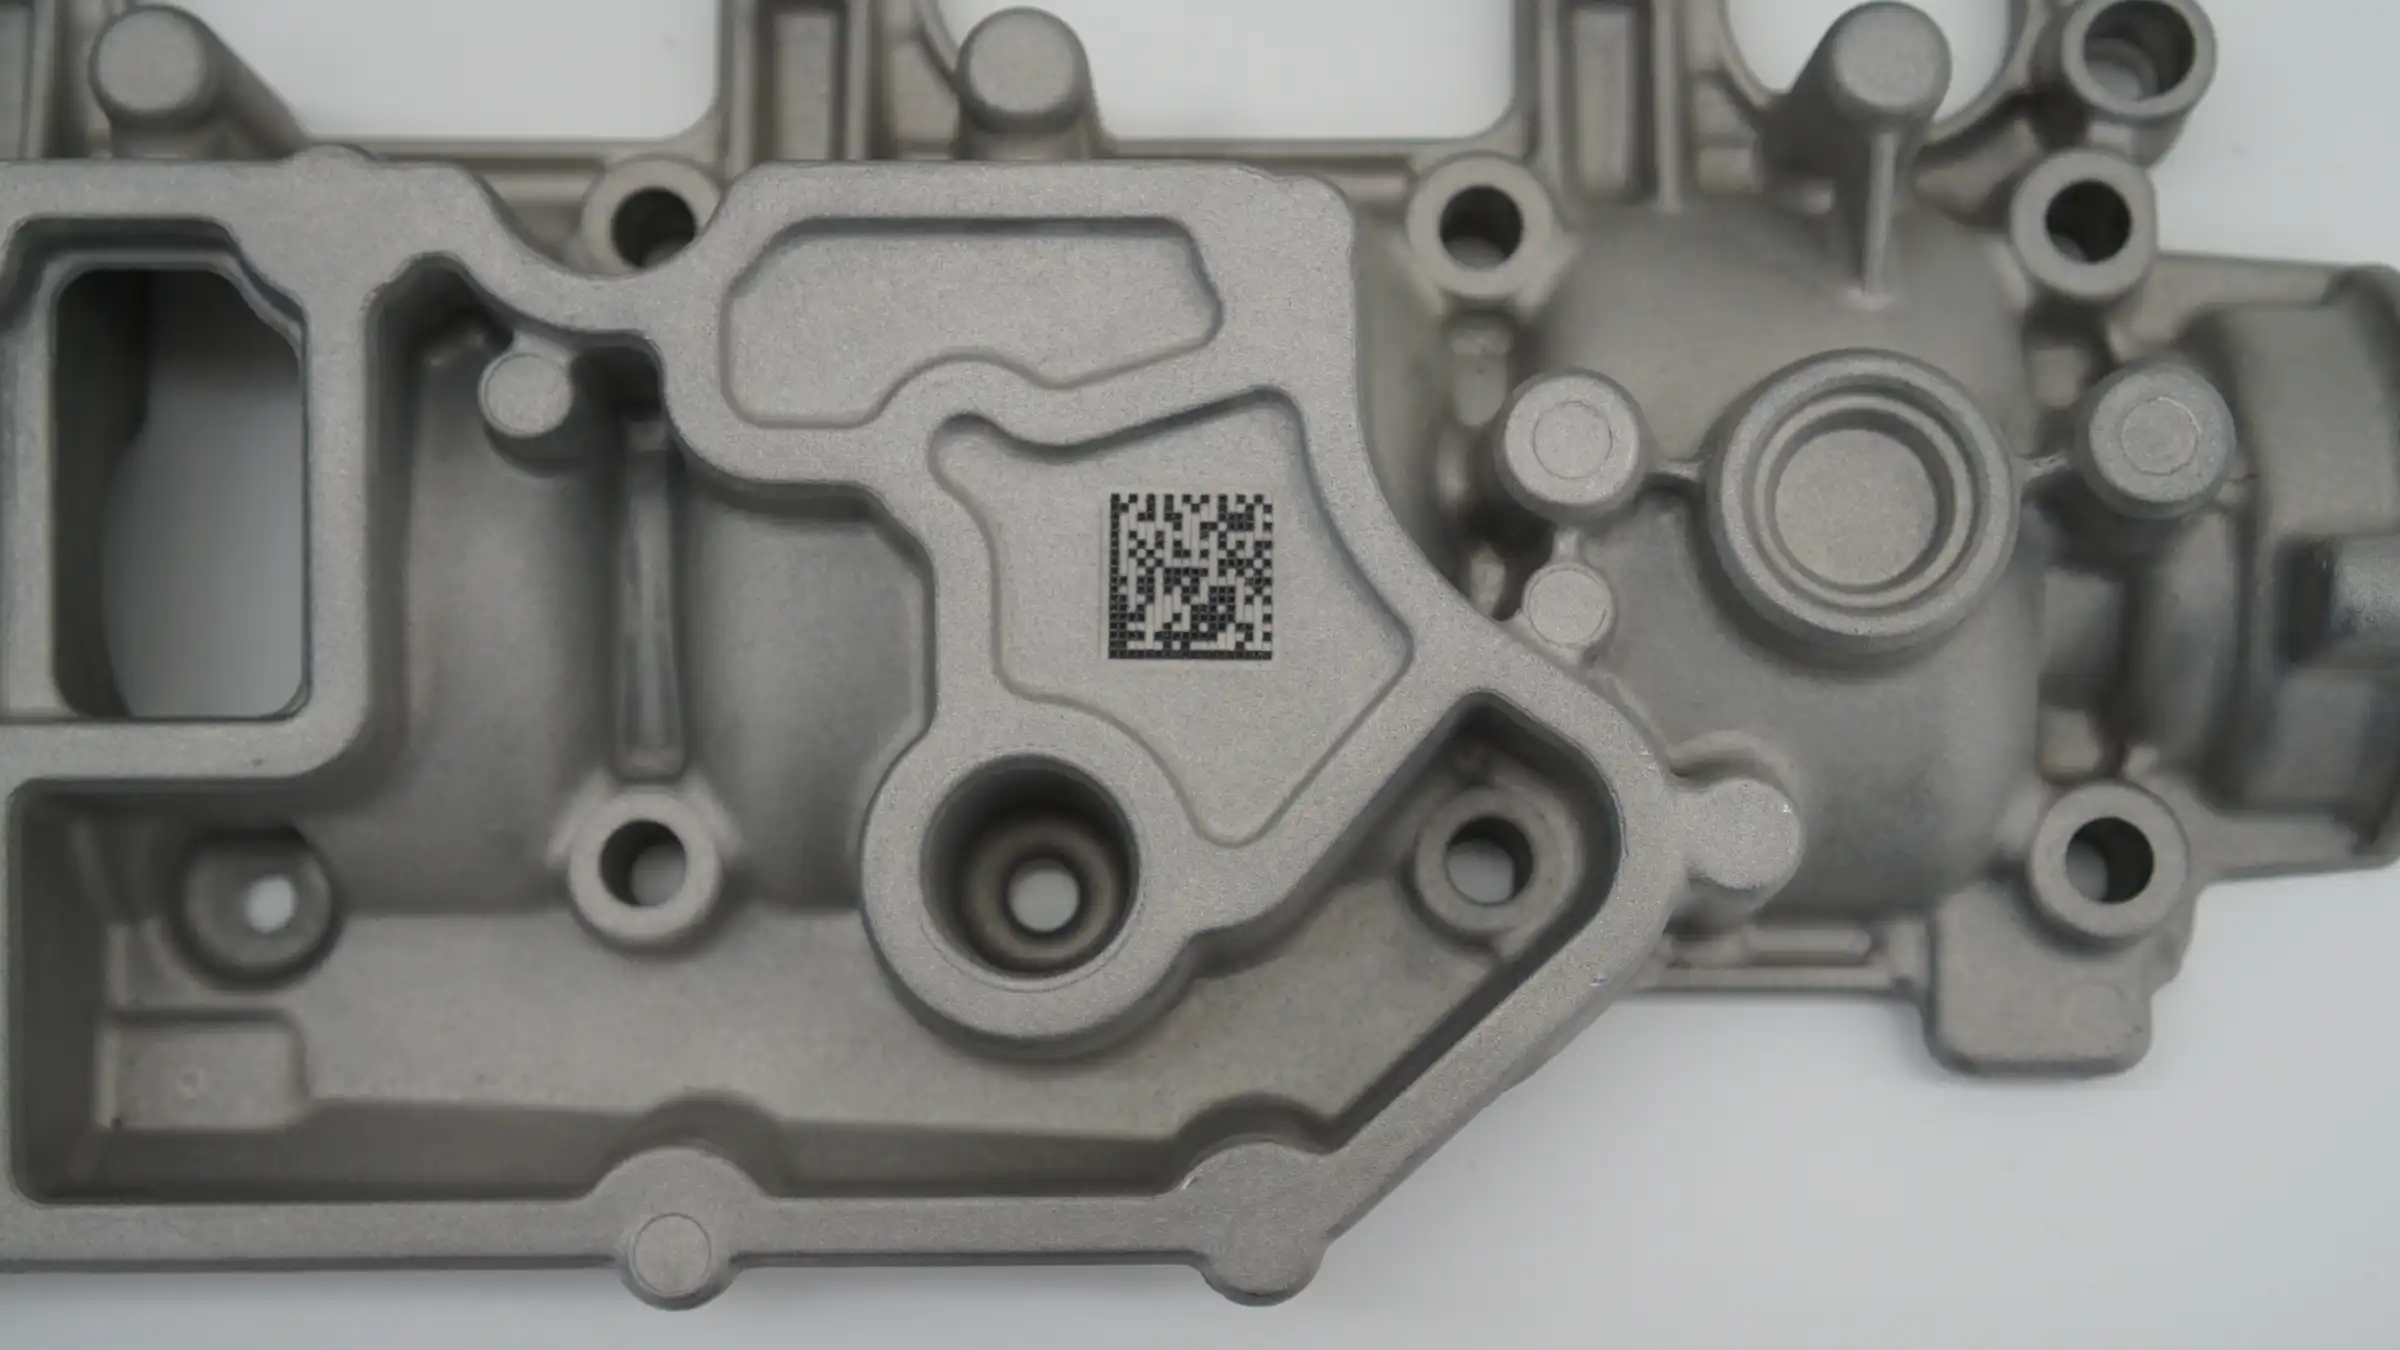
The strategy that delivers the most stable results on the raw casting goes in the opposite direction from deep engraving: widen the footprint and work at low energy over a broader area. Marks with a dense hatch, fills made of multiple light passes and a slightly widened focus average out the local inconsistencies: where one point falls on a pore, the one next to it falls on sound material, and to the eye as to the scanner the code module still comes out full and uniform.
It’s a contrast achieved through extension and averaging, not through cutting. DataMatrix characters and modules should be sized generously enough to absorb the graininess of the raw casting, avoiding thin strokes that a single pore can interrupt. The same logic of controlling energy input that applies to laser marking on aluminum becomes the guiding criterion here, because die-cast alloy is less predictable than its wrought version.
In this scenario the source matters. A MOPA source, being able to vary the pulse duration, allows you to tune the surface reaction to obtain controlled grays and blacks without driving the area into melting — a valuable margin of adjustment on surfaces that change from one part to the next. On why the adjustable pulse makes the difference, I refer you to the comparison between MOPA laser and fiber laser.
Marking on an already machined area: the most reliable strategy
When legibility is a requirement and not a nice-to-have — a traceability DataMatrix that has to be graded in line — the most solid solution isn’t to optimize the mark on the raw casting, but to take the raw casting out of the equation. Planning a small faced or milled pad at the marking point during mold design eliminates the casting skin and exposes homogeneous material: the surface becomes repeatable, and so does the contrast.
Design for reliable markingCastingMachined padLaser markingIn-line gradingIt’s a principle of design for marking: markability is decided upstream, when you draw the cavity, not downstream when the part is already cast. A pad of a few square inches, already provided for in the drawing, costs far less in terms of scrap and rework than a mark that passes grading one lot and fails the next. Where the cycle already includes a machining operation, marking on a machined face is almost always the right choice.
Zamak and die-cast aluminum: two behaviors to treat separately
Treating “die-cast parts” as a single category is a mistake. Zamak, a low-melting-point zinc alloy, tends to reflow and form halos easily: it calls for narrow, tightly controlled energy windows, because the margin between a clean mark and a melted surface is small. Die-cast aluminum, with its silicon content and the gas porosity typical of the process, instead presents a surface that is more heterogeneous point by point, where the risk is local inconsistency rather than widespread melting.
It follows that the recipe must be built by alloy and, ideally, validated on the real parts of that specific production — not carried over from one material to another. Part temperature matters too: marking components while they’re still hot introduces yet another variable on contrast, an aspect we addressed when discussing marking on hot foundry parts.
Cast-lot traceability: what really needs to be readable
On die-cast parts the mark almost always serves to carry the pour’s identity downstream: lot number, mold, cavity, date. These are the data that, when facing a defect, let you quickly isolate the production involved instead of stopping everything. For this to work, the code must not only be marked: it must pass an objective check.
This is where grading comes in, the evaluation of code quality according to recognized standards (ISO/IEC 15415 and AIM DPM for direct marking), applicable in line to set a repeatable acceptance threshold. It’s worth remembering that in-line grading and laboratory verification are two distinct things: verification requires controlled conditions and dedicated instrumentation, while grading is the standard you bring into production. On this difference we dedicated an in-depth look at the difference between reading, grading and verifying codes. On a variable raw casting, in-line grading is what turns “it looks readable” into a measurable criterion.
When the raw casting isn’t reliably markable (and it pays to move the point)
There’s an honest limit to acknowledge: some raw castings aren’t reliably markable, period. If the casting skin is too irregular, the surface porosity marked, and no machined area is planned, no parameter will guarantee a repeatable contrast at grading. In these cases the right technical choice isn’t to insist, but to move the moment of marking.
Often it pays to mark downstream of an operation that returns a stable surface: after shot peening or sandblasting, after machining, or after painting or coating, where a contrast obtained by selectively removing the film becomes markedly more predictable. Alternatively, when even this isn’t feasible, traceability is assigned to a dedicated nameplate. It isn’t a surrender: it’s placing the mark where the process makes it repeatable.
In short, on the contrast of die-cast parts the right question isn’t “how much power do I need,” but “which surface am I marking on, and can I make it more uniform.” Recognizing that the origin of the problem is metallurgical — and acting accordingly on the marking area, the zone to hit and the point in the cycle — is what takes you from a code that sometimes reads to a code that always reads.

Applications Manager | LASIT
Applications Manager at LASIT for over 20 years, Mario Palmieri oversees the management and development of the company’s laser laboratory. He is responsible for conducting sample tests for customers, supporting the automotive, medical, aerospace and electronics sectors in identifying the most suitable laser marking solution for their needs.